

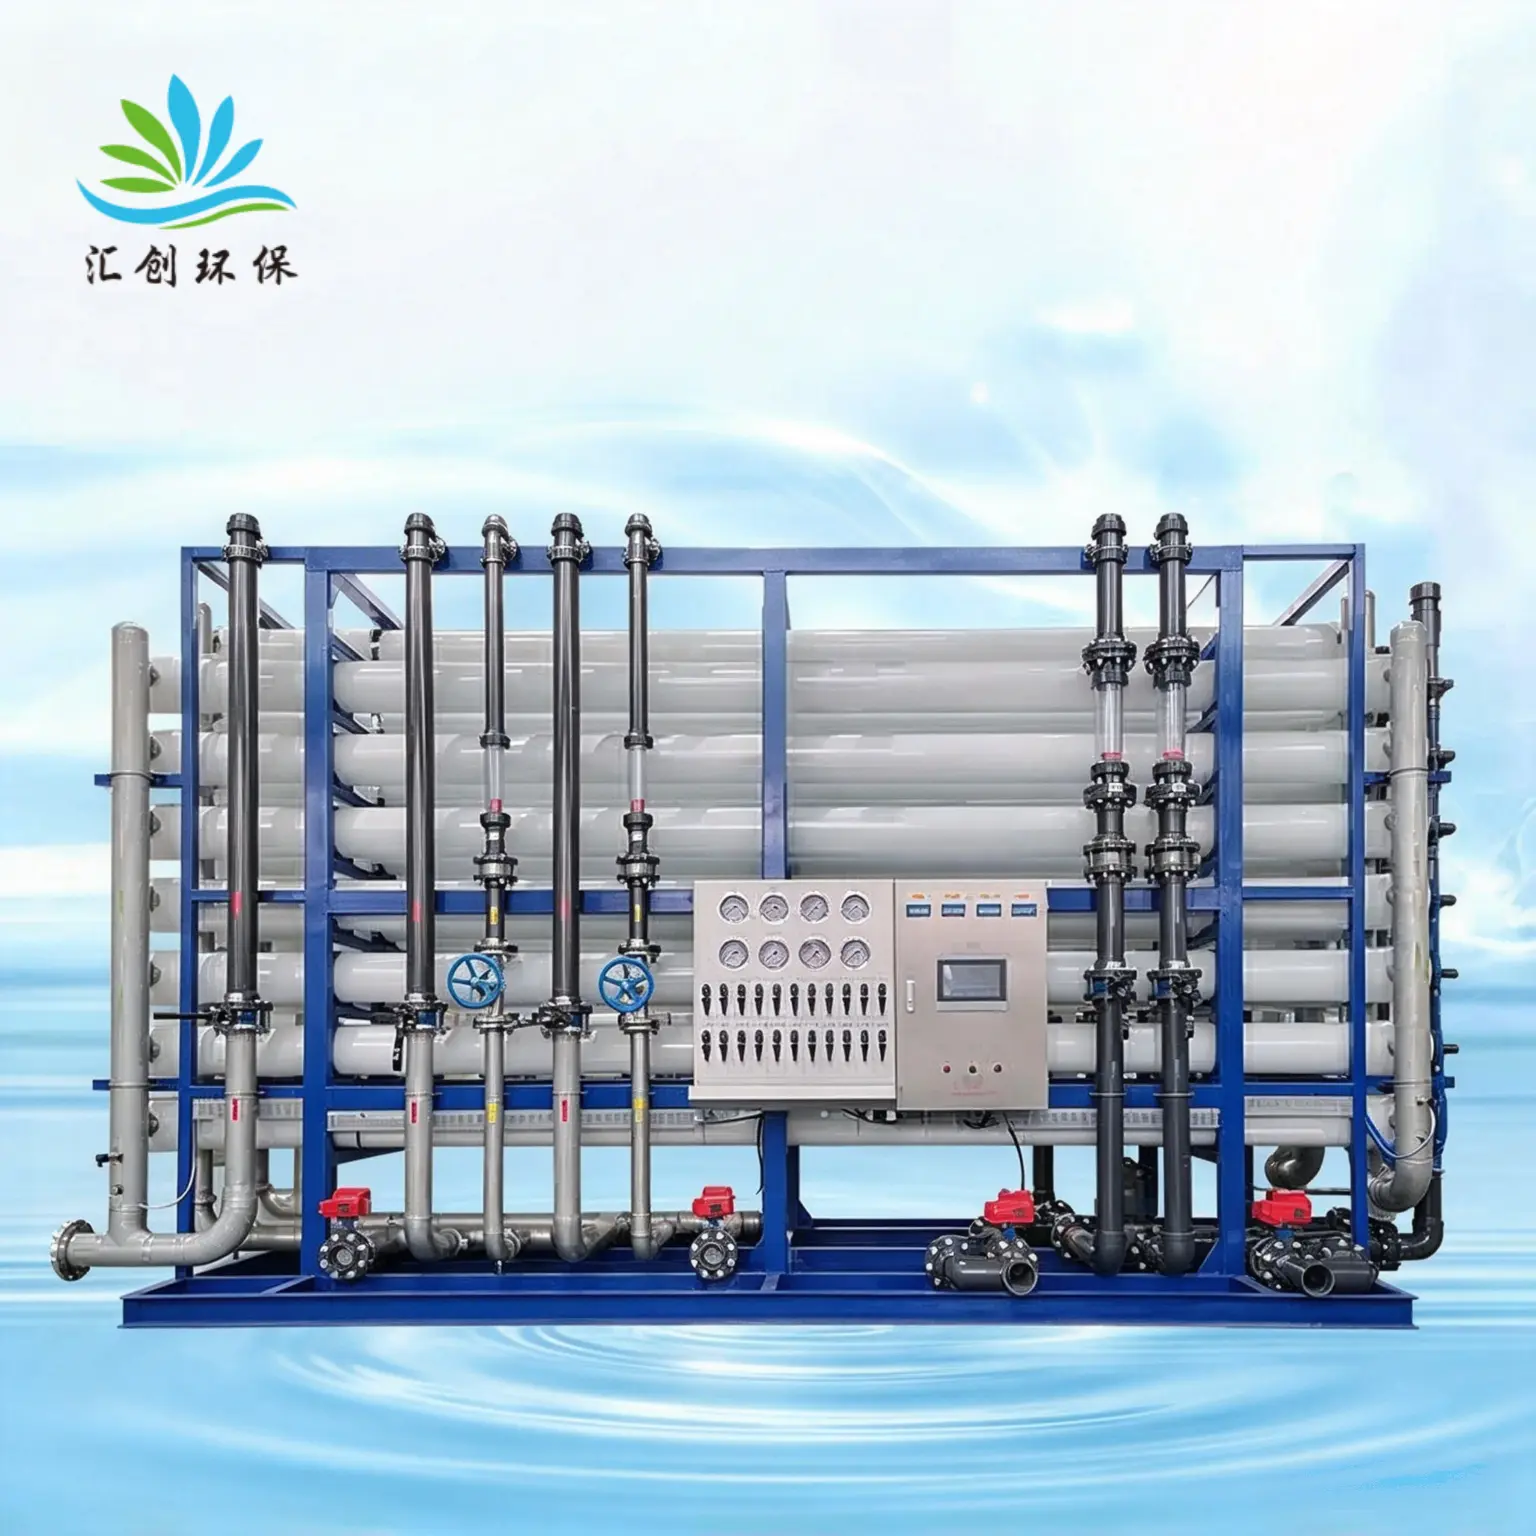
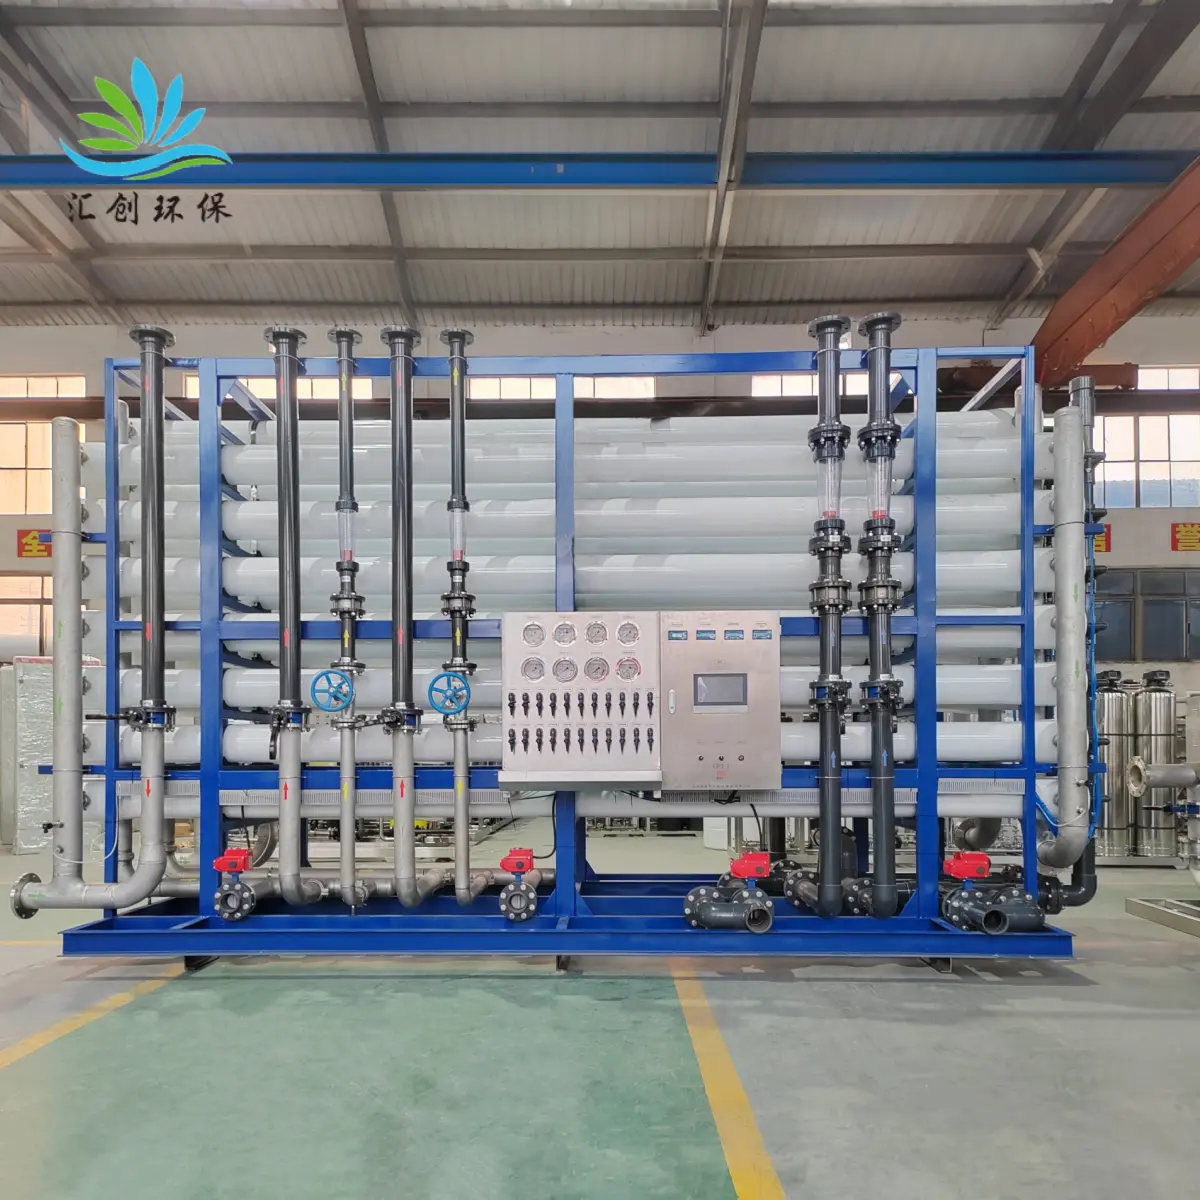
50 T/H Large-Scale Commercial & Industrial Reverse Osmosis (RO) Plant
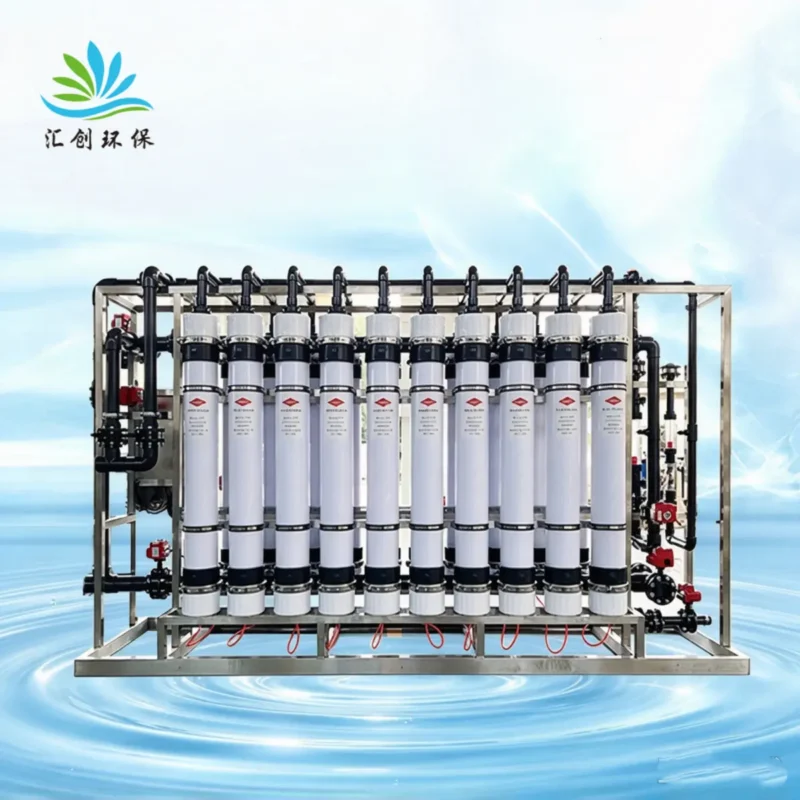
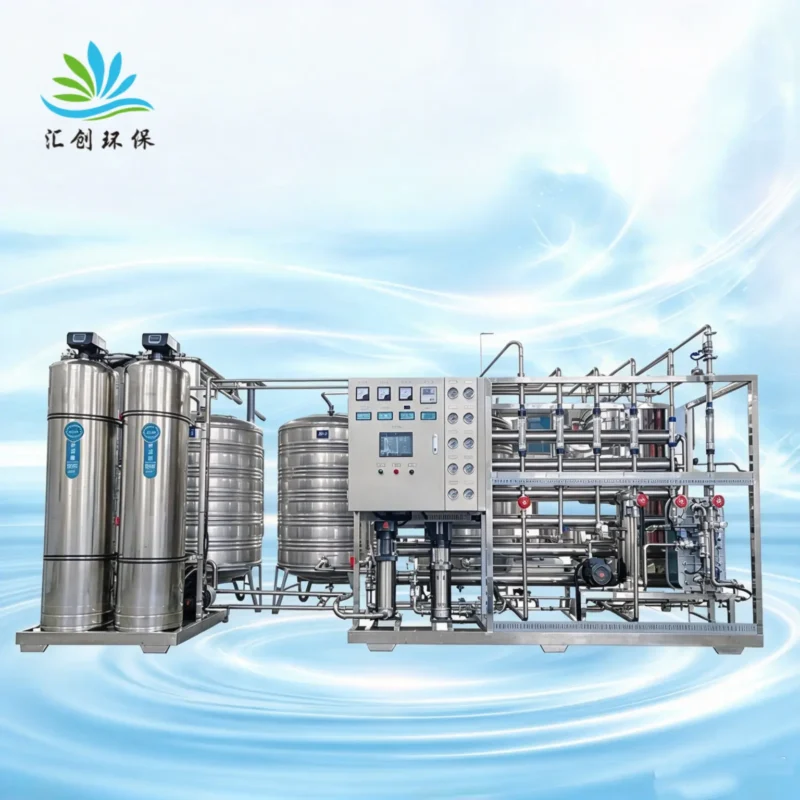
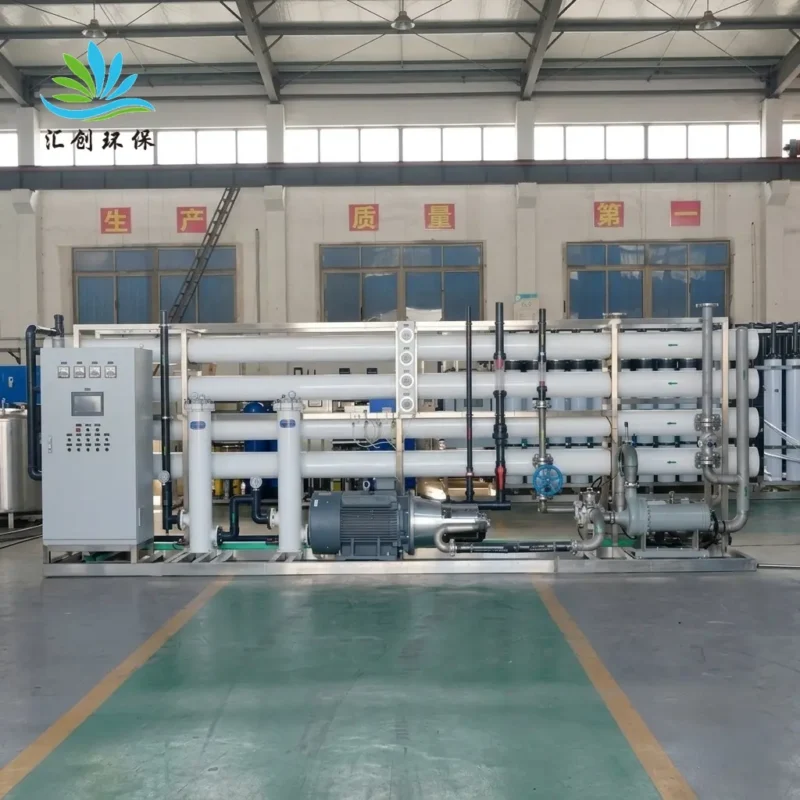
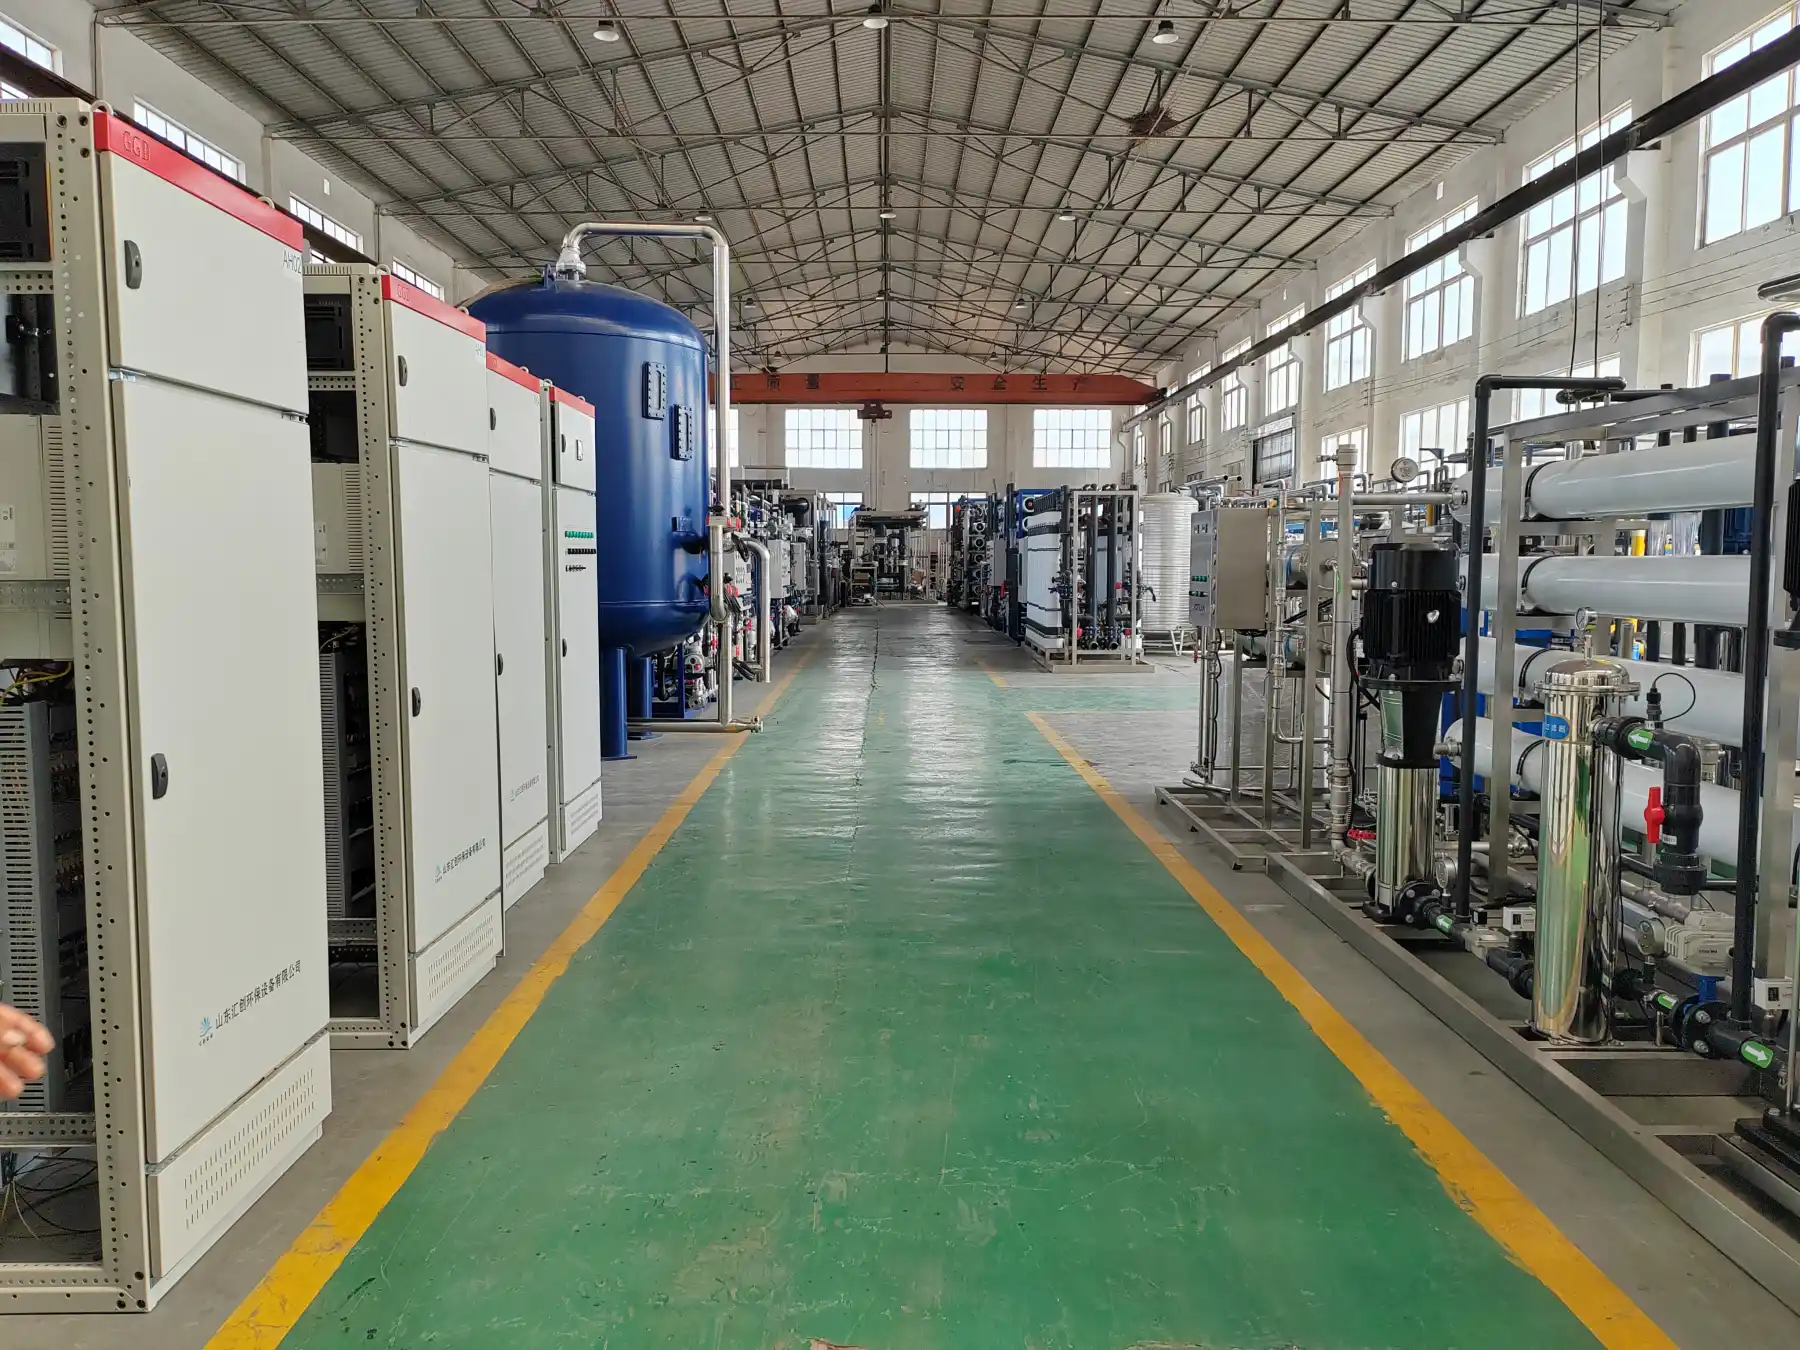
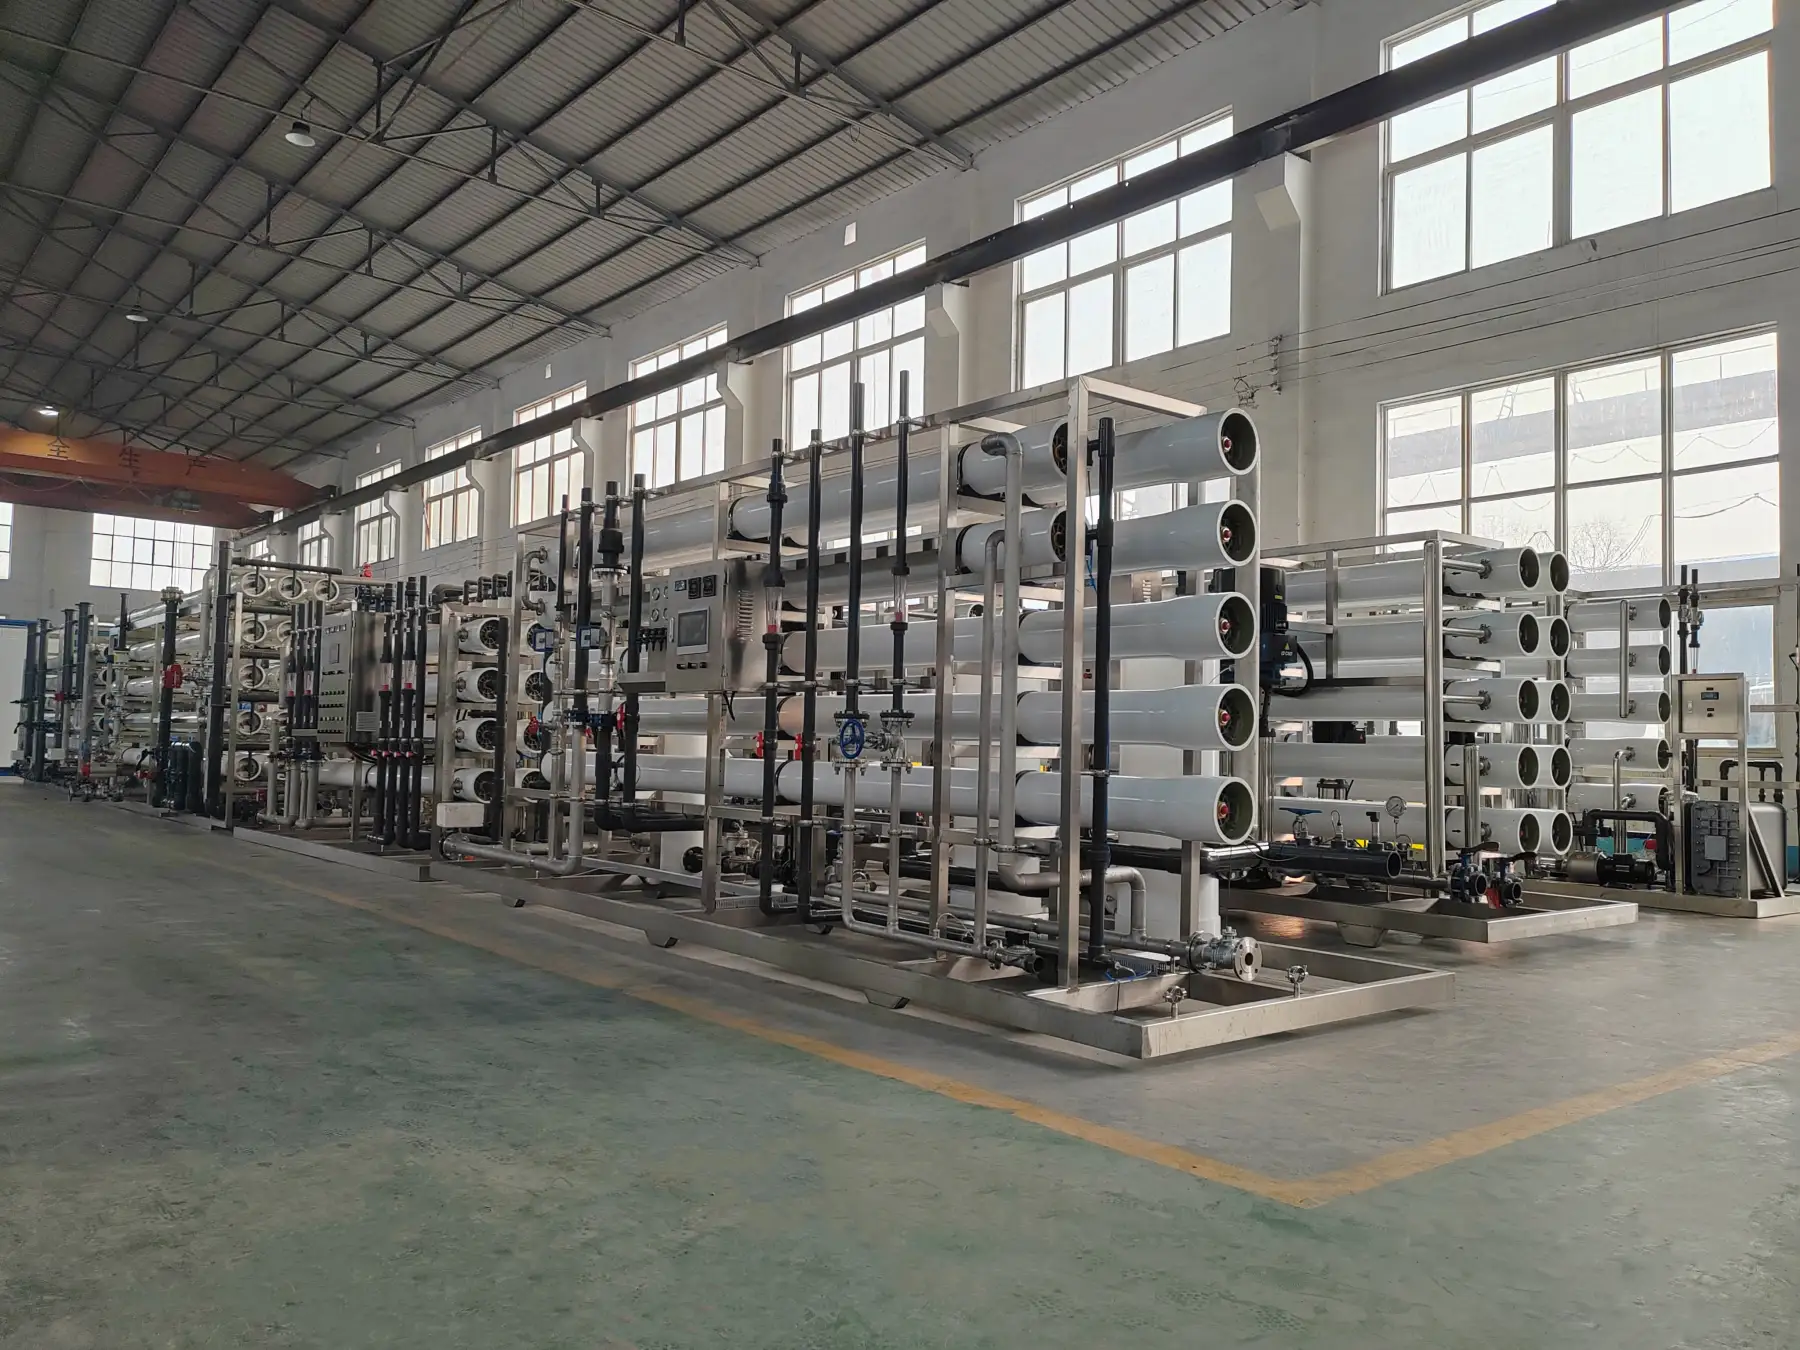
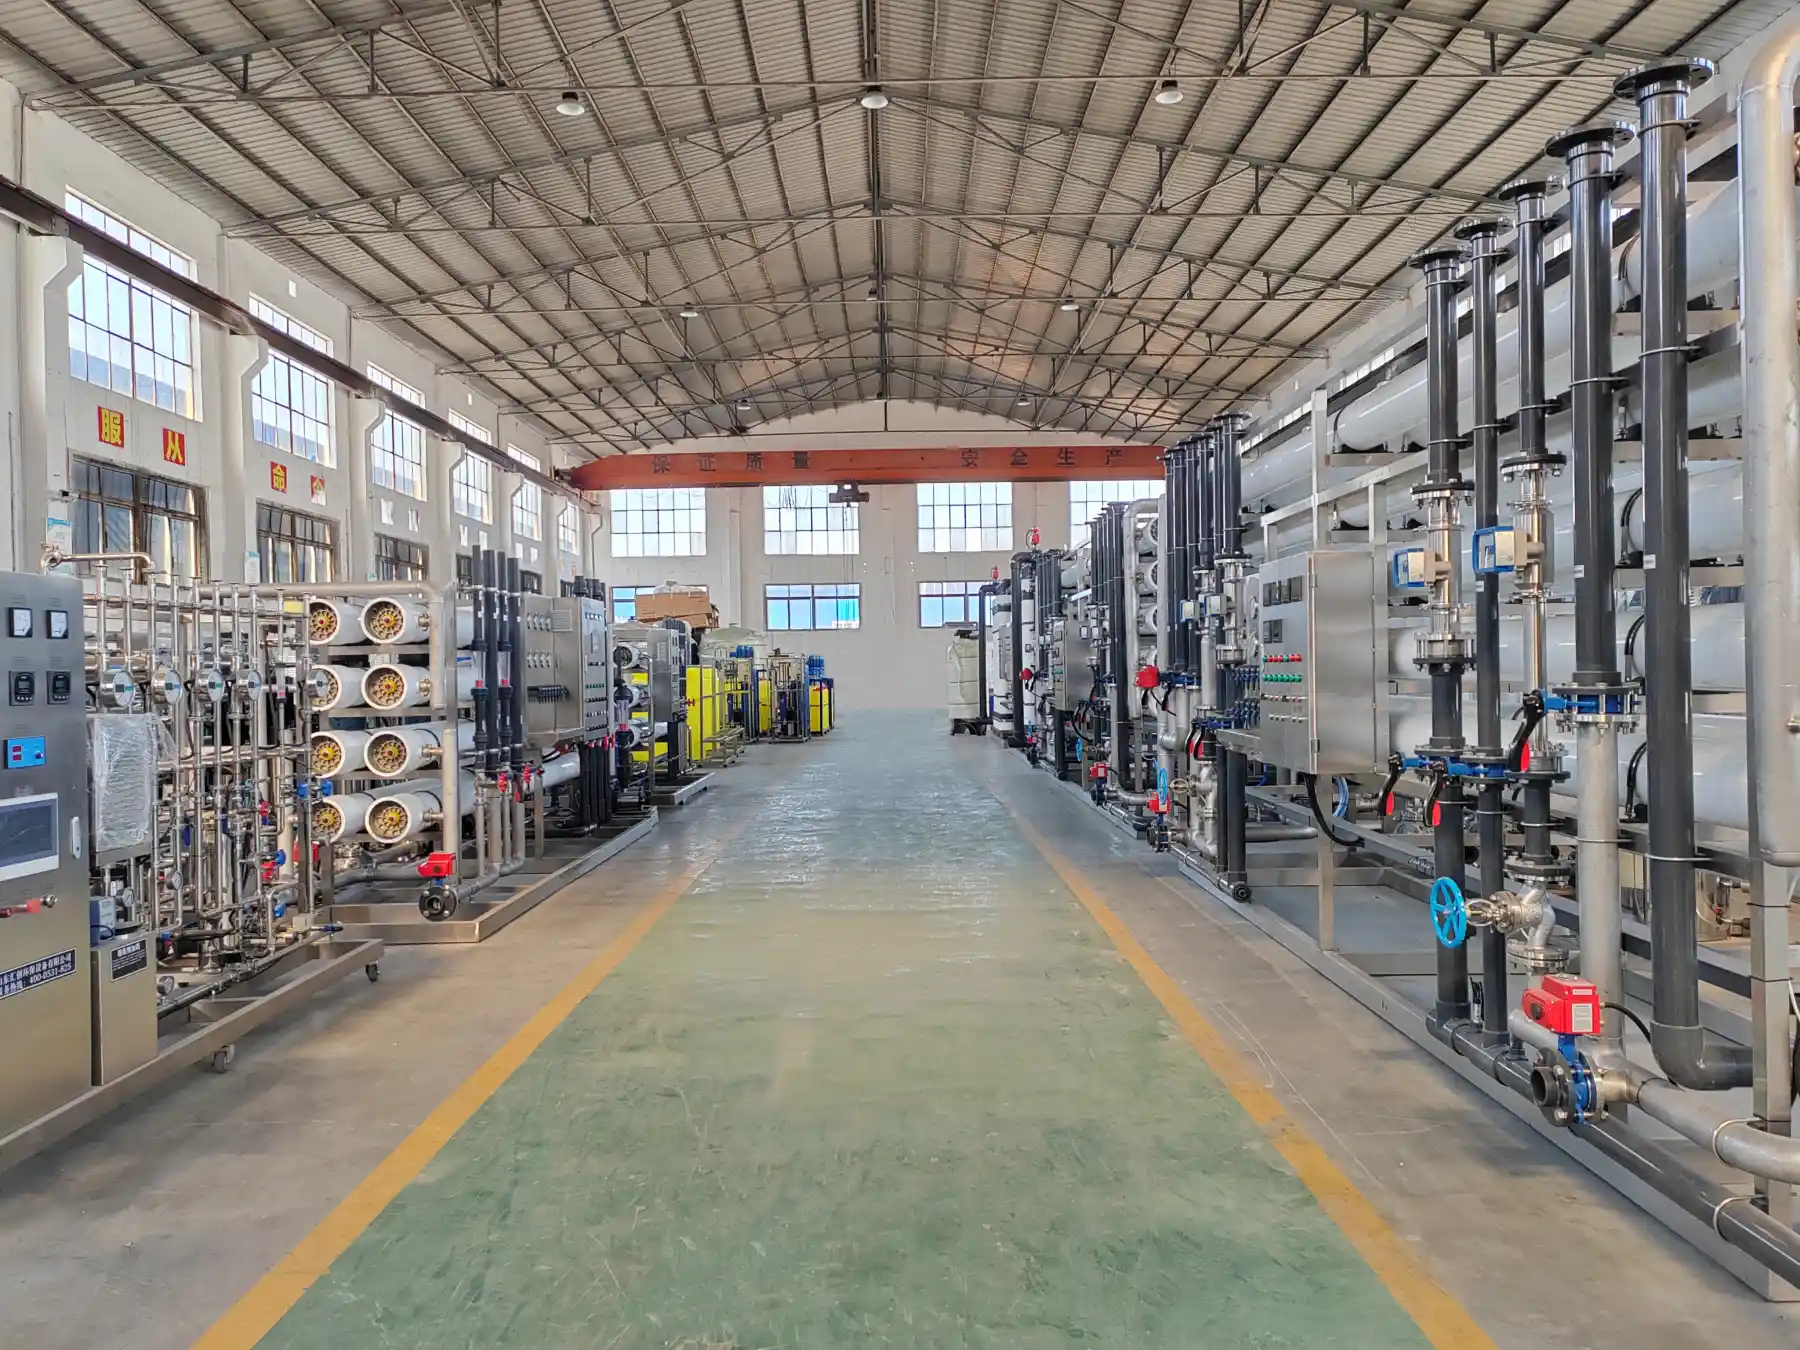
The 50 T/H Industrial Reverse Osmosis System designed and manufactured by Shandong Huichuang Environmental Protection Equipment Co., Ltd. is a heavy-duty, skid-mounted pure water purification system. Tailored for heavy industries with immense daily water demands, this RO water treatment plant features a rugged 5-stage treatment process that thoroughly purifies municipal tap water or underground well water into high-quality process water.
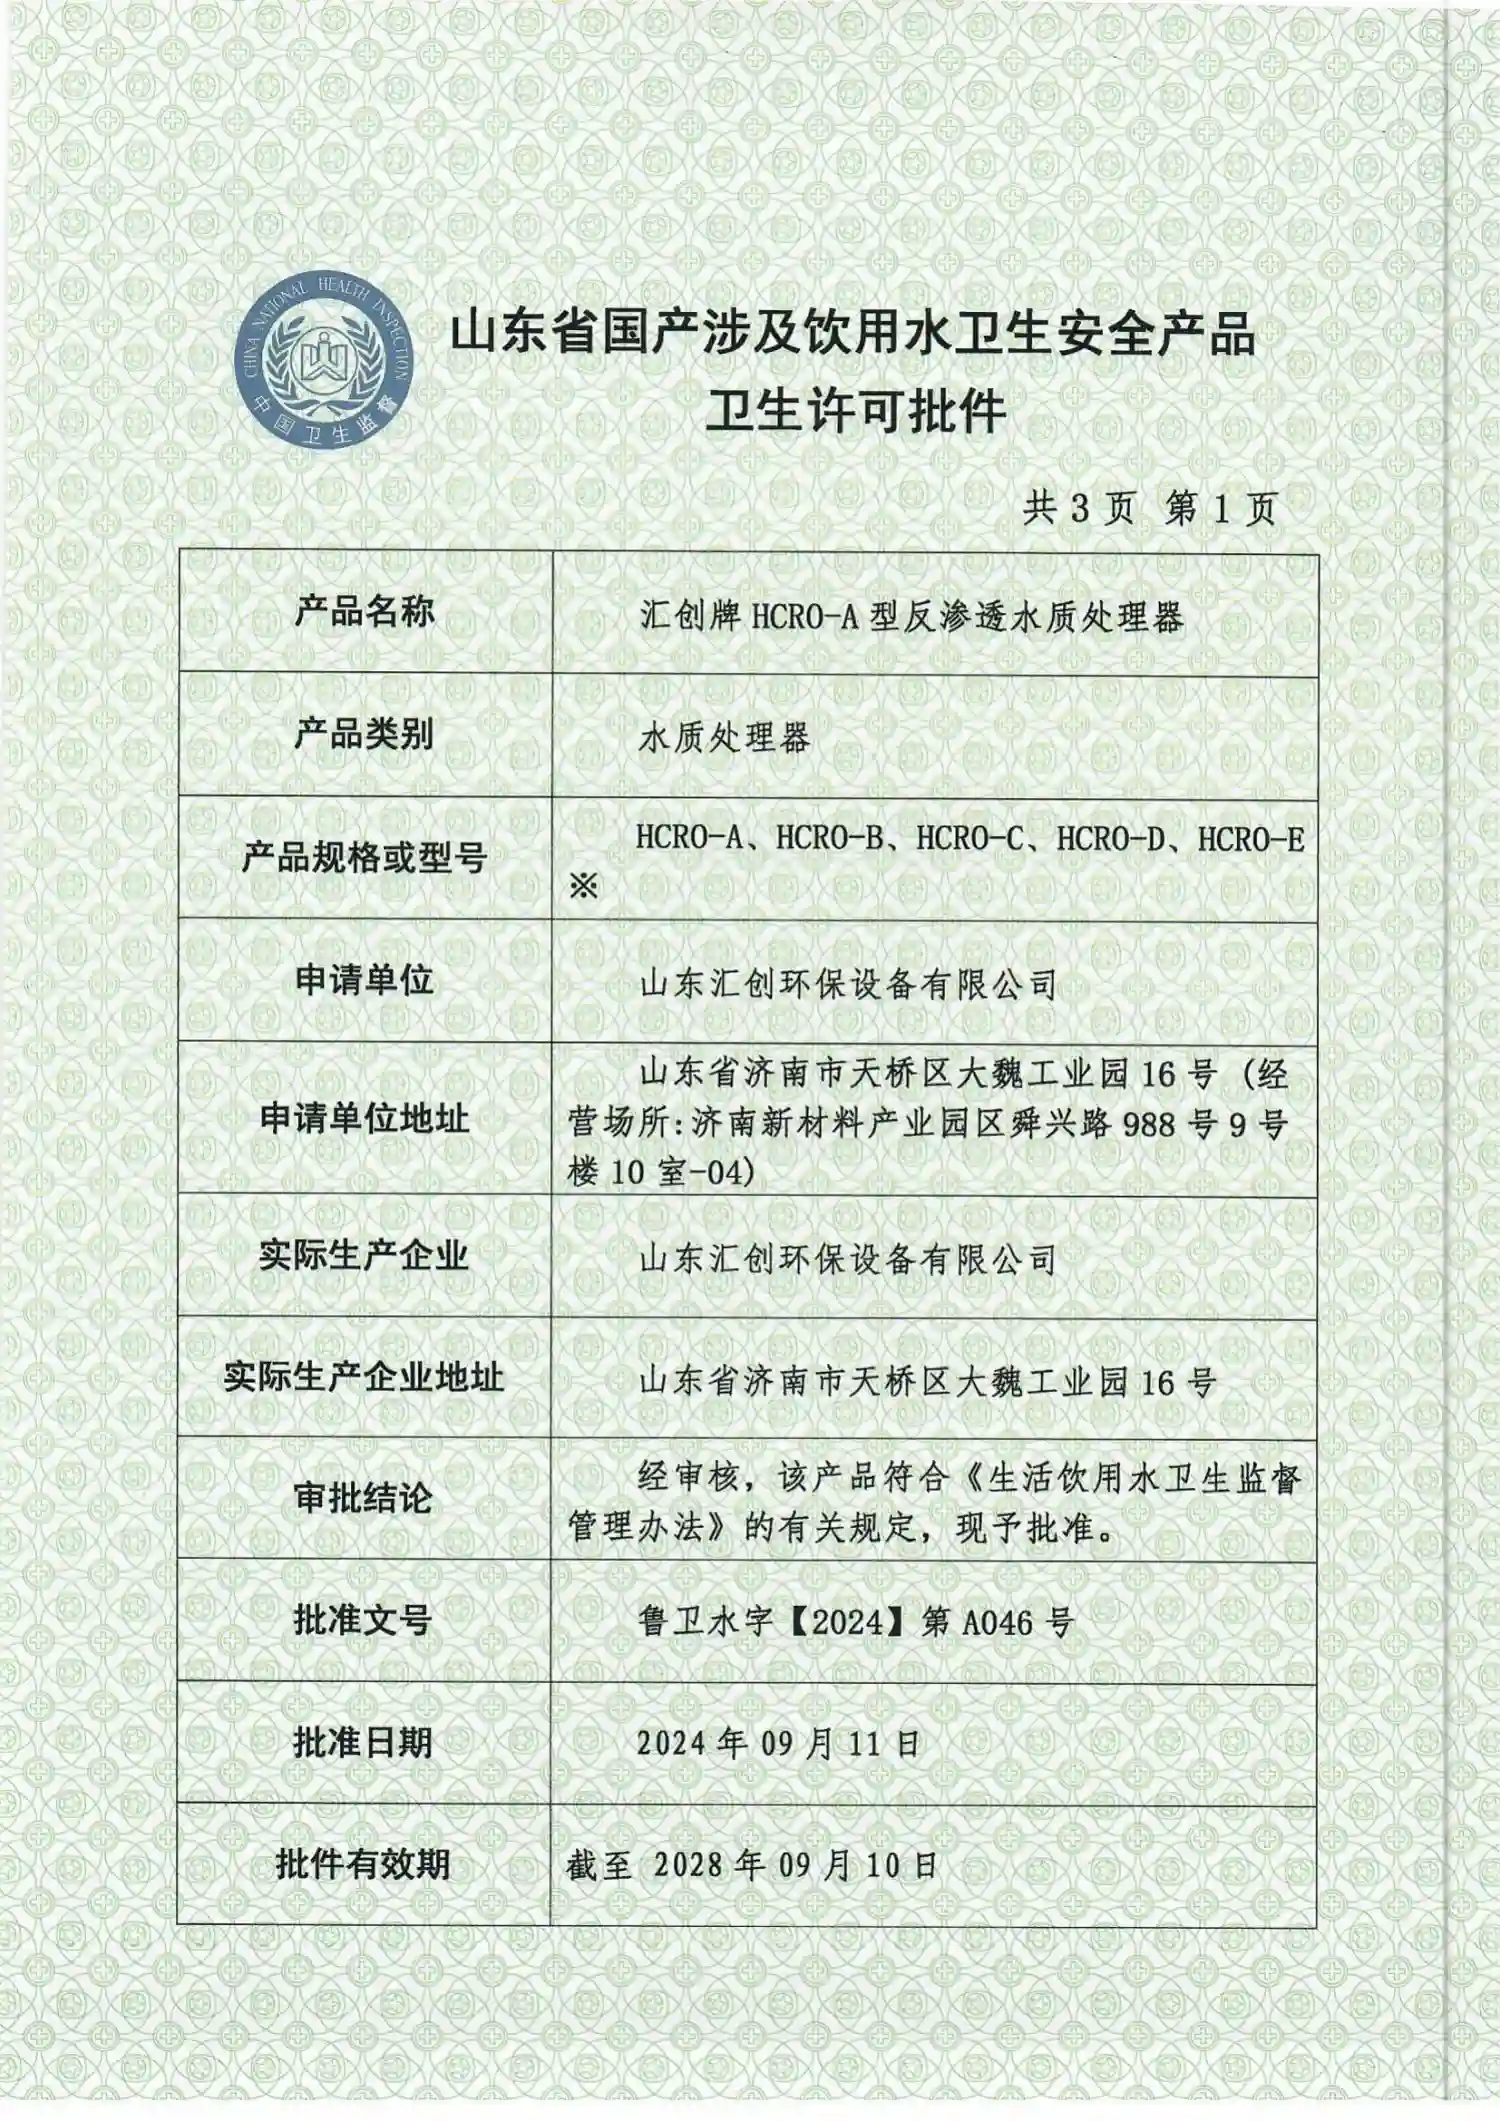
Compliant with strict industrial and sanitary guidelines (including the CJ94-2005 drinking water quality standards), our 50,000 LPH system ensures continuous, stable operation, massive turbidity reduction, and excellent desalination performance, helping global enterprises achieve energy reduction and green manufacturing.
Technical Specifications & Product Parameters
To assist B2B procurement managers and EPC contractors, here are the standard technical specifications of our 50 T/H Industrial RO system (Model: HC-RO-50T~120T/H):
| Parameter Item | Industrial Specification Details |
|---|---|
| Production Capacity | 50 Tons / Hour (Scalable up to 120 T/H per skid) |
| Working Operating Pressure | 1.0 – 1.5 MPa (High-efficiency pressure optimization) |
| Total Power Rating | 110 – 220 KW |
| Power Supply Required | 380V / 50Hz (Industrial Three-Phase) |
| Water Recovery Rate | 60% – 75% (Highly sustainable & cost-saving) |
| Applicable Source Water | Municipal Tap Water, Groundwater, Deep Well Water |
| Treatment Process | Advanced 5-Stage Treatment / Fully Automated Control |
| Design & Quality Standards | CJ94-2005 Standard for Drinking Water Quality |
| System Dimensions | Custom-designed based on client’s site layout |
Key Advantages of Our 50 T/H Industrial RO Equipment
- Real-Time Online Water Quality Monitoring: Integrated with high-precision sensors and multi-parameter instruments, the system constantly tracks effluent conductivity, TDS, and flux changes. This guarantees that your treated water consistently complies with strict production requirements.
- Premium Top-Tier RO Membranes: We source membranes exclusively from globally recognized, top-tier brands. This ensures an outstanding salt rejection profile, superb chemical resistance, a significantly extended membrane lifespan, and a much lower total cost of ownership (TCO).
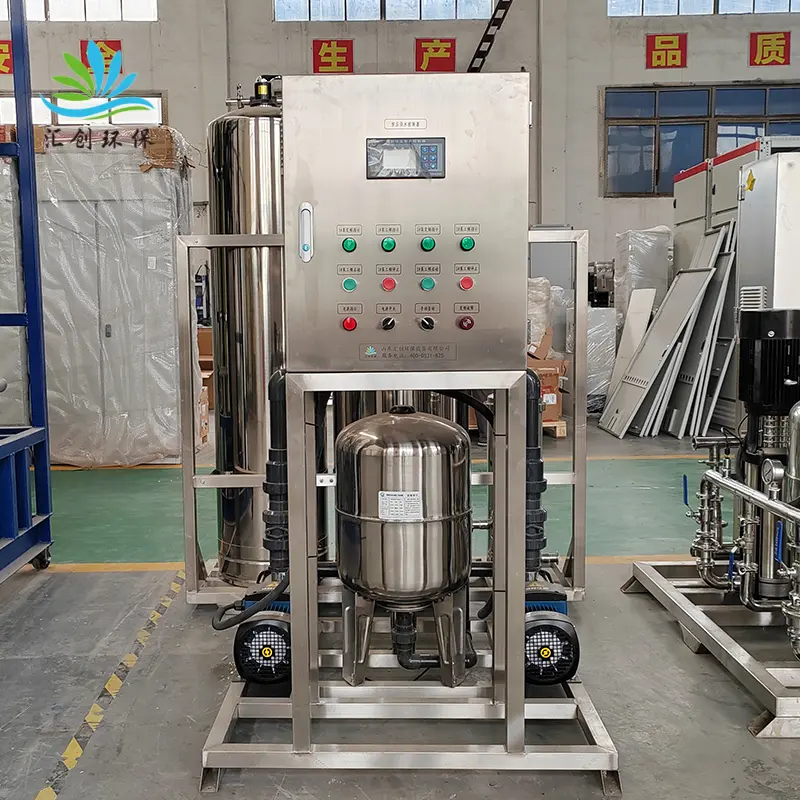
- Smart PLC Fully Automated System: Features a high-end PLC controller with a user-friendly HMI touch screen. The plant achieves fully automated startup, shut-down, backwashing, and safety interlocks, reducing manual maintenance and on-site labor to an absolute minimum.
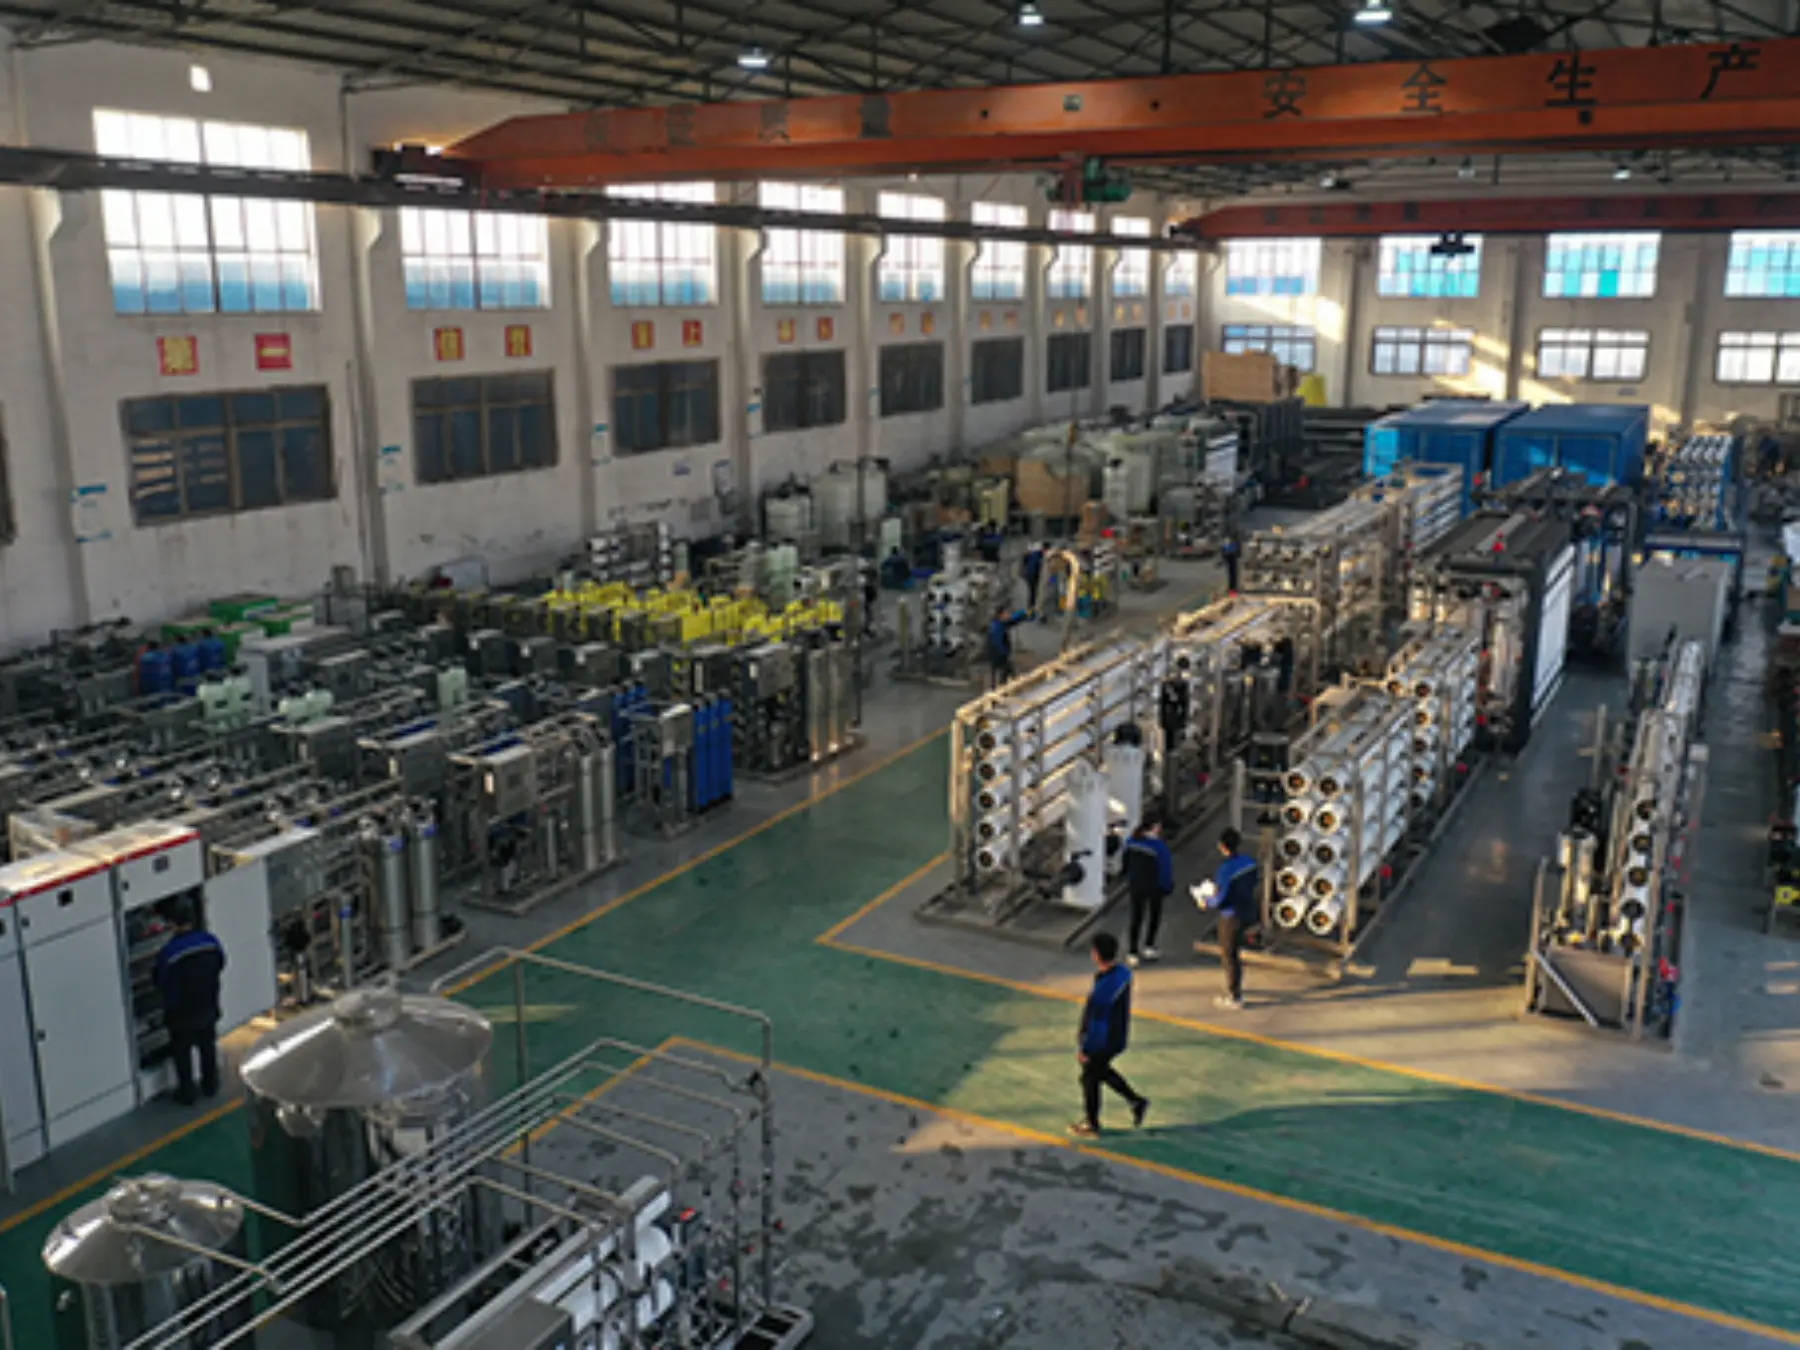
- Tailored Non-Standard Customization: Backed by our 15,000 sqm production facility, 15 senior engineers, and 30+ technicians, we specialize in customizing skid arrangements, pump configurations, and chemical dosing systems to perfectly match local raw water chemistry.
B2B Target Applications & Industries
Our heavy-duty 50,000 LPH reverse osmosis purification systems are deeply trusted by global EPC firms and factory owners across key industrial sectors:
- Food & Beverage: Ingredient blending, product processing, and high-purity washing water.
- Chemical & Petrochemical: Process solution preparation, chemical synthesis, and industrial boiler feed water.
- Boiler & Power Infrastructure: Thermal power stations, high-pressure boiler makeup water, and cooling tower loop replenishment.
- Wastewater Reclamation (Midiwater): Deep concentration, advanced wastewater treatment, and eco-friendly factory water reuse.
Frequently Asked Questions (FAQ)
How do you achieve a 60% to 75% water recovery rate in a 50 T/H RO system?
Our system leverages specialized multi-stage concentrate staging and optional brine recirculation loops. By matching top-tier low-fouling membranes with optimal driving pressure (1.0-1.5 MPa), we maximize pure permeate extraction while securely keeping concentrated salt ions below precipitation scaling levels.
Can the layout be adjusted if our factory floor space is limited?
Absolutely. We specialize in non-standard, customized engineering layout designs. Our engineering team can arrange the membrane housings, multi-stage pumps, and pretreatment vessels into compact single-skid or multi-tier structures to perfectly accommodate your local mechanical room blueprint.
Partner with a Leading Source Factory: With over 30,000 clients served worldwide, Shandong Huichuang provides direct wholesale B2B pricing, complete CAD engineering schematics, and lifetime technical support. Contact our engineering team today to receive a free tailored proposal and competitive quotation for your 50 T/H RO water treatment project!
Reviews
There are no reviews yet.