

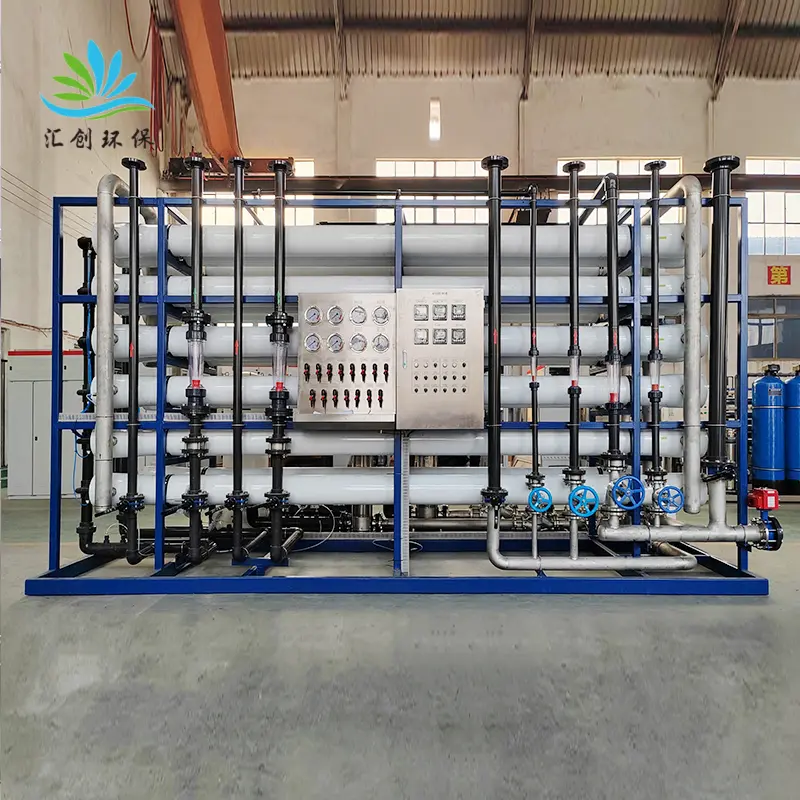
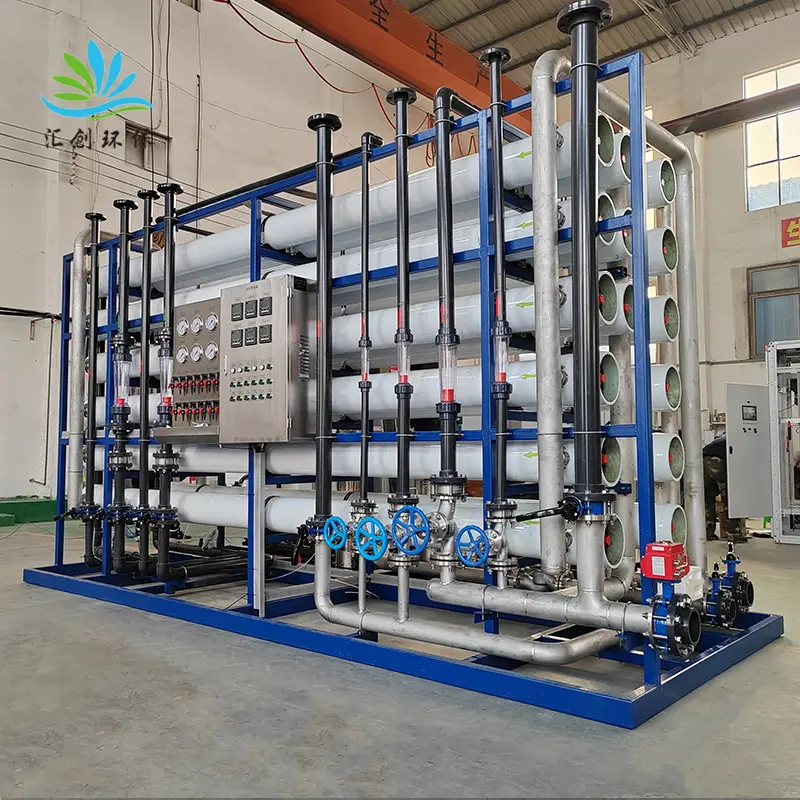
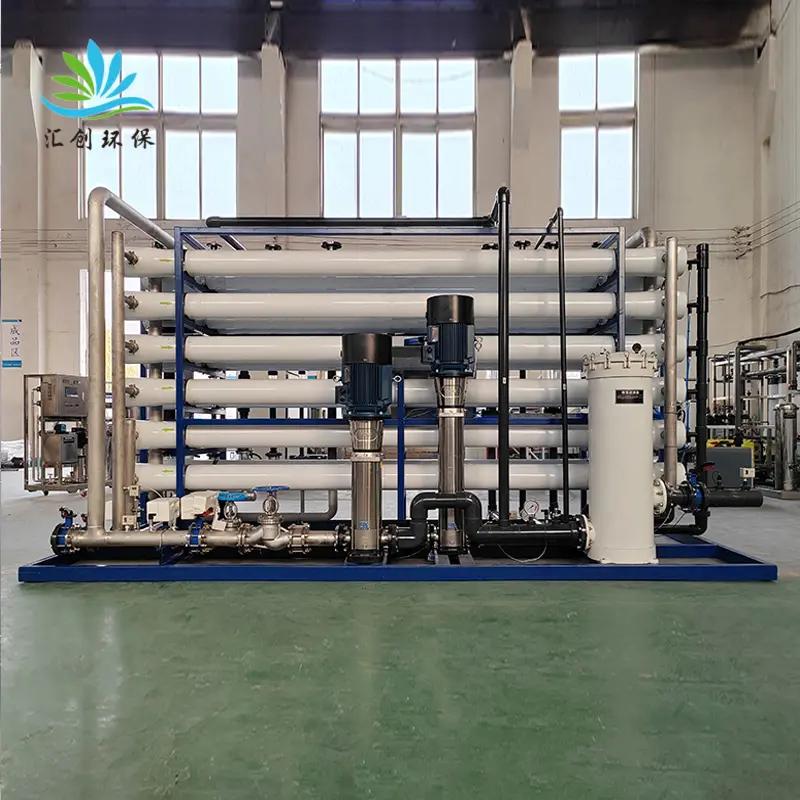
30 T/H High-Efficiency Low-Pressure Industrial Nanofiltration (NF) System
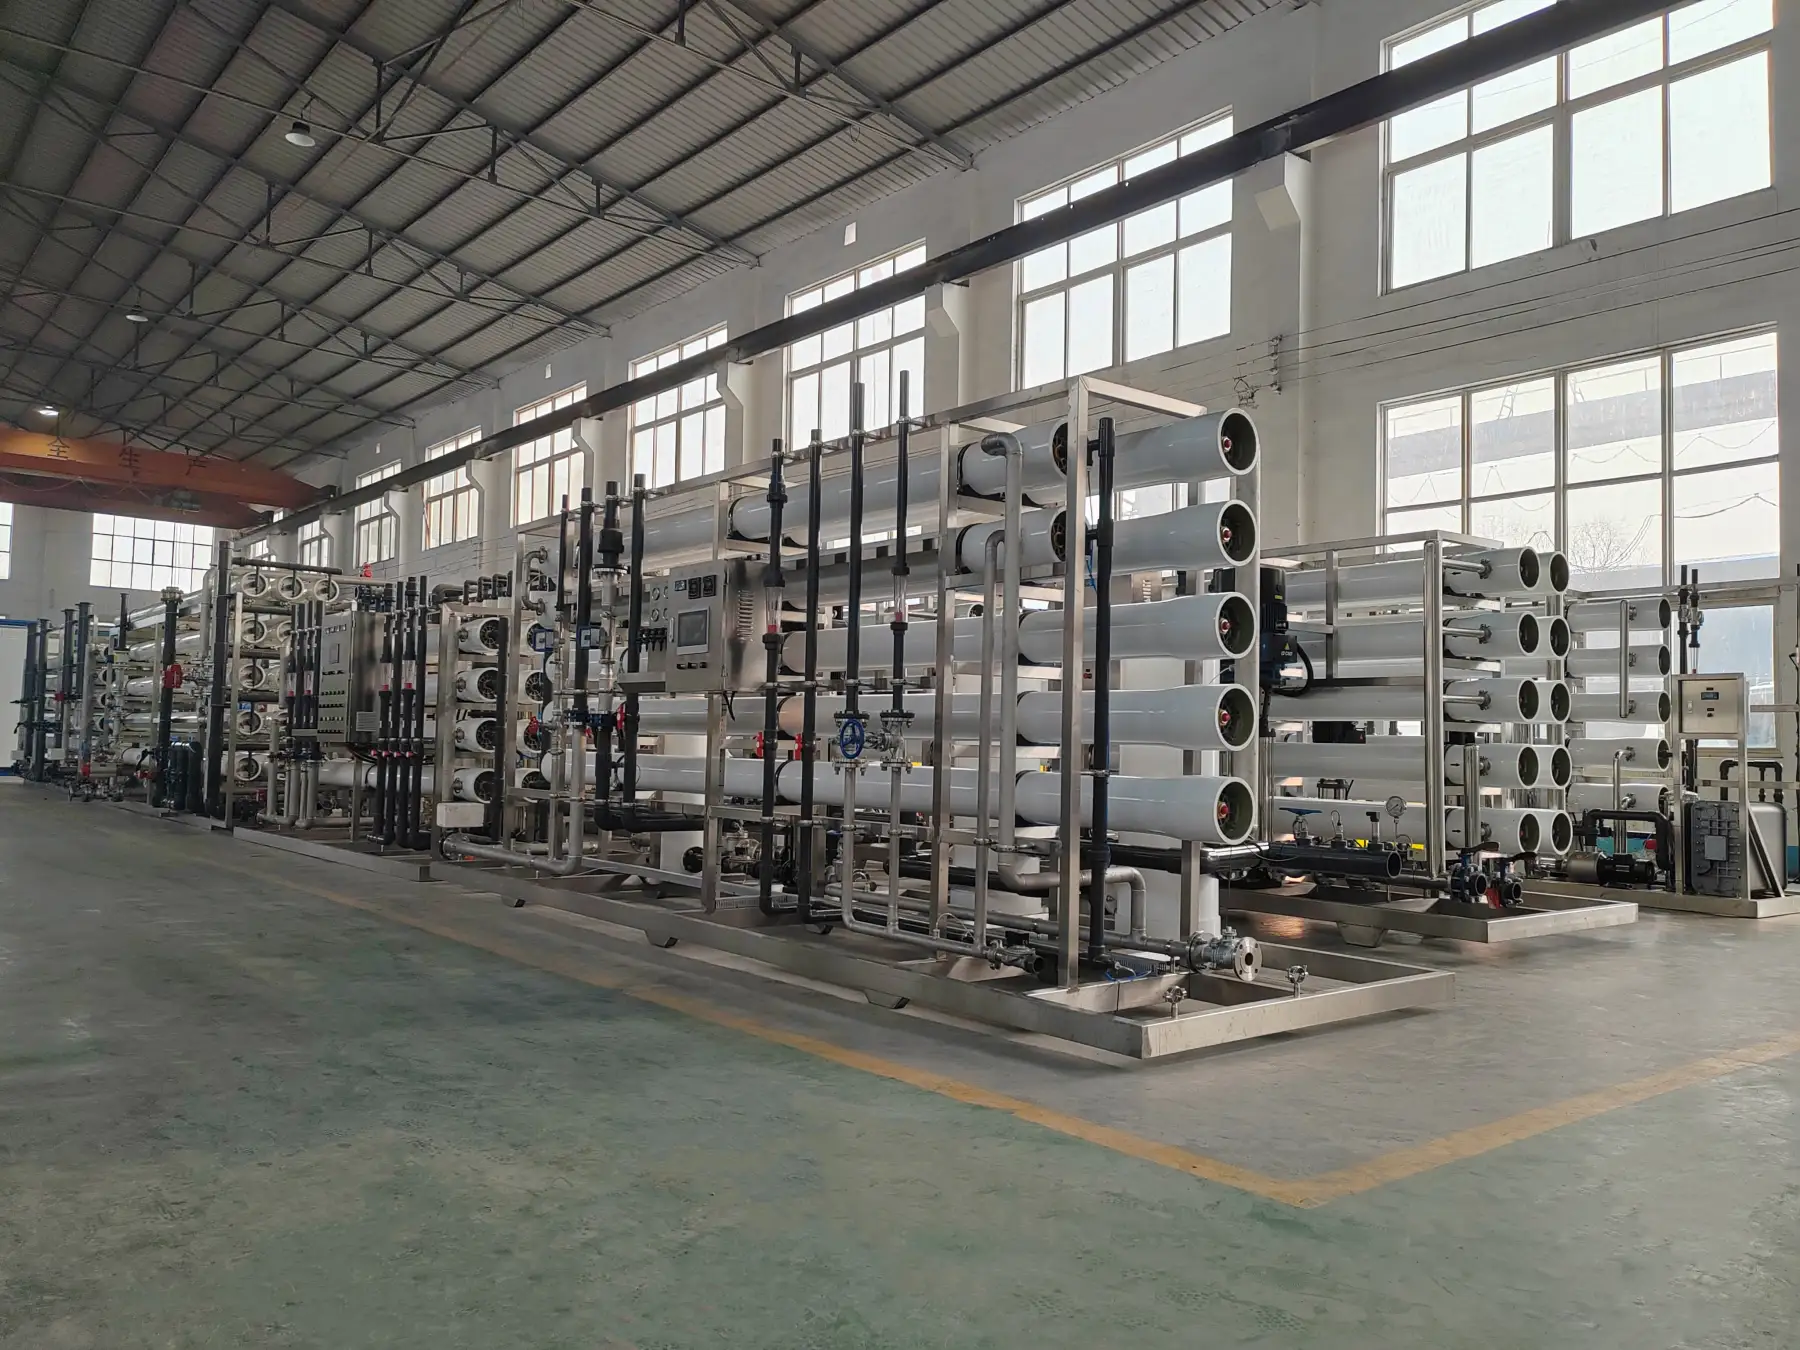
The 30 T/H Industrial Nanofiltration System engineered and manufactured by Shandong Huichuang Environmental Protection Equipment Co., Ltd. is a highly cost-effective, skid-mounted advanced water purification plant. Acting as a precision bridge between Ultrafiltration (UF) and Reverse Osmosis (RO), nanofiltration belongs to the category of advanced low-pressure membrane filtration equipment. It is primarily utilized for fine water purification, deep decolorization, water softening (hardness removal), and selective desalination.
Unlike traditional reverse osmosis plants that strip water of all components, our commercial NF system delivers selective molecular screening. It effectively traps harmful impurities while allowing beneficial, healthy minerals to pass through, yielding exceptional water taste and ideal chemical characteristics. Operating under significantly reduced hydraulic pressure, this 30,000 LPH system achieves massive power and water savings, making it the premier choice for modern industrial and municipal utility upgrades.
Technical Specifications & Operational Framework
To assist global B2B procurement managers, water engineering companies, and EPC contractors, here are the detailed specifications of our 30 T/H Industrial Nanofiltration equipment:
| Technical Parameter | Industrial Specification Details |
|---|---|
| Standard Flow Rate Capacity | 30 Tons / Hour (30,000 Liters Per Hour) |
| Filtration Mechanism | Low-Pressure NF Membrane Technology (Selective Ion Retention) |
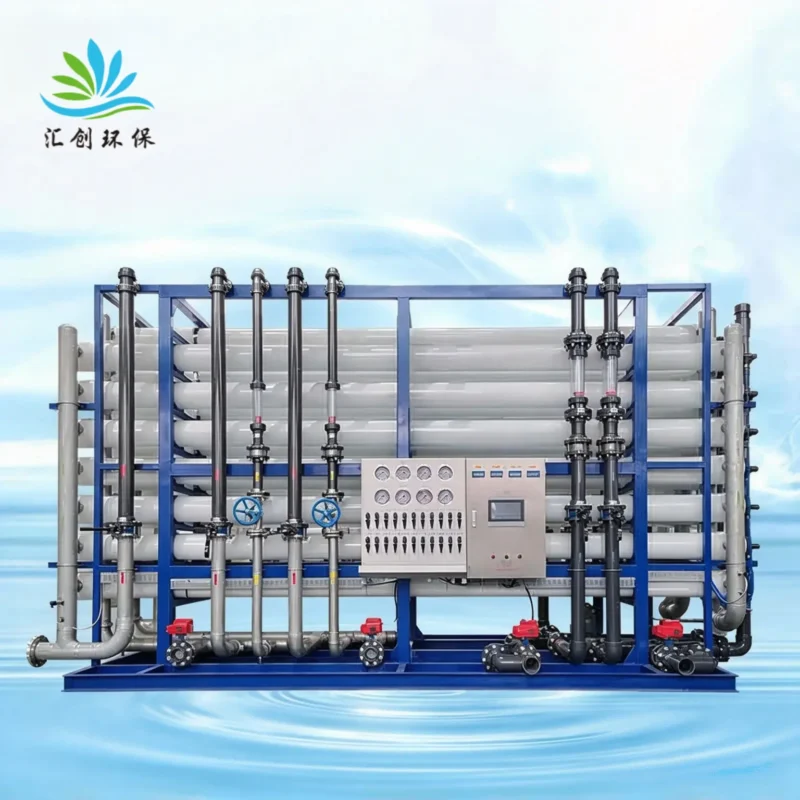
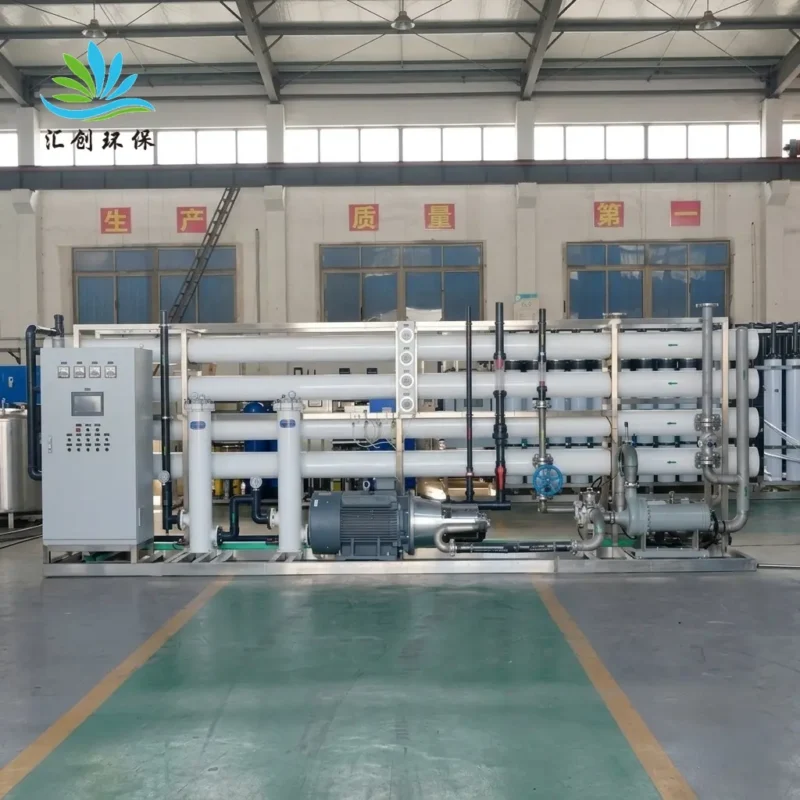
| Structural Blueprint | Heavy-Duty Protected Carbon Steel Base with Stainless Steel Control Panel |
| Monitoring Instrumentation | Centralized Liquid Flow Meters, High-Precision Pressure Gauges, Smart Sensors |
| Operating Control Design | Fully Automated PLC System (Smart Flushing, Automatic Inflow & Shut-down) |
| Power & Eco Profile | 380V / 50Hz Three-Phase, Pure Physical Separation (No Chemical Reagents) |
| Raw Water Adaptability | Highly Adaptive to Underground Well Water, Surface Water, Municipal Tap Water |
Key Advantages of Huichuang Industrial Nanofiltration Plants
- Selective Retention & Superior Effluent Quality: Equipped with precision-controlled pore-size NF membranes, the system efficiently intercepts colloids, macromolecular organics, pigments, odors, calcium/magnesium hardness ions, and heavy divalent salts. It completely eradicates common water supply issues such as yellowing, heavy scale buildup, and chemical impurities while retaining a natural, pleasant drinking water taste.
- Low Operating Pressure & Reduced Running Cost: Because NF membranes require far lower driving pressures compared to standard brackish water RO elements, the system operates with significantly downsized pump ratings. This translates to an eco-friendly operation that consumes far less electricity, cuts down on wastewater discharge, and dramatically lowers long-term utility bills.
- 100% Pure Physical Filtration with No Secondary Pollution: Our nanofiltration process is completely mechanical and physical. It requires no complex chemical dosing or hazardous regeneration reagents. This ensures zero secondary pollution, an environmentally sustainable carbon footprint, and minimal manual maintenance for long-term continuous uptime.
- Smart PLC Automation & Unattended Reliability: Built for continuous industrial deployment, the system features a smart centralized controller that automates water intake, high-efficiency membrane backwashing, forward flushing, and safety diagnostics. The compact, skid-mounted structure arrives pre-tested and ready for quick plug-and-play installation on-site.
B2B Target Applications & Fields
Our industrial-grade 30 T/H nanofiltration booster skids serve as the primary premium utility asset across a broad spectrum of commercial and industrial sectors:
- Commercial Drinking Water Upgrades: Direct large-scale potable water purification and mineral water refinement for high-end residential networks, school campuses, and hospitality hubs.
- Groundwater & Deep Well Remediation: Deep softening, color removal, and heavy-metal remediation of rural or industrial underground well water sources.
- Industrial Wastewater Reclamation: Advanced polishing and tertiary treatment of industrial middle-water, enabling closed-loop sustainable recycling.
- Material Concentration & Chemical Processing: Low-temperature concentration, desalt separation, and compound clarification for food, beverage, and chemical process streams.
Frequently Asked Questions (FAQ)
How does nanofiltration cut operating costs compared to standard Reverse Osmosis (RO)?
Nanofiltration operates as a loose RO/tight UF hybrid membrane with high monovalent salt transmission. Because it allows basic monovalent salts to pass through while targeting complex scales and heavy ions, the required osmotic backpressure is much lower. This allows the system to achieve identical purification targets for hardness and color while utilizing up to 30% to 40% less electrical power.
What makes this system a “green, zero-pollution” solution for my facility?
Unlike ion-exchange water softeners or traditional mixed-bed resin filters that demand thousands of liters of salt brine, acids, or alkalis for chemical regeneration cycles, our nanofiltration skid relies purely on hydraulic pressure and cross-flow membrane separation. There are no hazardous chemicals to handle, store, or neutralize, guaranteeing an entirely eco-friendly green production workflow.
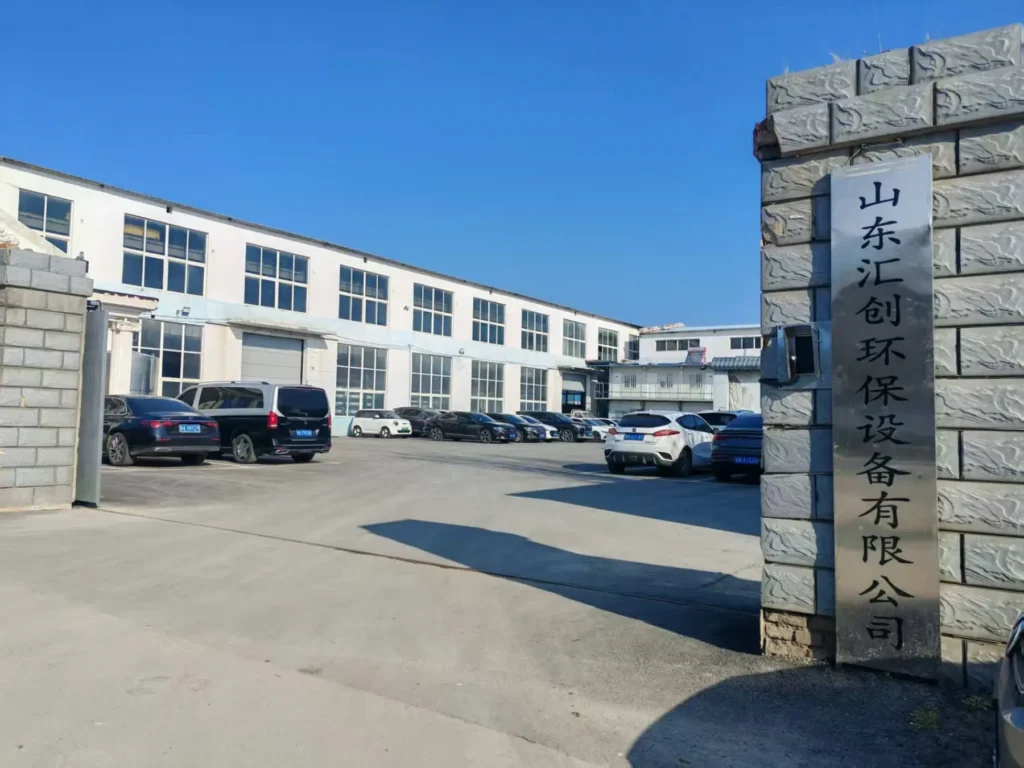
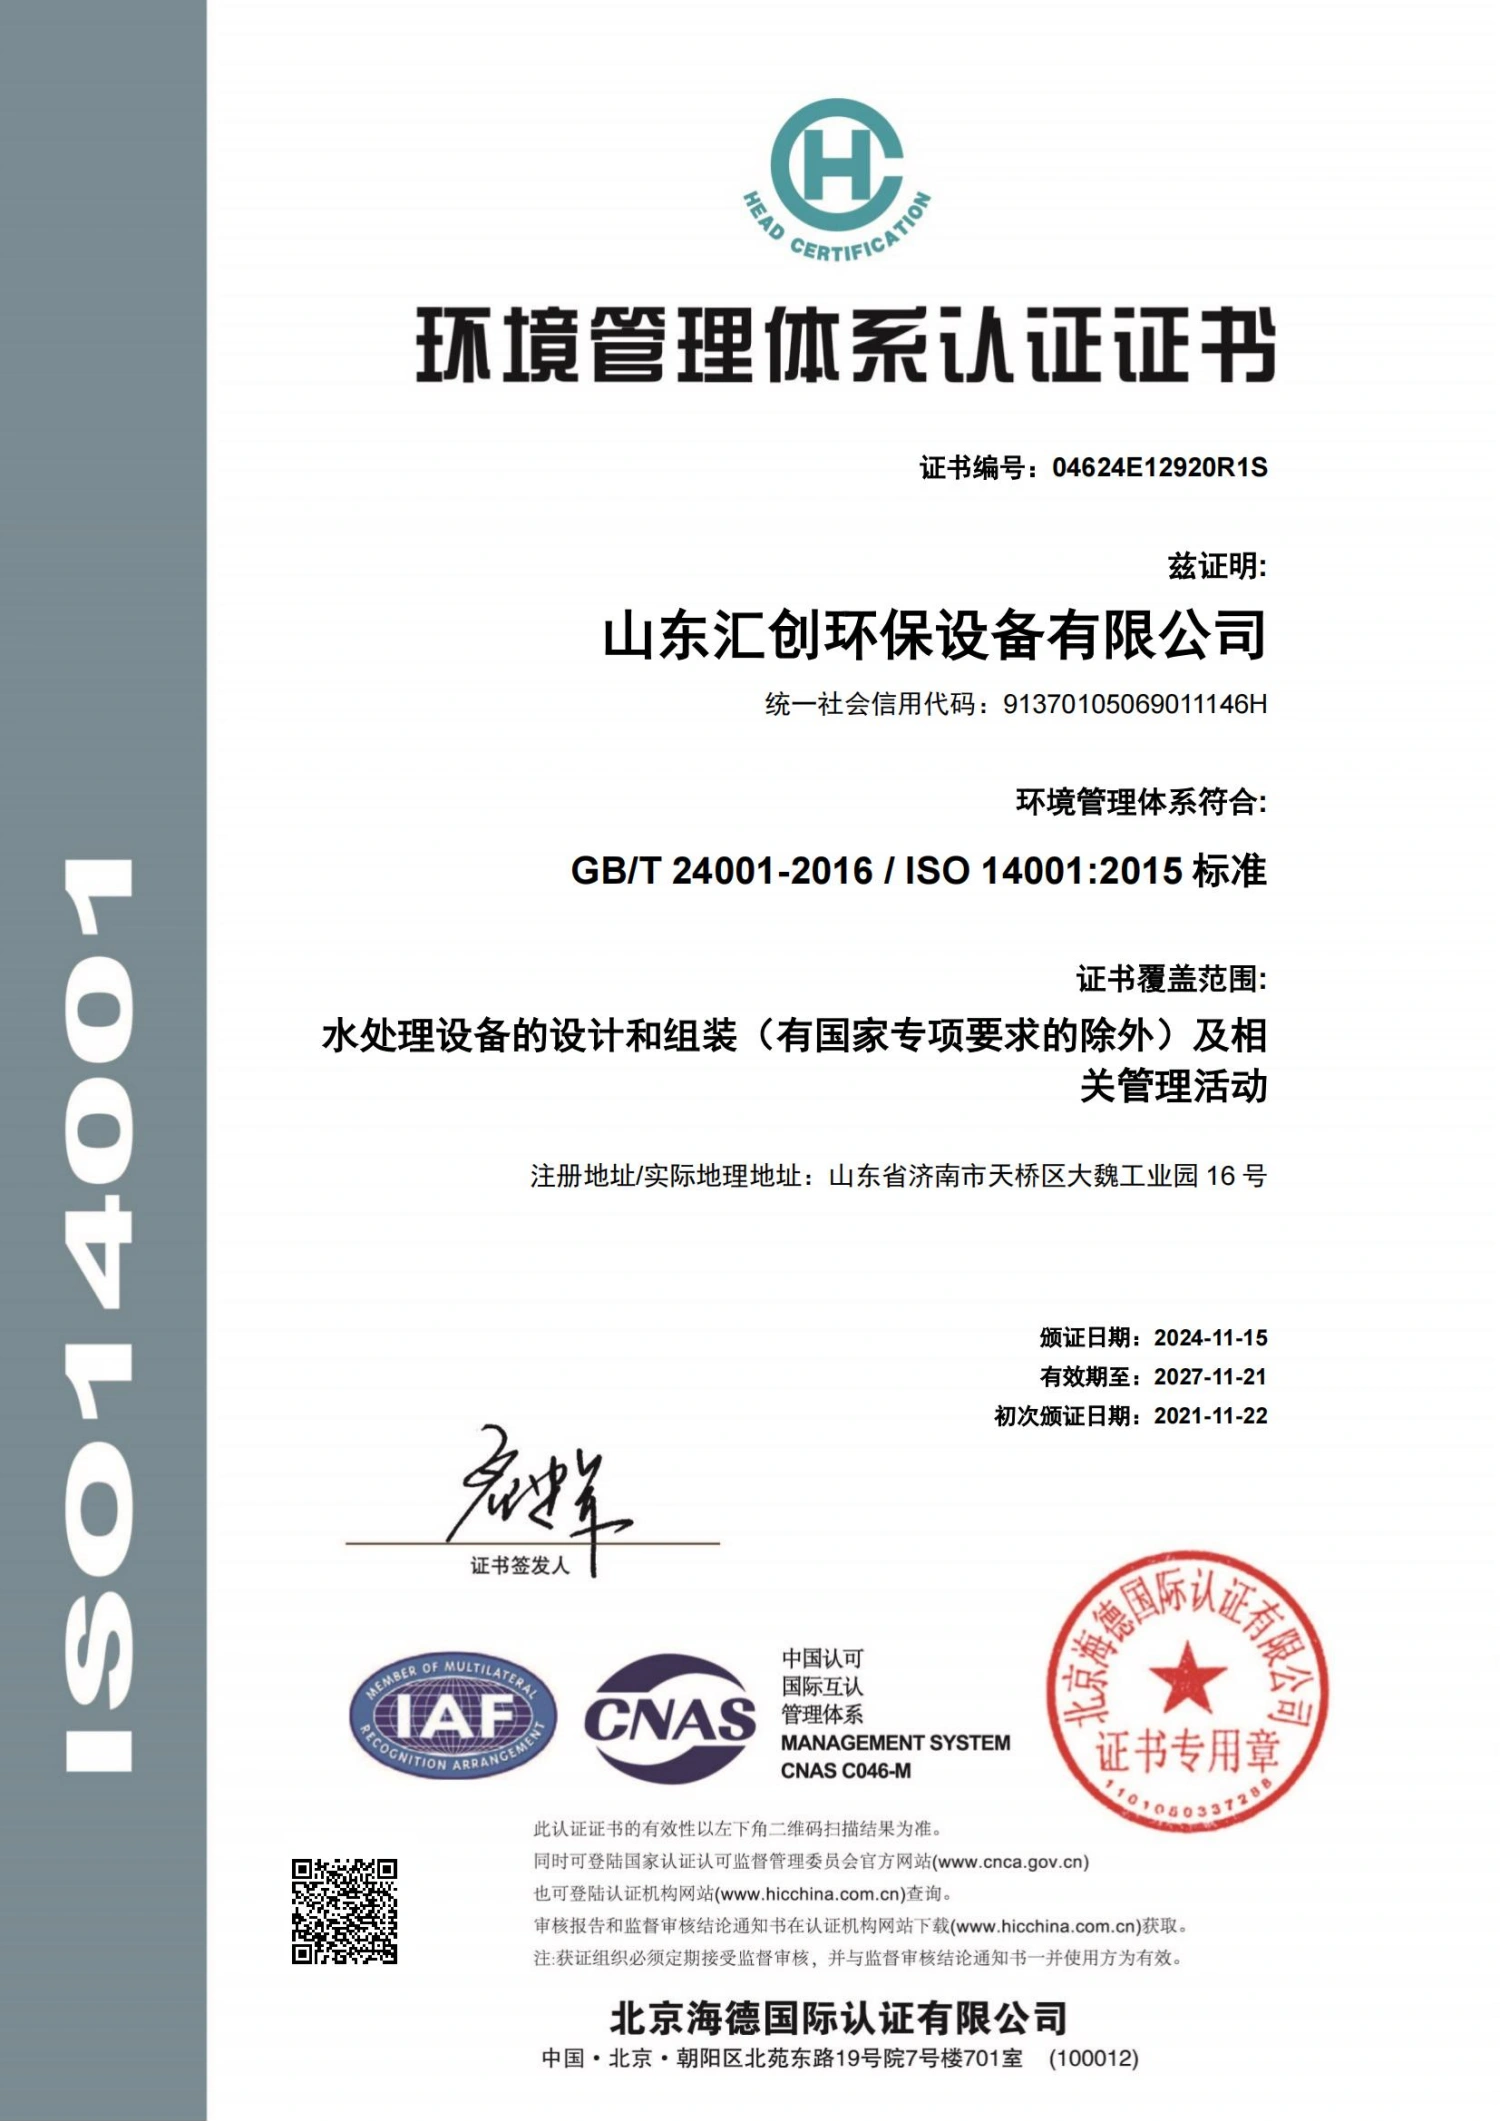
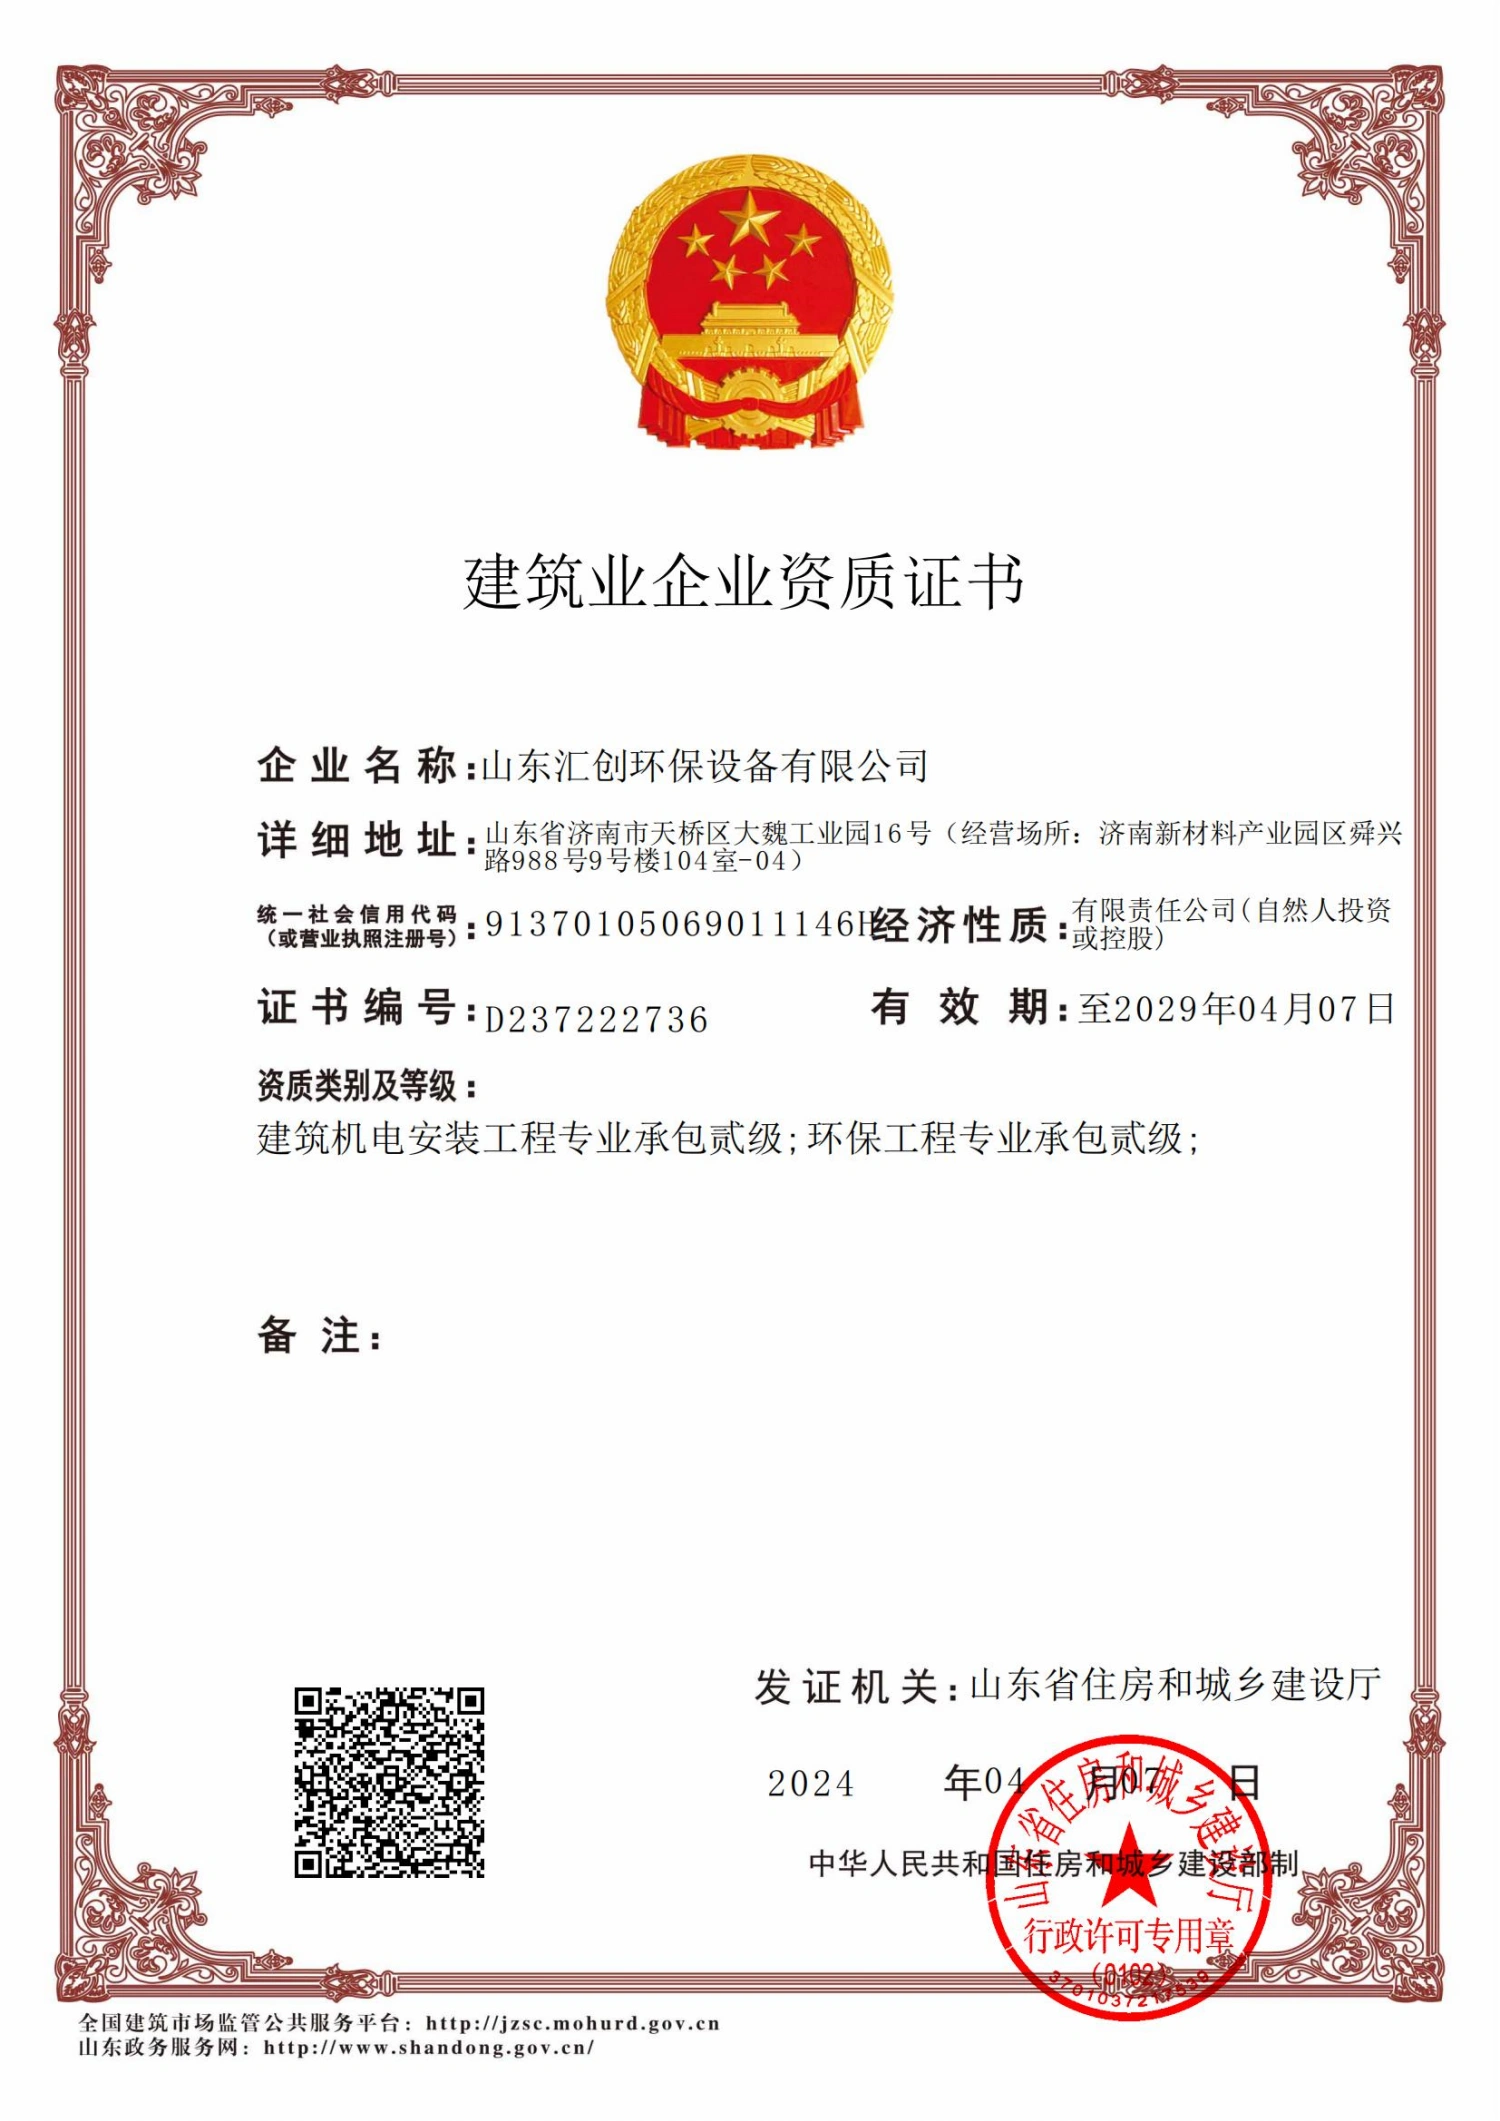
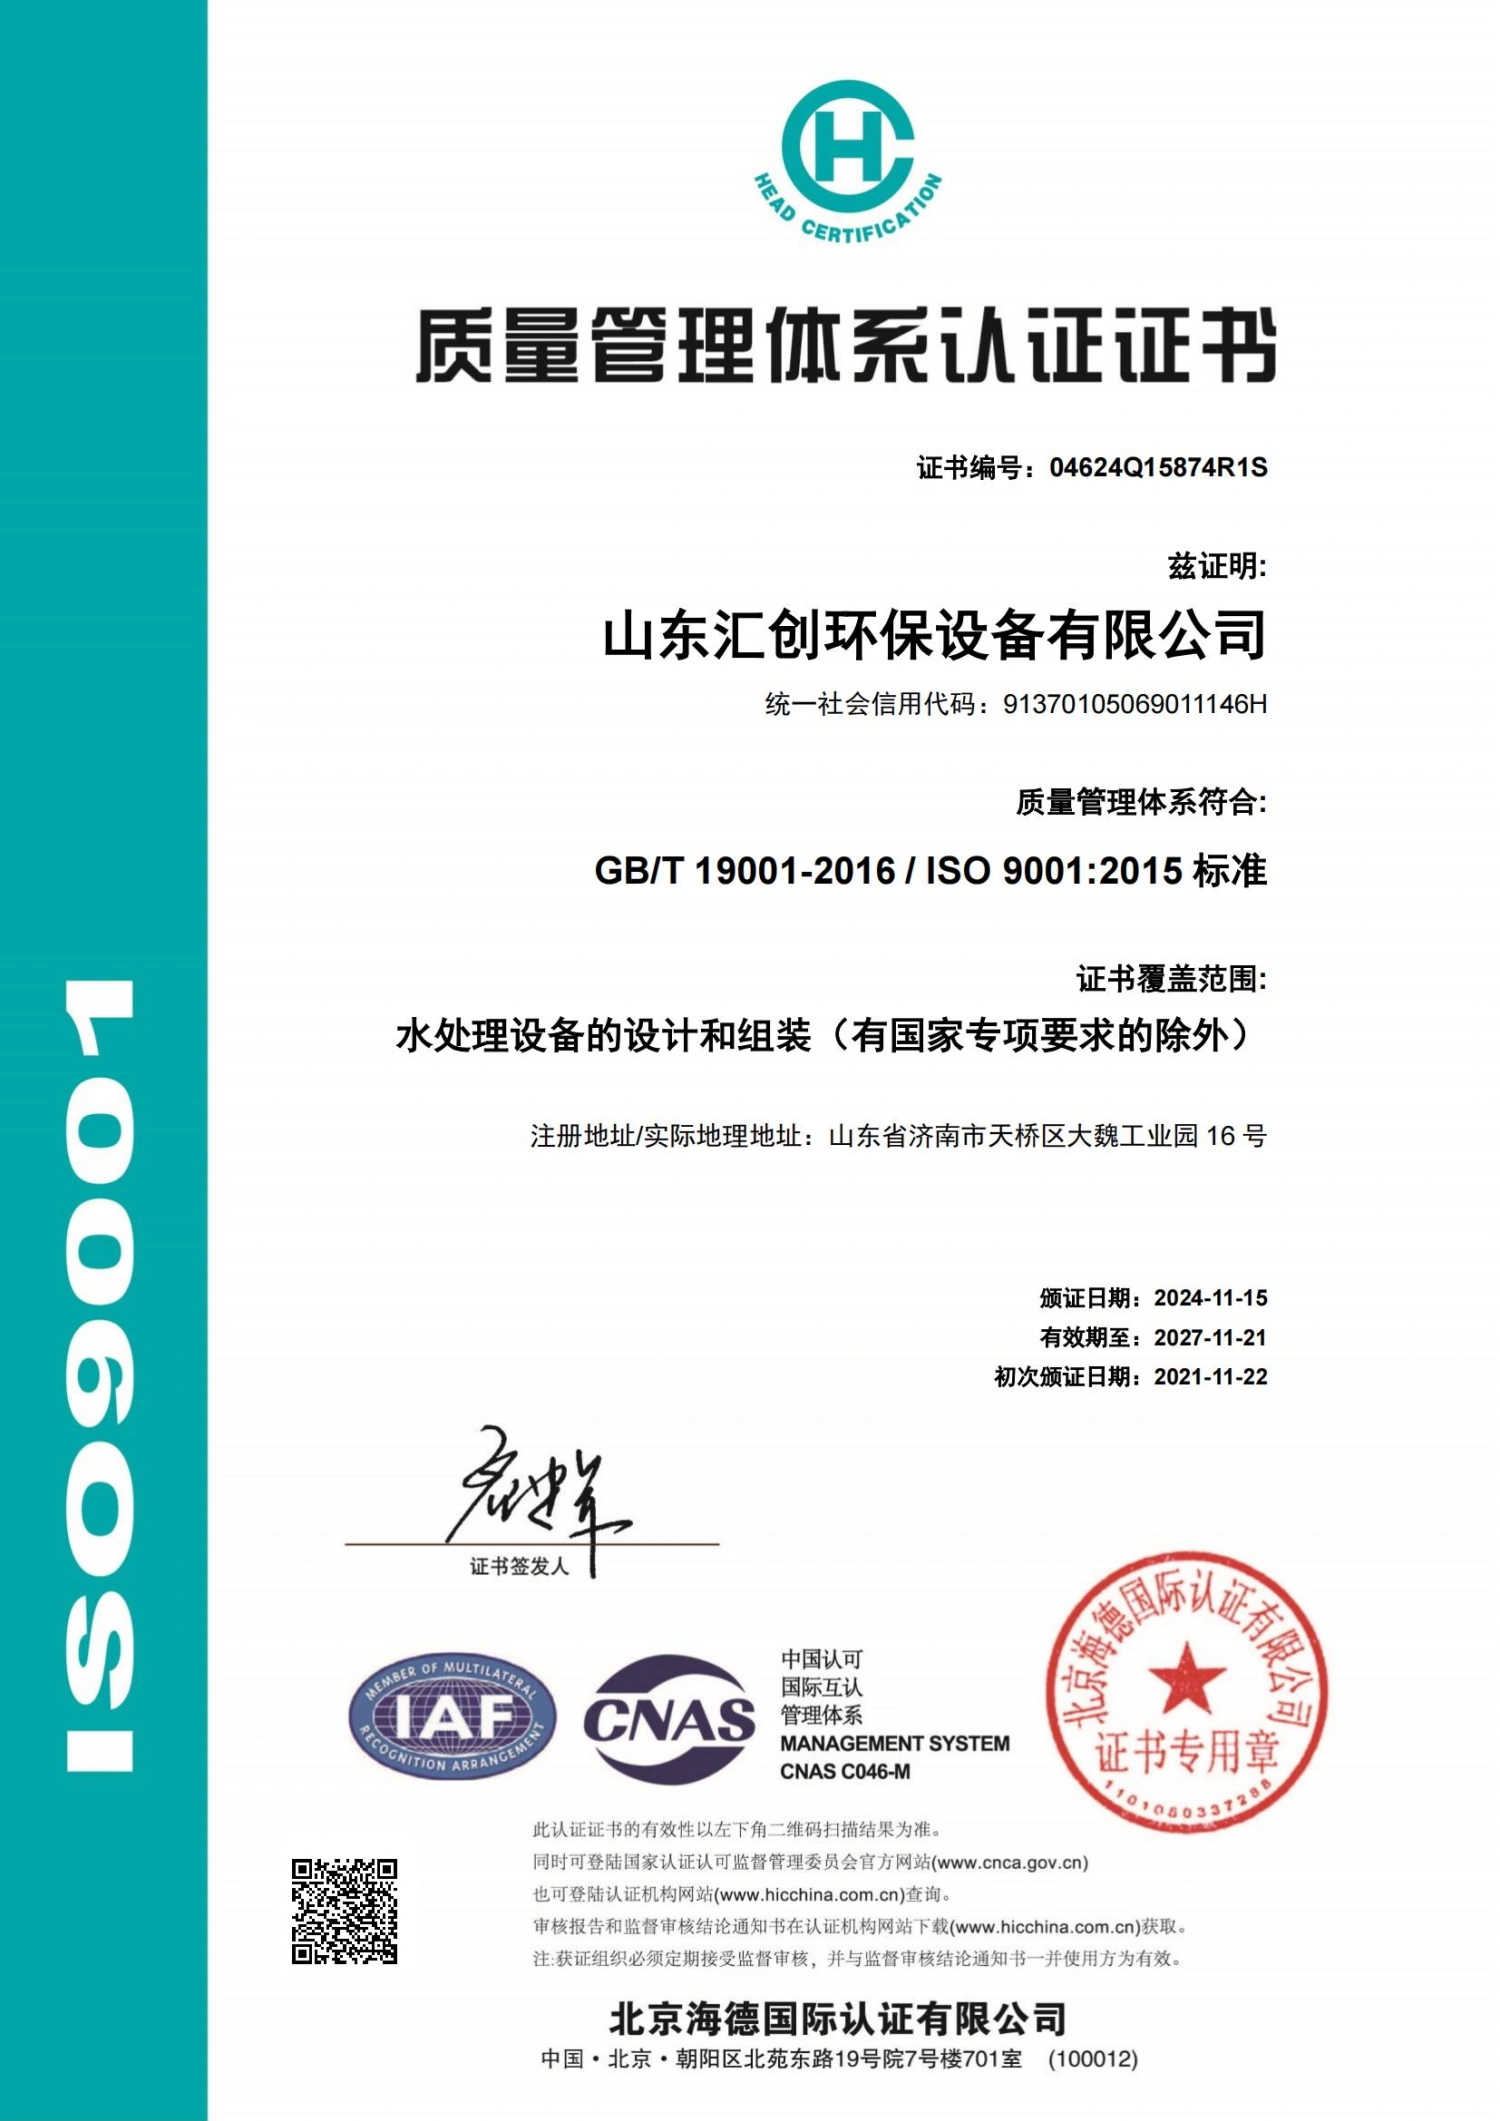
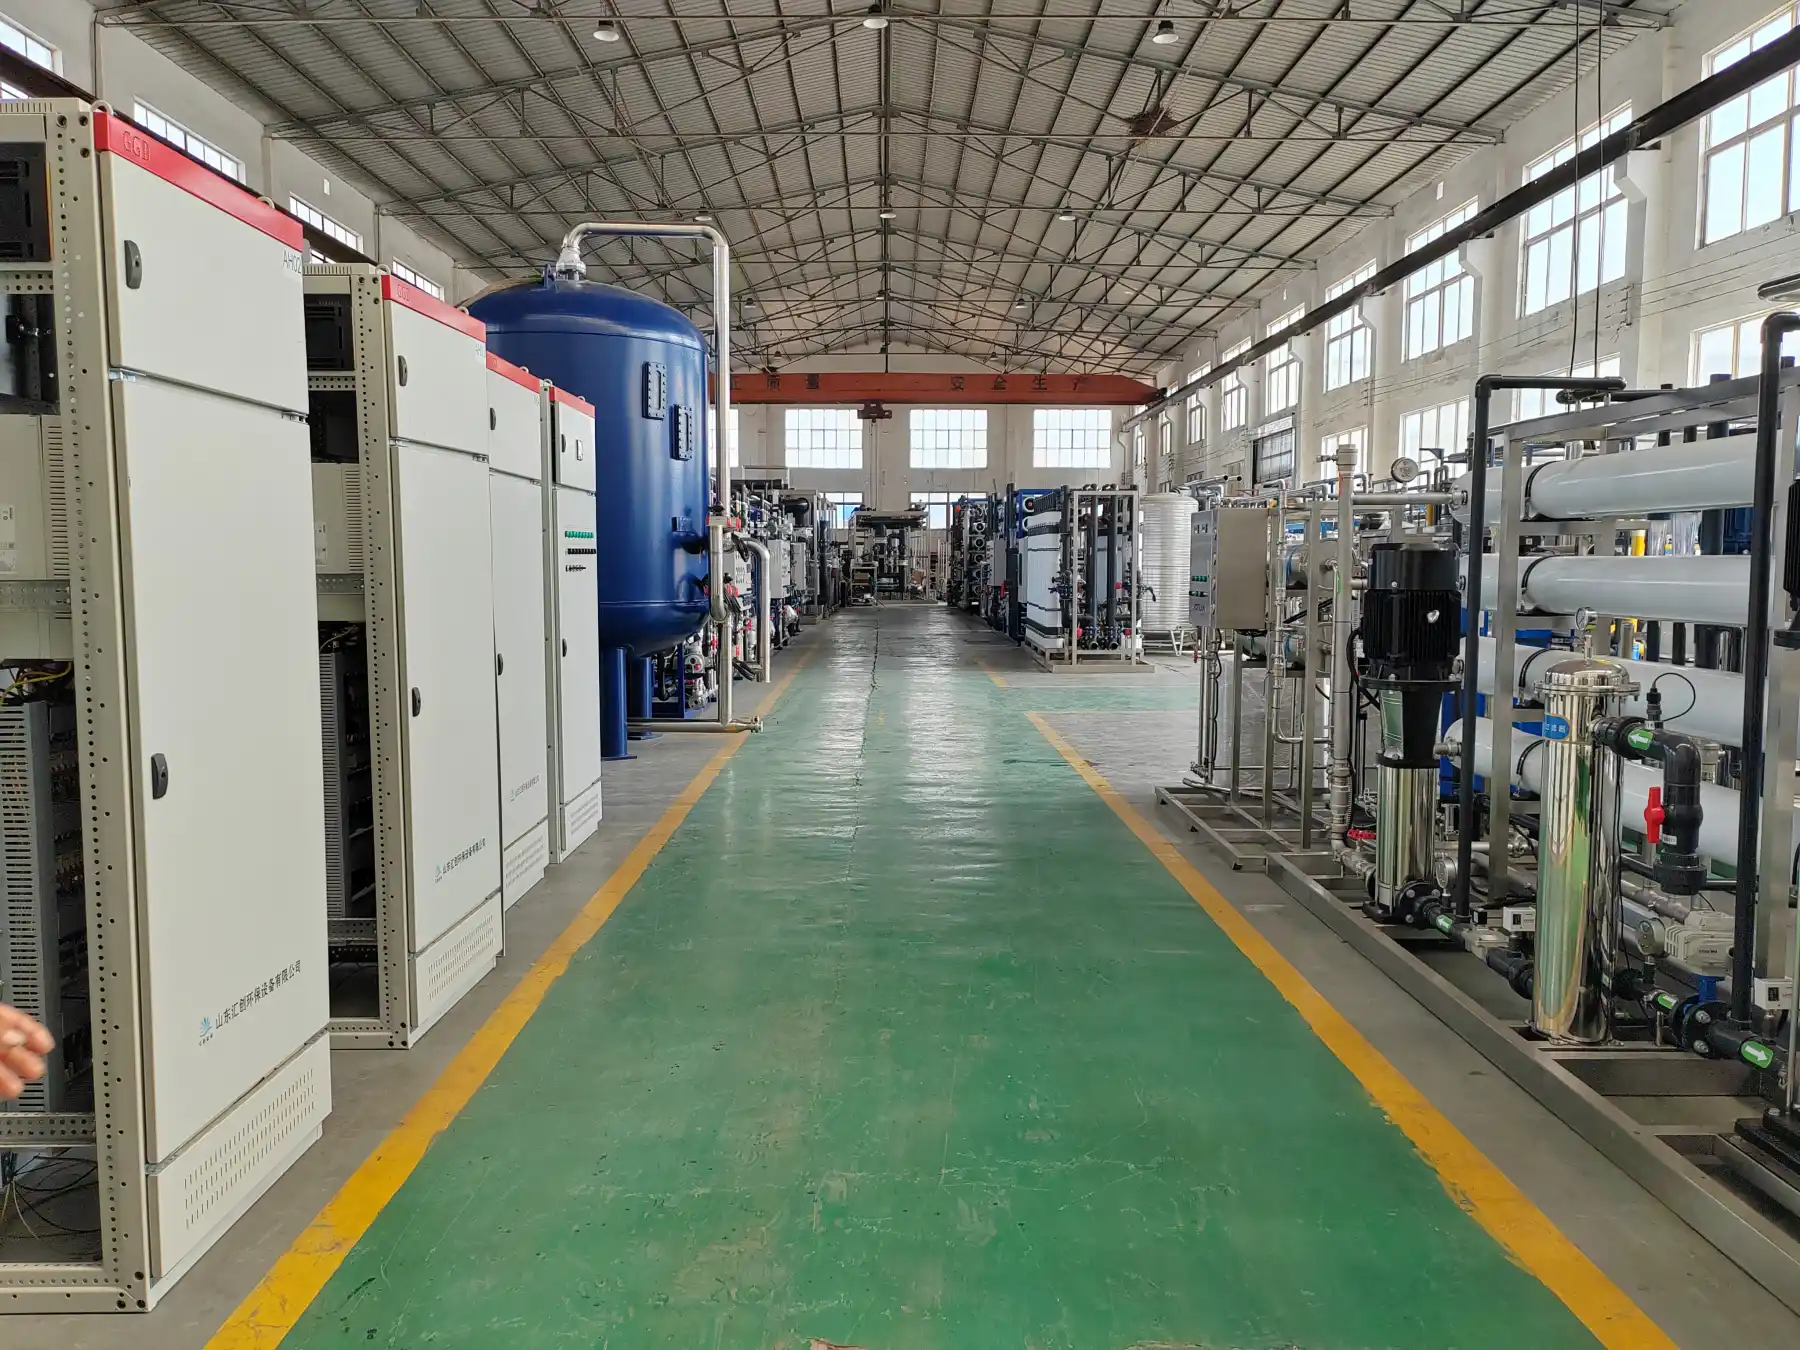
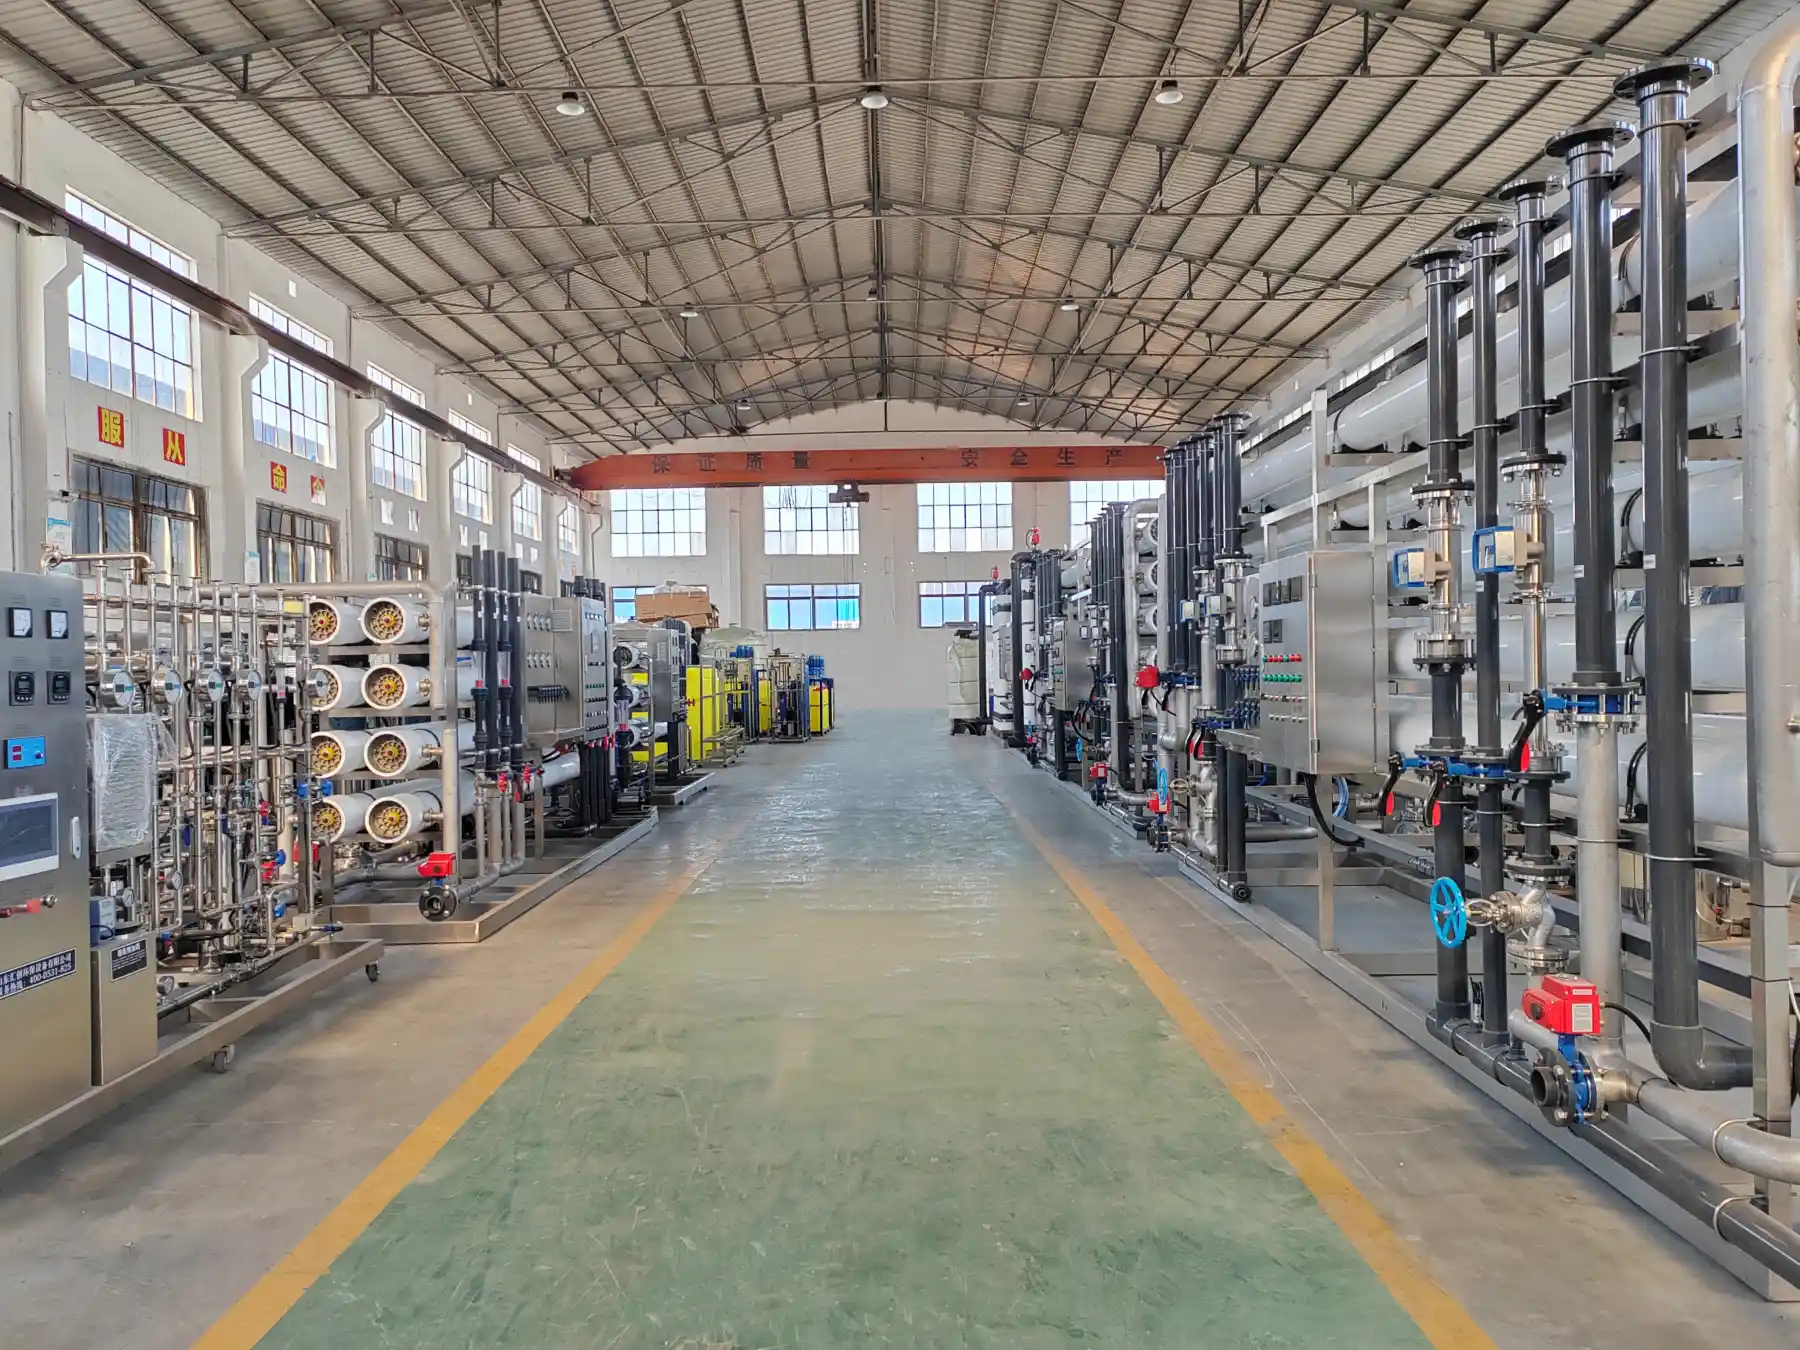
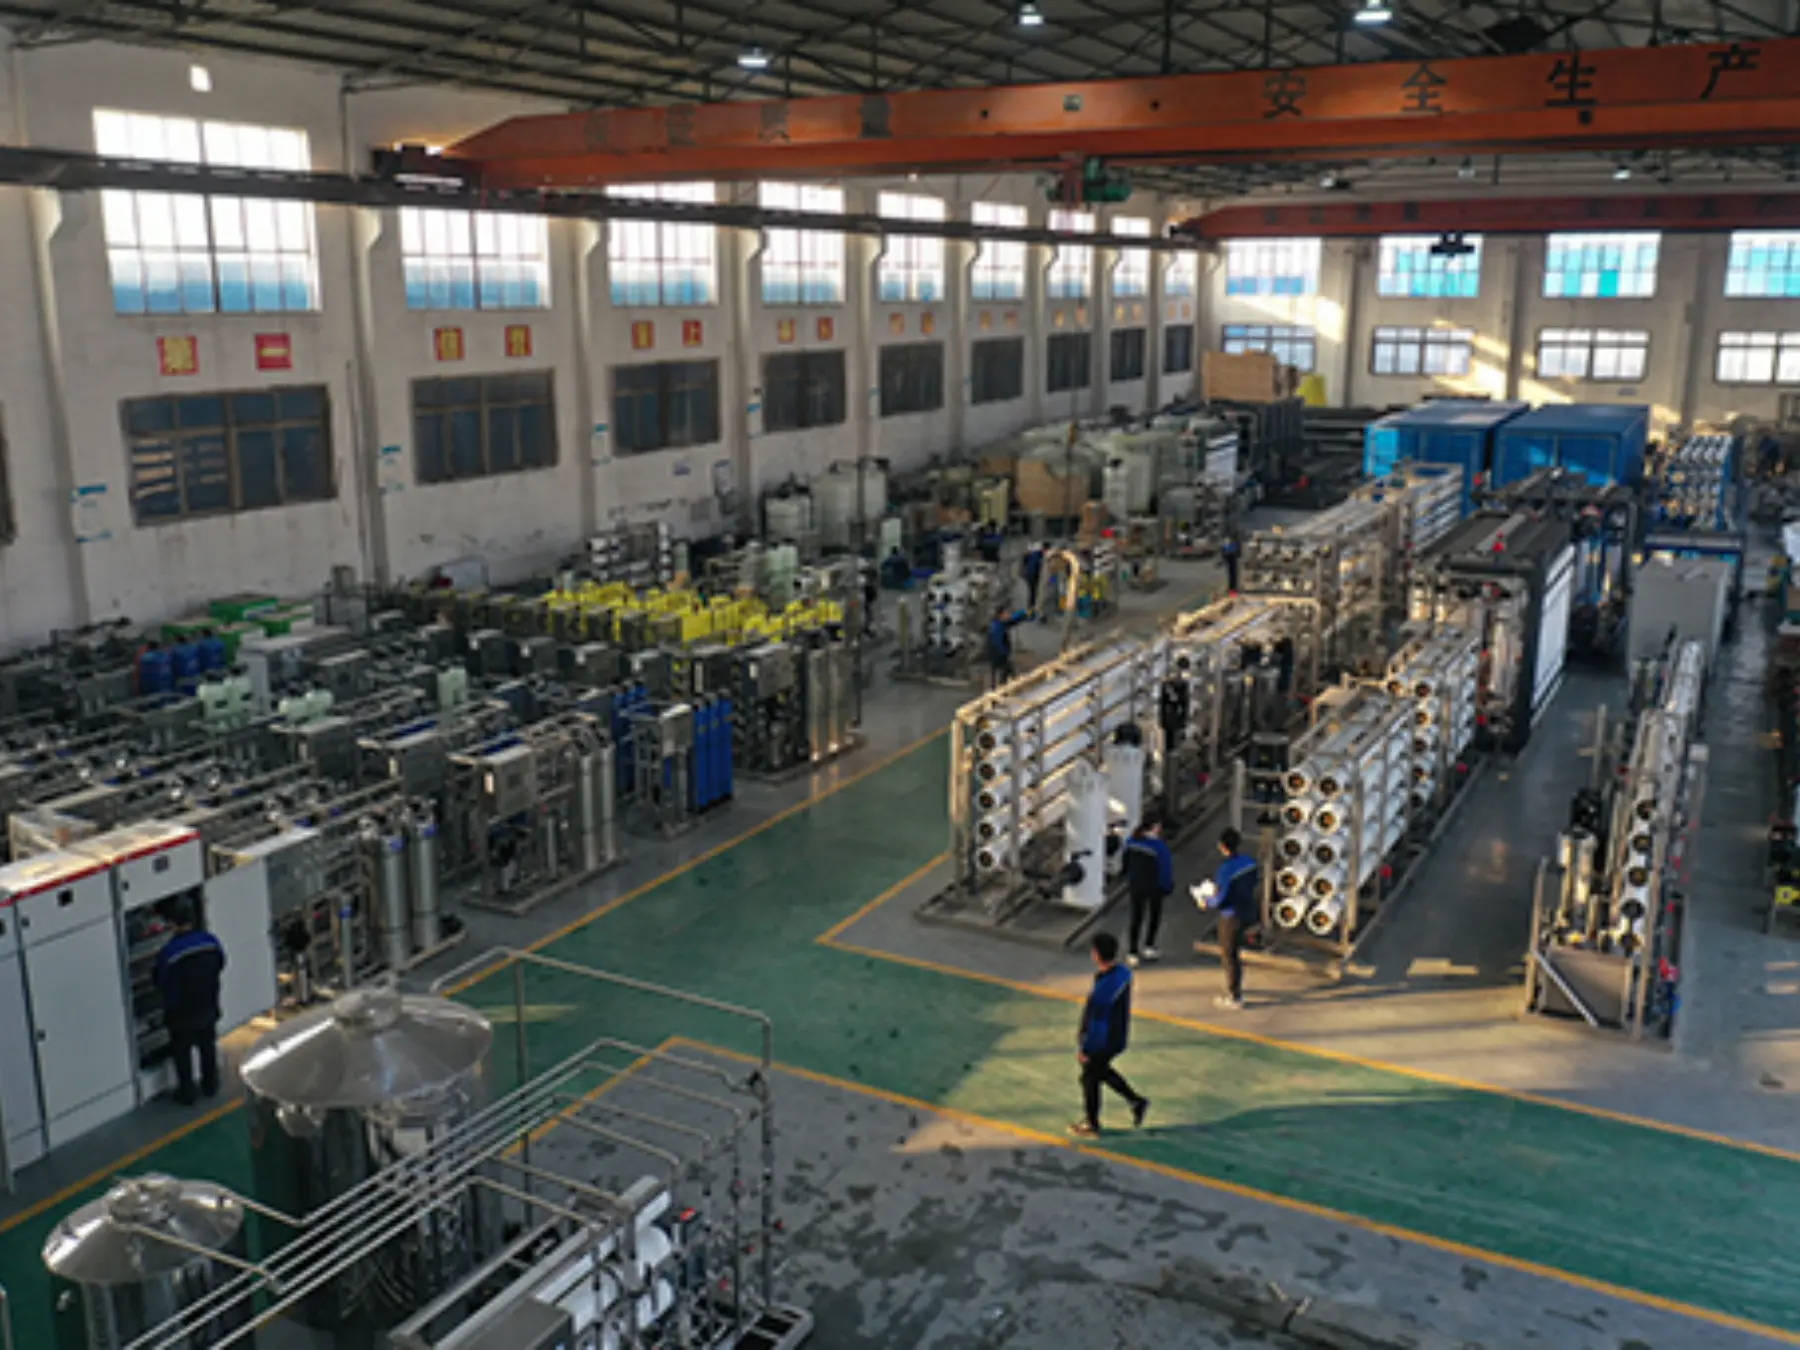
Partner with a Leading Chinese Source Factory: Supported by a 15,000 sqm workshop, 15 senior design engineers, and over 30,000 satisfied global clients, Shandong Huichuang offers premium OEM/ODM capabilities, non-standard layout designs, and direct B2B wholesale pricing. Contact our engineering team today to receive a free custom technical blueprint and competitive quotation for your water project!
Reviews
There are no reviews yet.