

Packaged & Integrated Industrial Wastewater Treatment Plant Overview
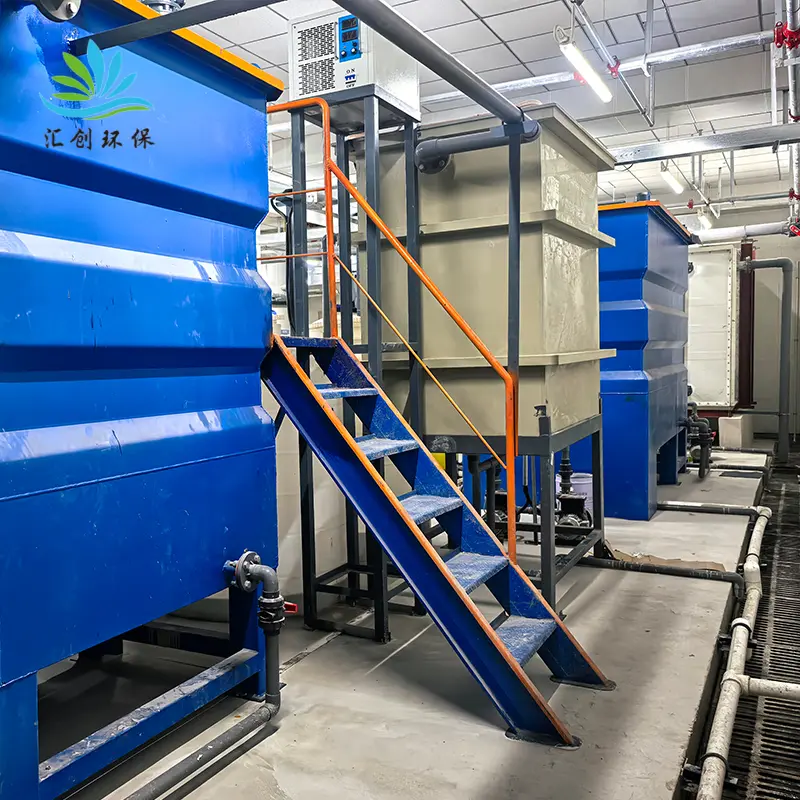
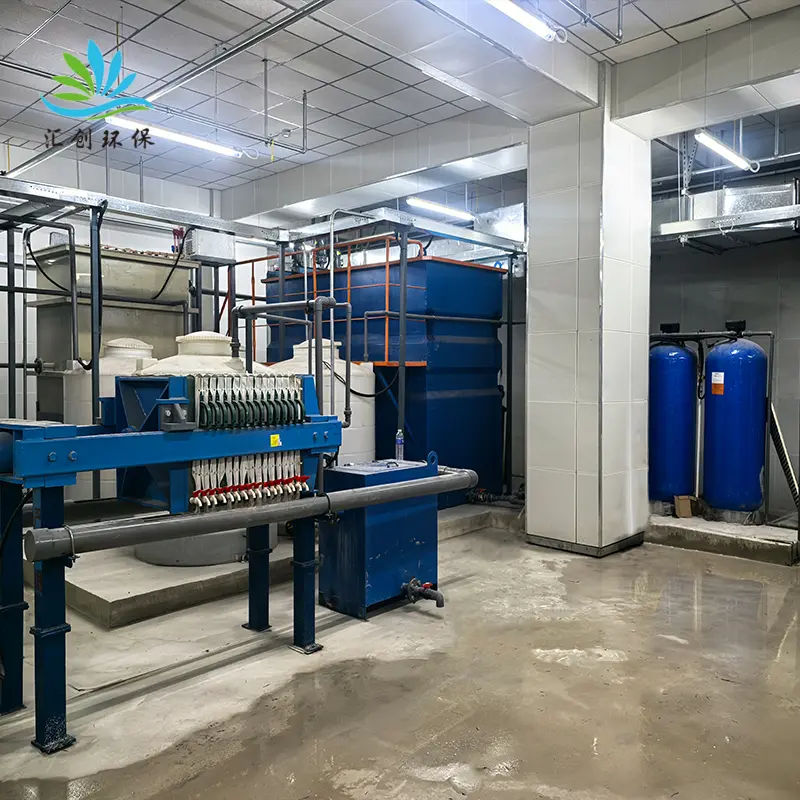
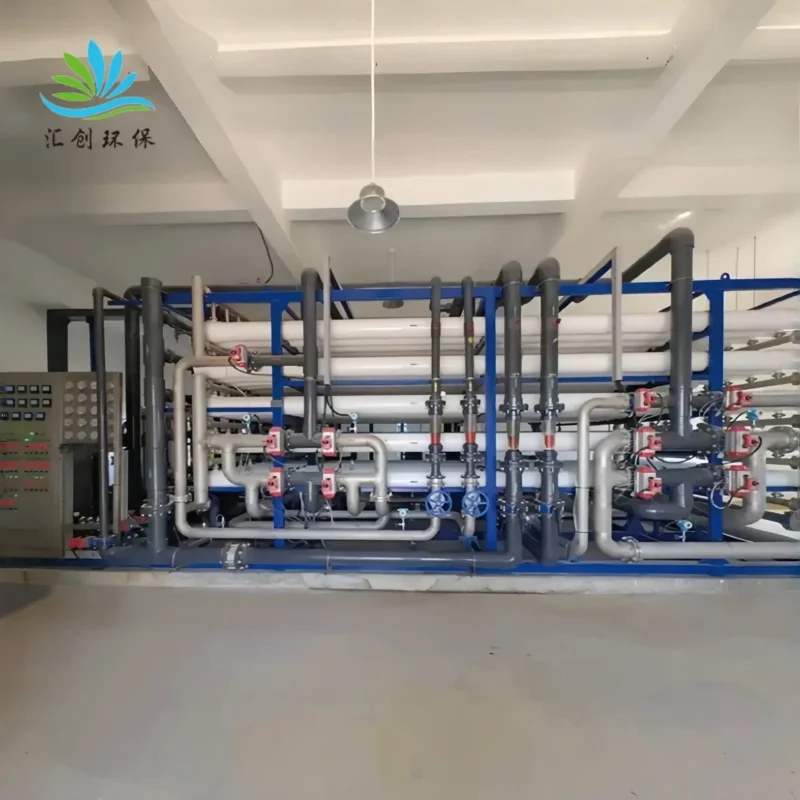
The Integrated Wastewater Treatment System designed and manufactured by Shandong Huichuang Environmental Protection Equipment Co., Ltd. is a highly mature, heavy-duty purification plant engineered for modern environmental compliance. Raw industrial manufacturing effluent and corporate domestic sewage often carry heavily fluctuating loads of organic matter, ammonia nitrogen, suspended solids, and chemical oxygen demand (COD). If left untreated, discharging this water triggers severe environmental damage and catastrophic regulatory fines.
Our turnkey packaged wastewater treatment skids are specifically built to solve these commercial compliance crises. By replacing massive, expensive traditional concrete basins with high-strength, compact modular steel tanks, this system delivers an absolute barrier against industrial pollution. It easily handles variable water volume shocks, turning toxic influent into clean, compliant water that strictly adheres to the GB8978-1996 Class 1A standard for direct environmental discharge or on-site water recycling.
Technical Specifications & Engineering Parameters
To assist global B2B procurement managers, municipal contractors, and EPC engineering firms in matching their project parameters, here are the certified specifications of our standard integrated wastewater purification series:
| Technical Feature Item | Industrial Specification Details |
|---|---|
| Core Biological Process | AOO Technology (Anaerobic → Anoxic → Oxic Process) |
| Advanced Deep Filtration | High-Flux MBR (Membrane Bioreactor) or Industrial UF Modules |
| Target Effluent Standard | Class 1A Quality Level (GB8978-1996 Comprehensive Code) |
| Applicable Influent Types | Domestic Sewage, Pharmaceutical Wastewater, Chemical Effluent, Food Processing Waste |
| Control Automation | Fully Automated PLC Center (Smart Automated Aeration & Sludge Discharge) |
| Structural Shell Profile | Corrosion-Resistant Reinforced Carbon Steel Box / Custom Layout |
| Operation Features | Low Noise, Strong Hydraulic Shock Resistance, Unattended Smart Operation |
Scientific Multi-Stage Treatment Roadmap
To secure flawless effluent clarity even during massive peak-load fluctuations, our wastewater plant utilizes an exceptionally reliable, sequential process flow:
- Stage 1: Mechanical Pretreatment & Bar Screening: The raw influent passes through a high-efficiency bar screen and balancing equalization tank to physically trap suspended debris, hair, lint, mud, and free oil slicks, ensuring the safety of down-line pumps.
- Stage 2: Advanced Hydrolysis & Acidification (AOO Bio-Chemical): The water enters an anaerobic/anoxic environment where specialized bacterial colonies rapidly break down complex, refractory macromolecules, organic substances, ammonia nitrogen, and COD into simpler biodegradable elements.
- Stage 3: Aerobic Contact Oxidation: Under active automated aeration, robust aerobic micro-organisms quickly consume the dissolved organic pollution, oxidizing nitrides and thoroughly clarifying the fluid matrices.
- Stage 4: MBR/UF Secondary Clarification & Disinfection: The water undergoes a final deep filtration process through premium high-flux MBR membrane modules or UF separation arrays, stripping away all microscopic colloids, suspended particles, and sludge flocs. After final chlorination or UV disinfection, it emerges completely pure and odorless.
Why Choose Our Packaged Wastewater Treatment Plants?
- Turnkey Integrated Layout & Low Civil Costs: Unlike old-fashioned concrete wastewater plants that demand months of disruptive excavation and high civil construction fees, our steel-packaged system features a highly compact, space-saving footprint. It arrives fully pre-assembled, saving valuable property area and slashing installation time.
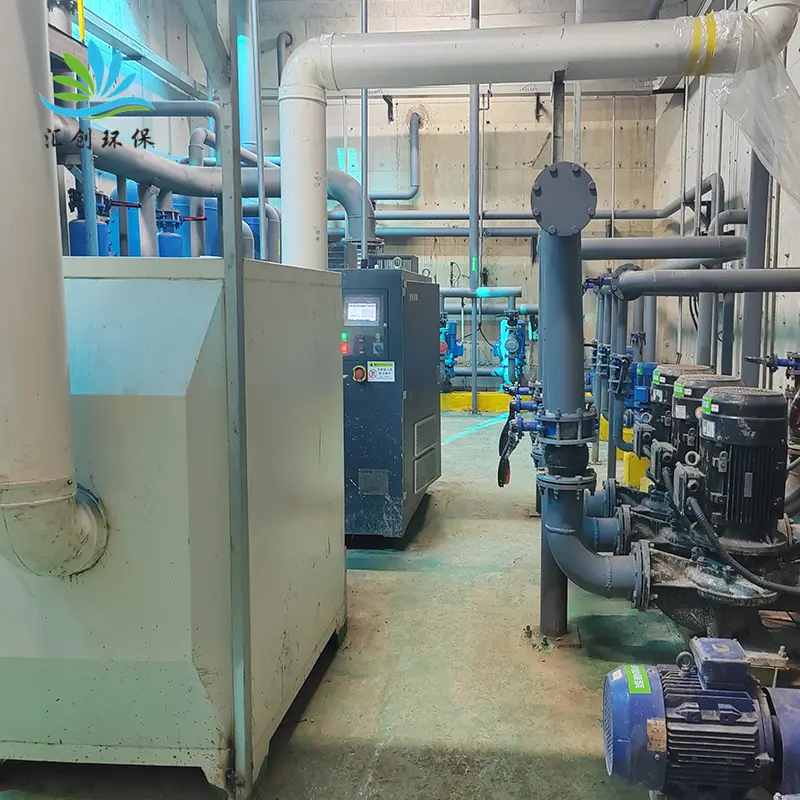
- Unattended 24/7 Automation via Smart PLC: The system features a centralized smart electrical control cabinet that monitors all operation loops. It automatically handles timed aeration cycles, water intake, and automated sludge recycling, allowing the entire plant to operate safely all day without full-time on-site operators.
- Superb Shock Load Resistance & Durability: Engineered with a highly resilient biomass buffer framework, the plant easily handles sudden chemical fluctuations or volume spikes without suffering biomass failure. The heavy-walled carbon steel shell is treated with high-grade anti-corrosion coatings to deliver a long, stable operational lifespan.
- 100% Green Recycling & Eco-Friendly Reuse: The high-quality treated water can be discharged directly into nature without risking fines, or instantly routed for recycling uses like landscape greening, on-site floor washing, or cooling loop makeup—saving your business immense water utility costs.
B2B Target Applications & Fields
- Industrial Manufacturing Complexes: Complete on-site treatment and purification for pharmaceutical factories, chemical compounding plants, and food & beverage processing hubs.
- Commercial Facilities & Tourism: Decentralized water treatment for luxury hotels, remote holiday resorts, large construction worksites, and high-density shopping plazas.
- Municipal & Residential Networks: Turnkey sewage treatment systems for residential housing communities, remote rural villages, and municipal towns without public sewer access.
Frequently Asked Questions (FAQ)
Can this integrated wastewater system be installed completely underground?
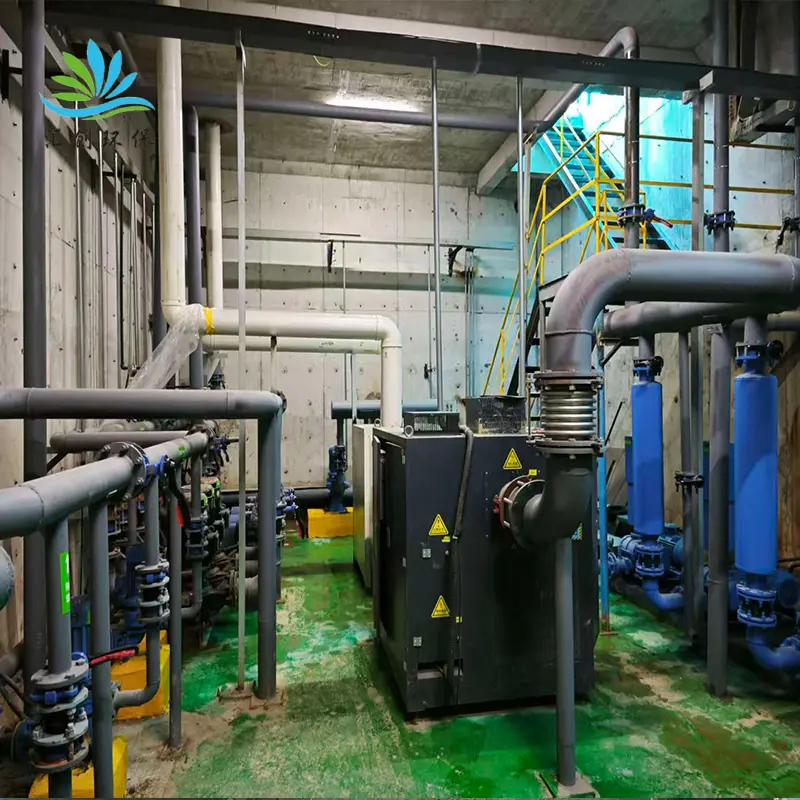
Yes, absolutely. Our packaged systems are highly versatile and can be installed above ground on a simple concrete slab, or buried completely underground with a lawn overlay. The underground installation is an excellent option for hotels and resorts, as it effectively preserves landscape aesthetics while isolating mechanical noise and keeping the utility area out of sight.
What routine maintenance is required for the MBR membrane modules?
Thanks to our integrated automated PLC backwashing and smart forward-flushing programs, the MBR modules resist biological fouling extraordinarily well. The system automatically executes short hydraulic flushes during daily operation, leaving manual or chemical cleaning (CIP) requirements down to only once or twice a year under standard domestic loading parameters.
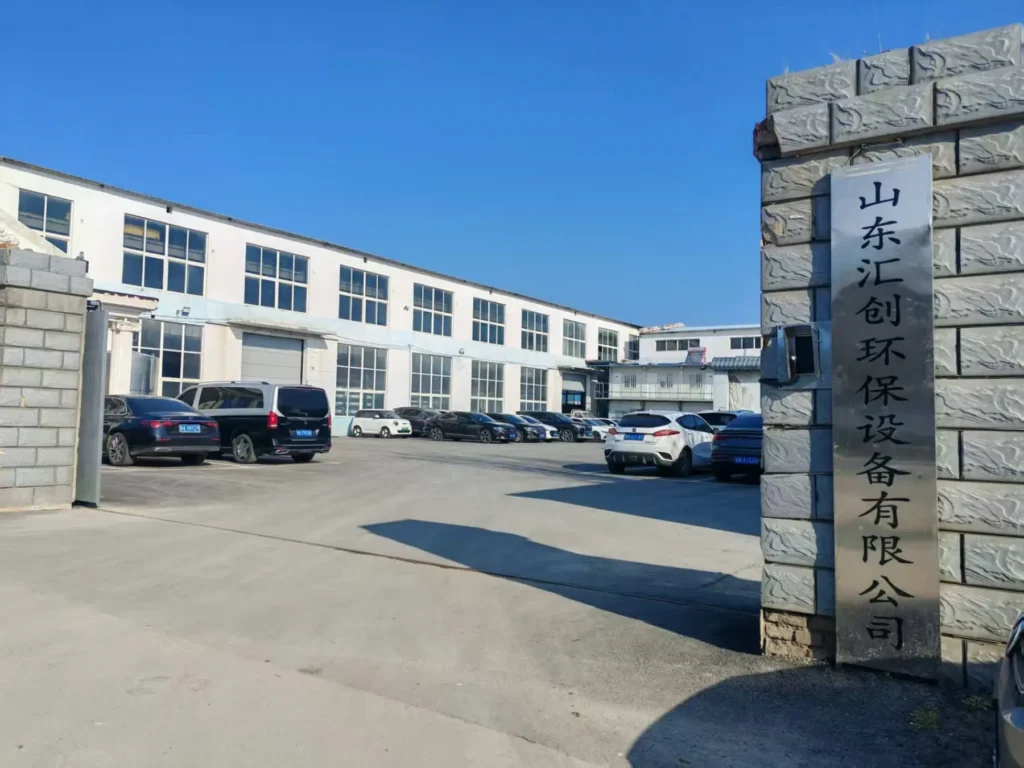
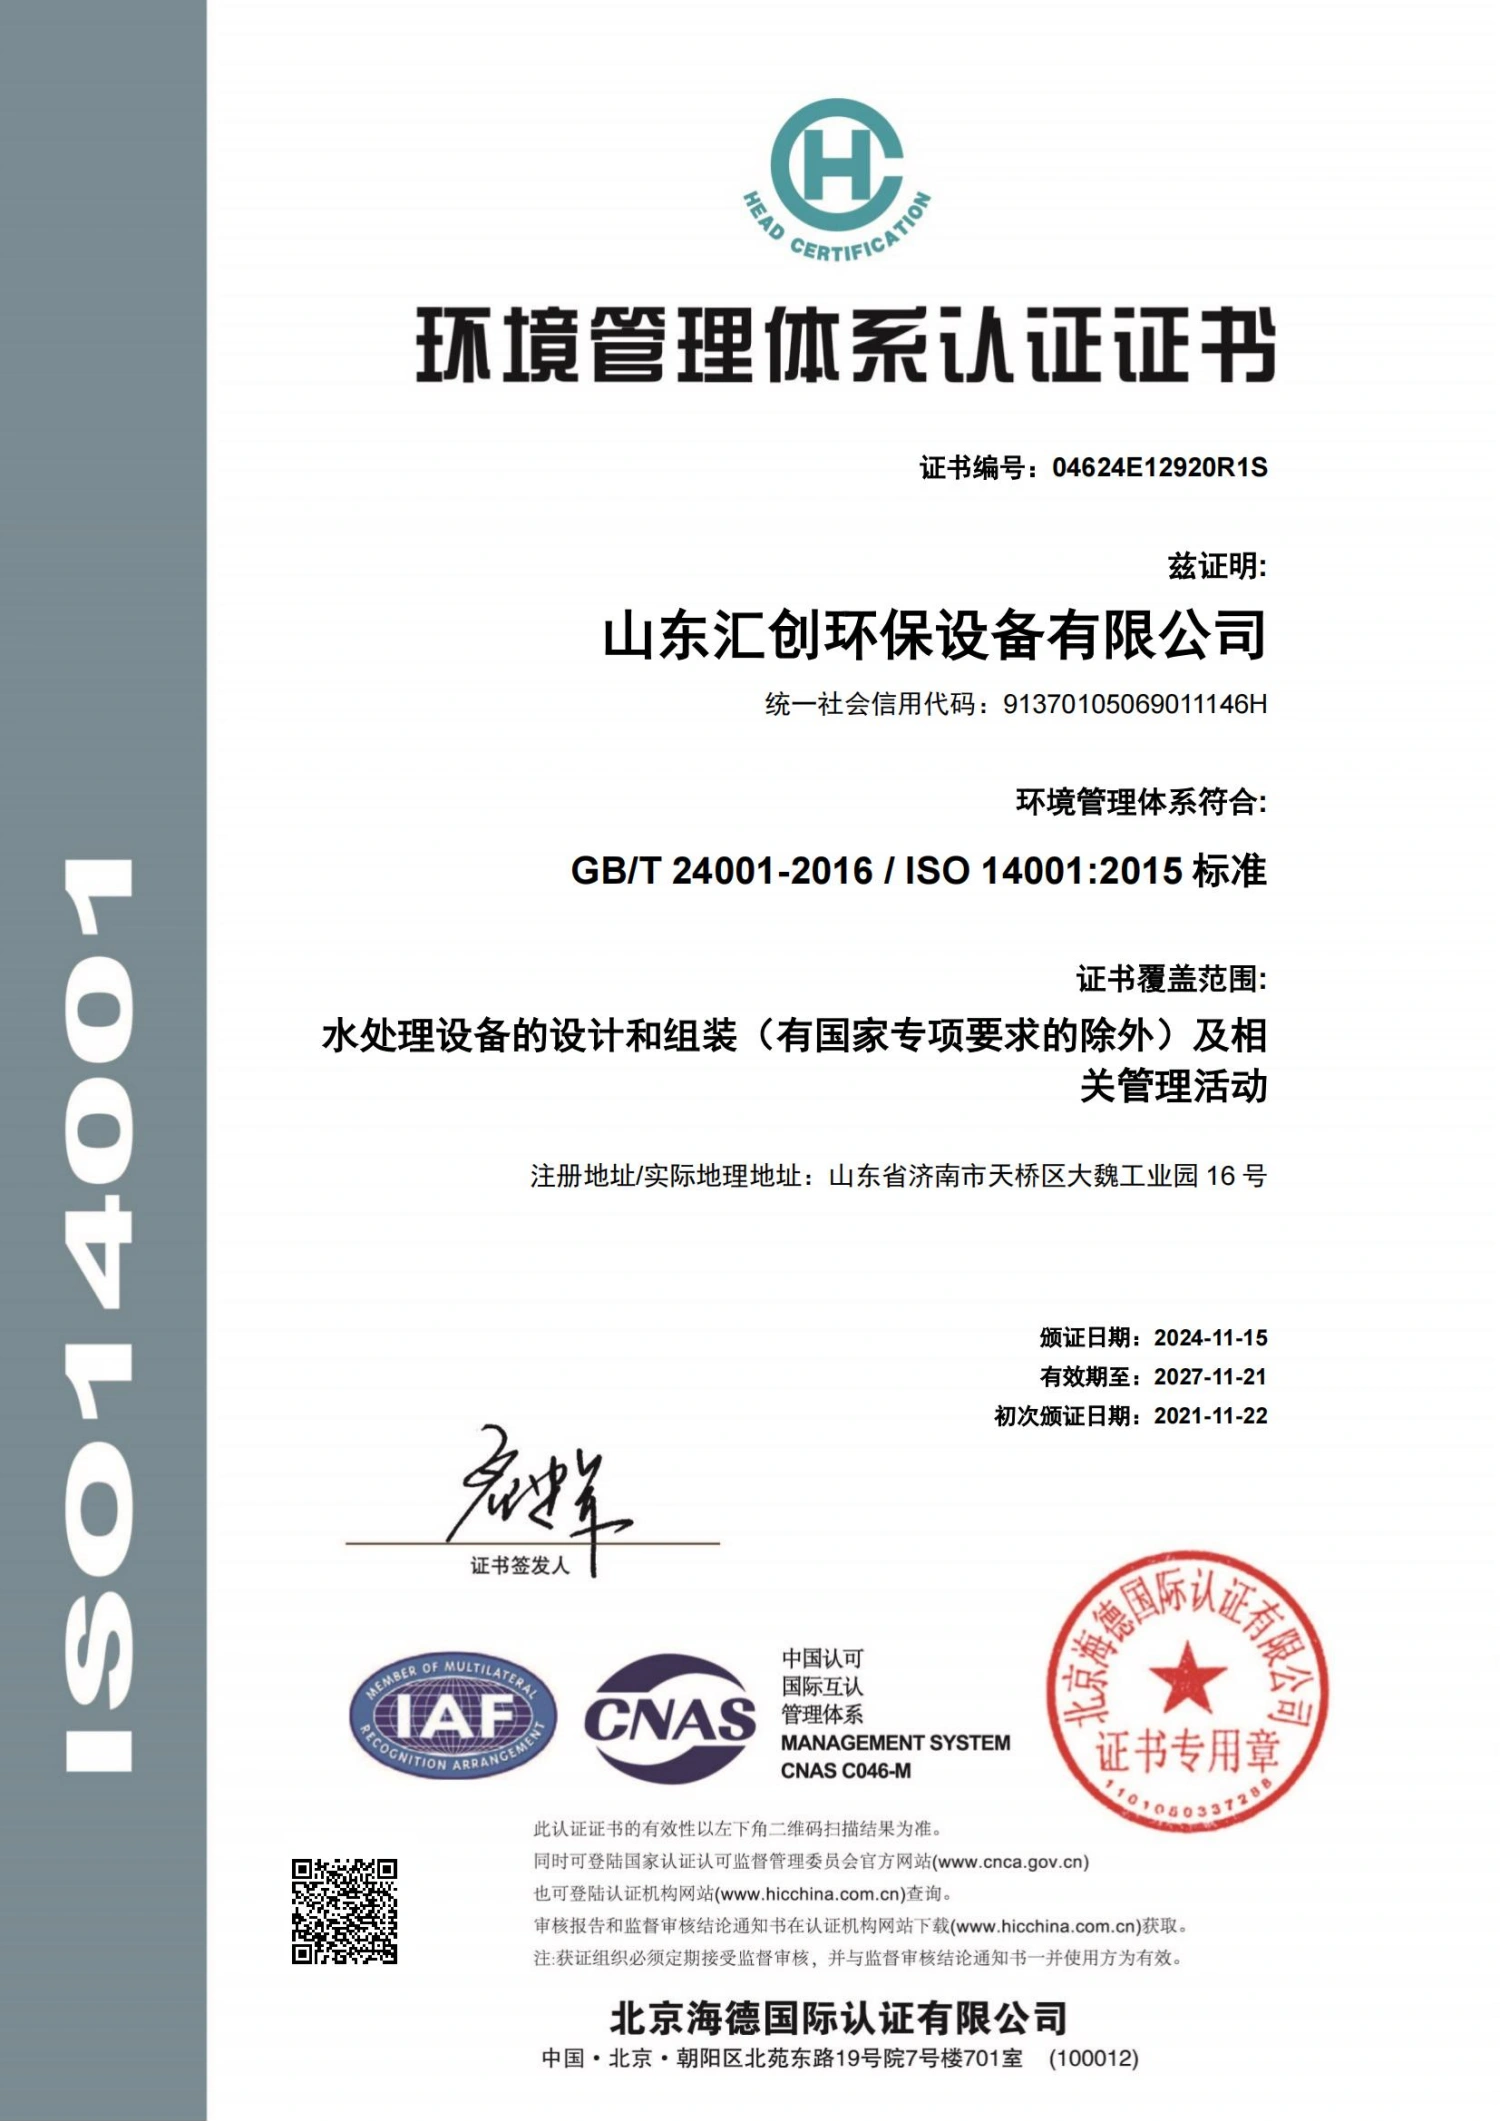
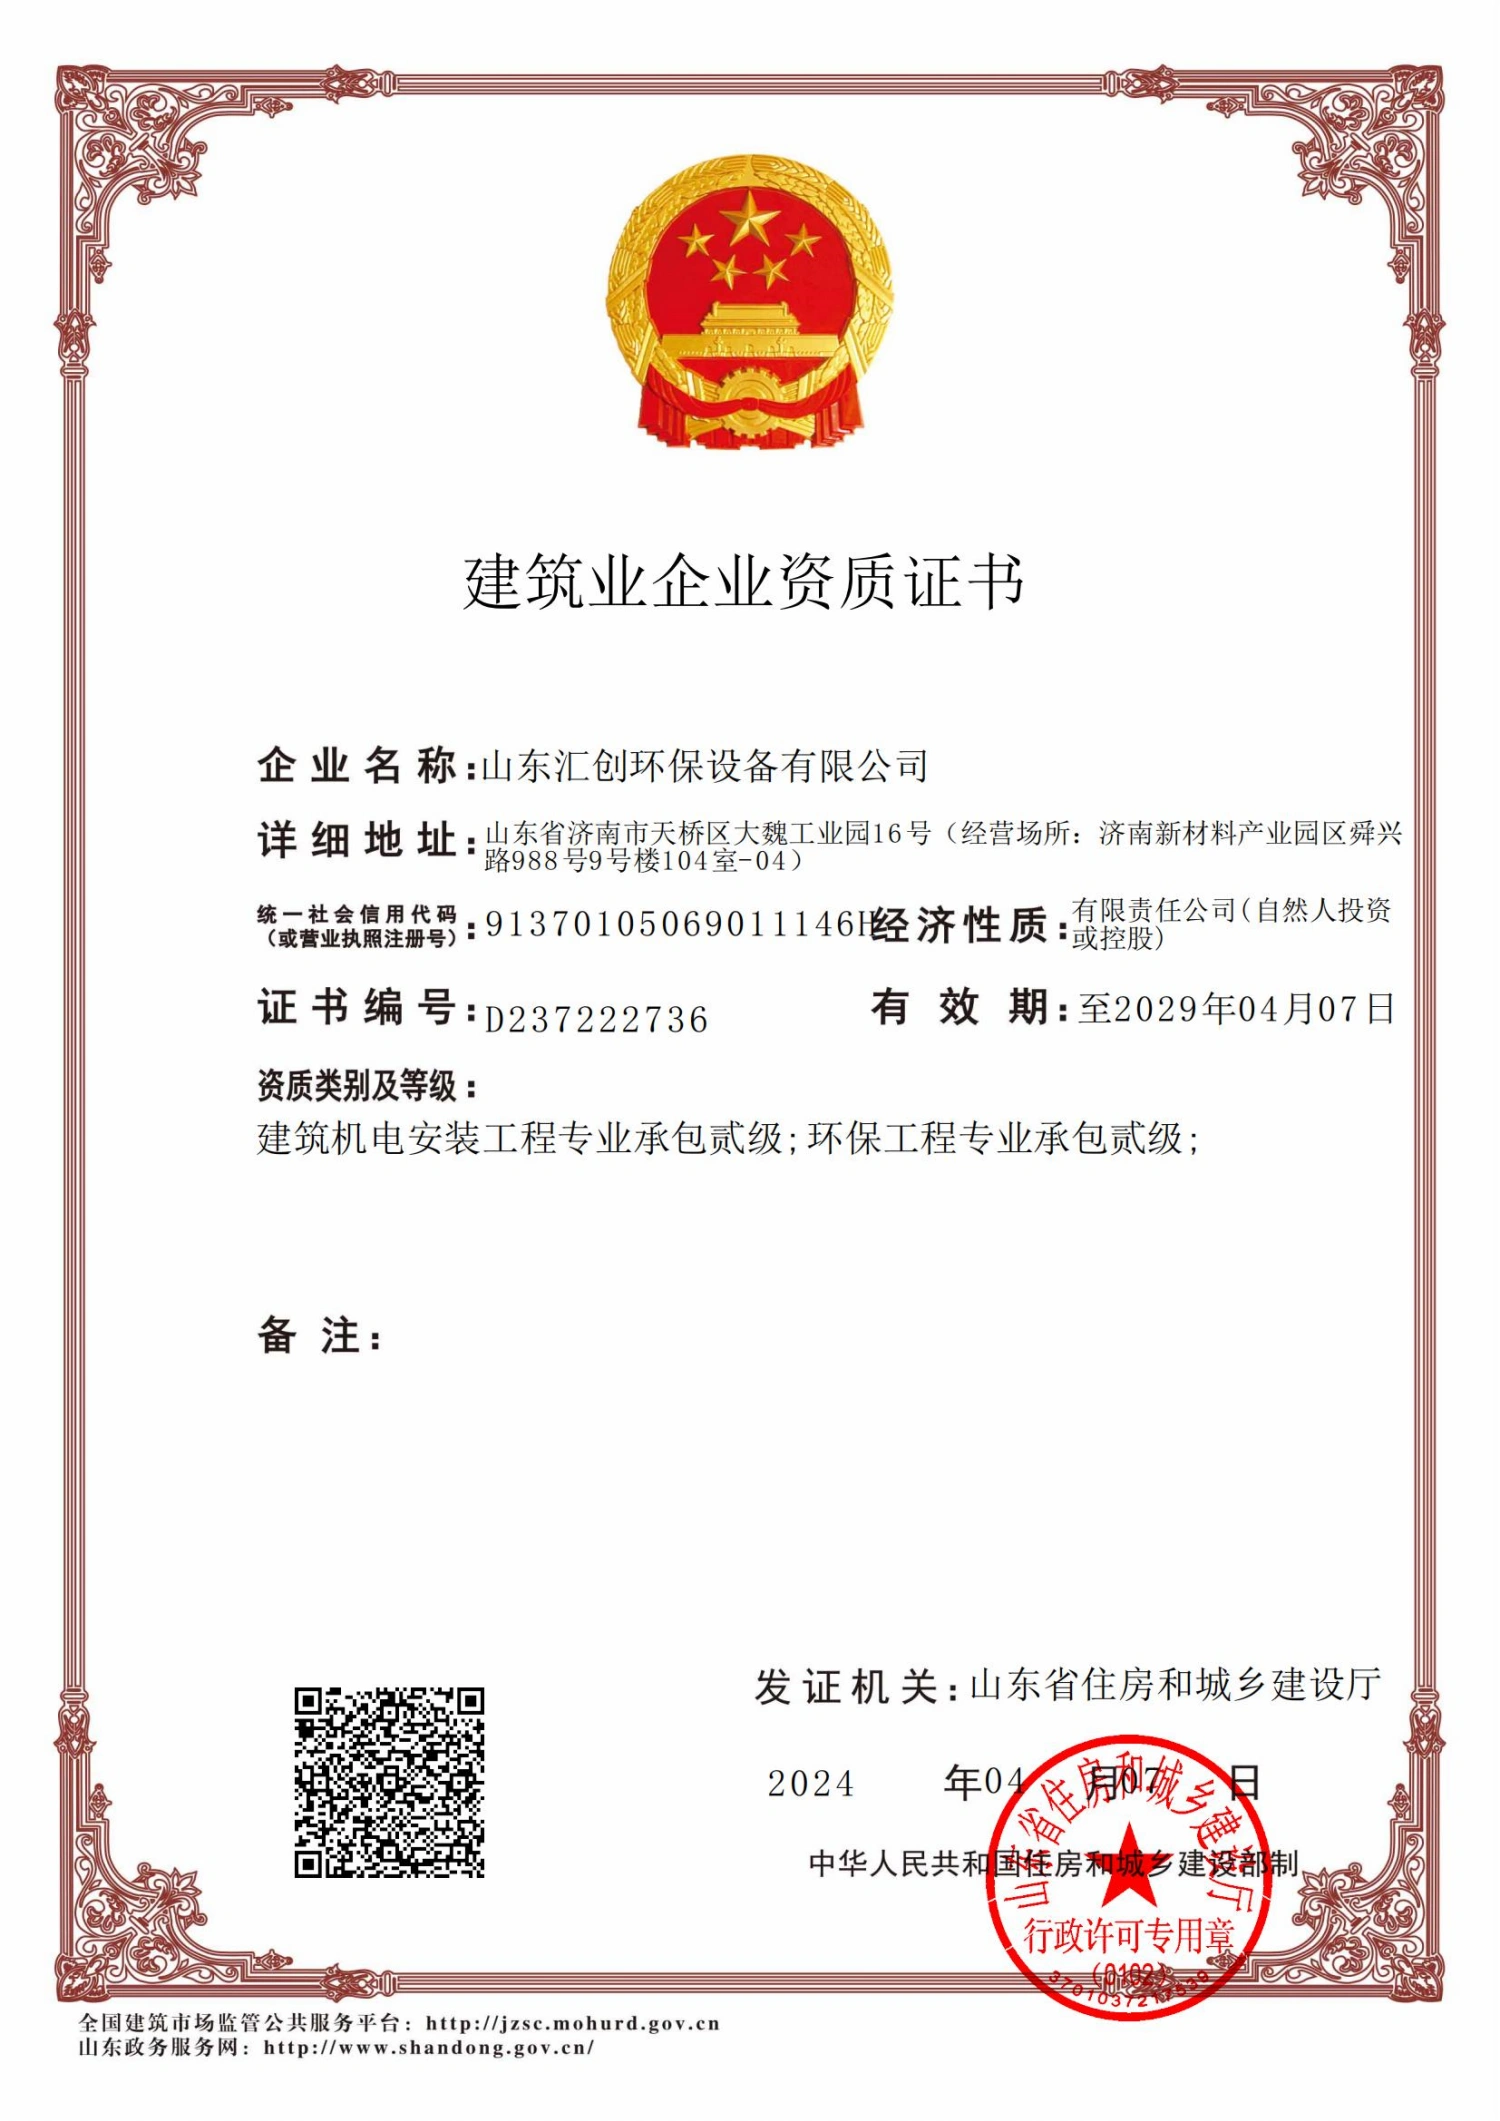
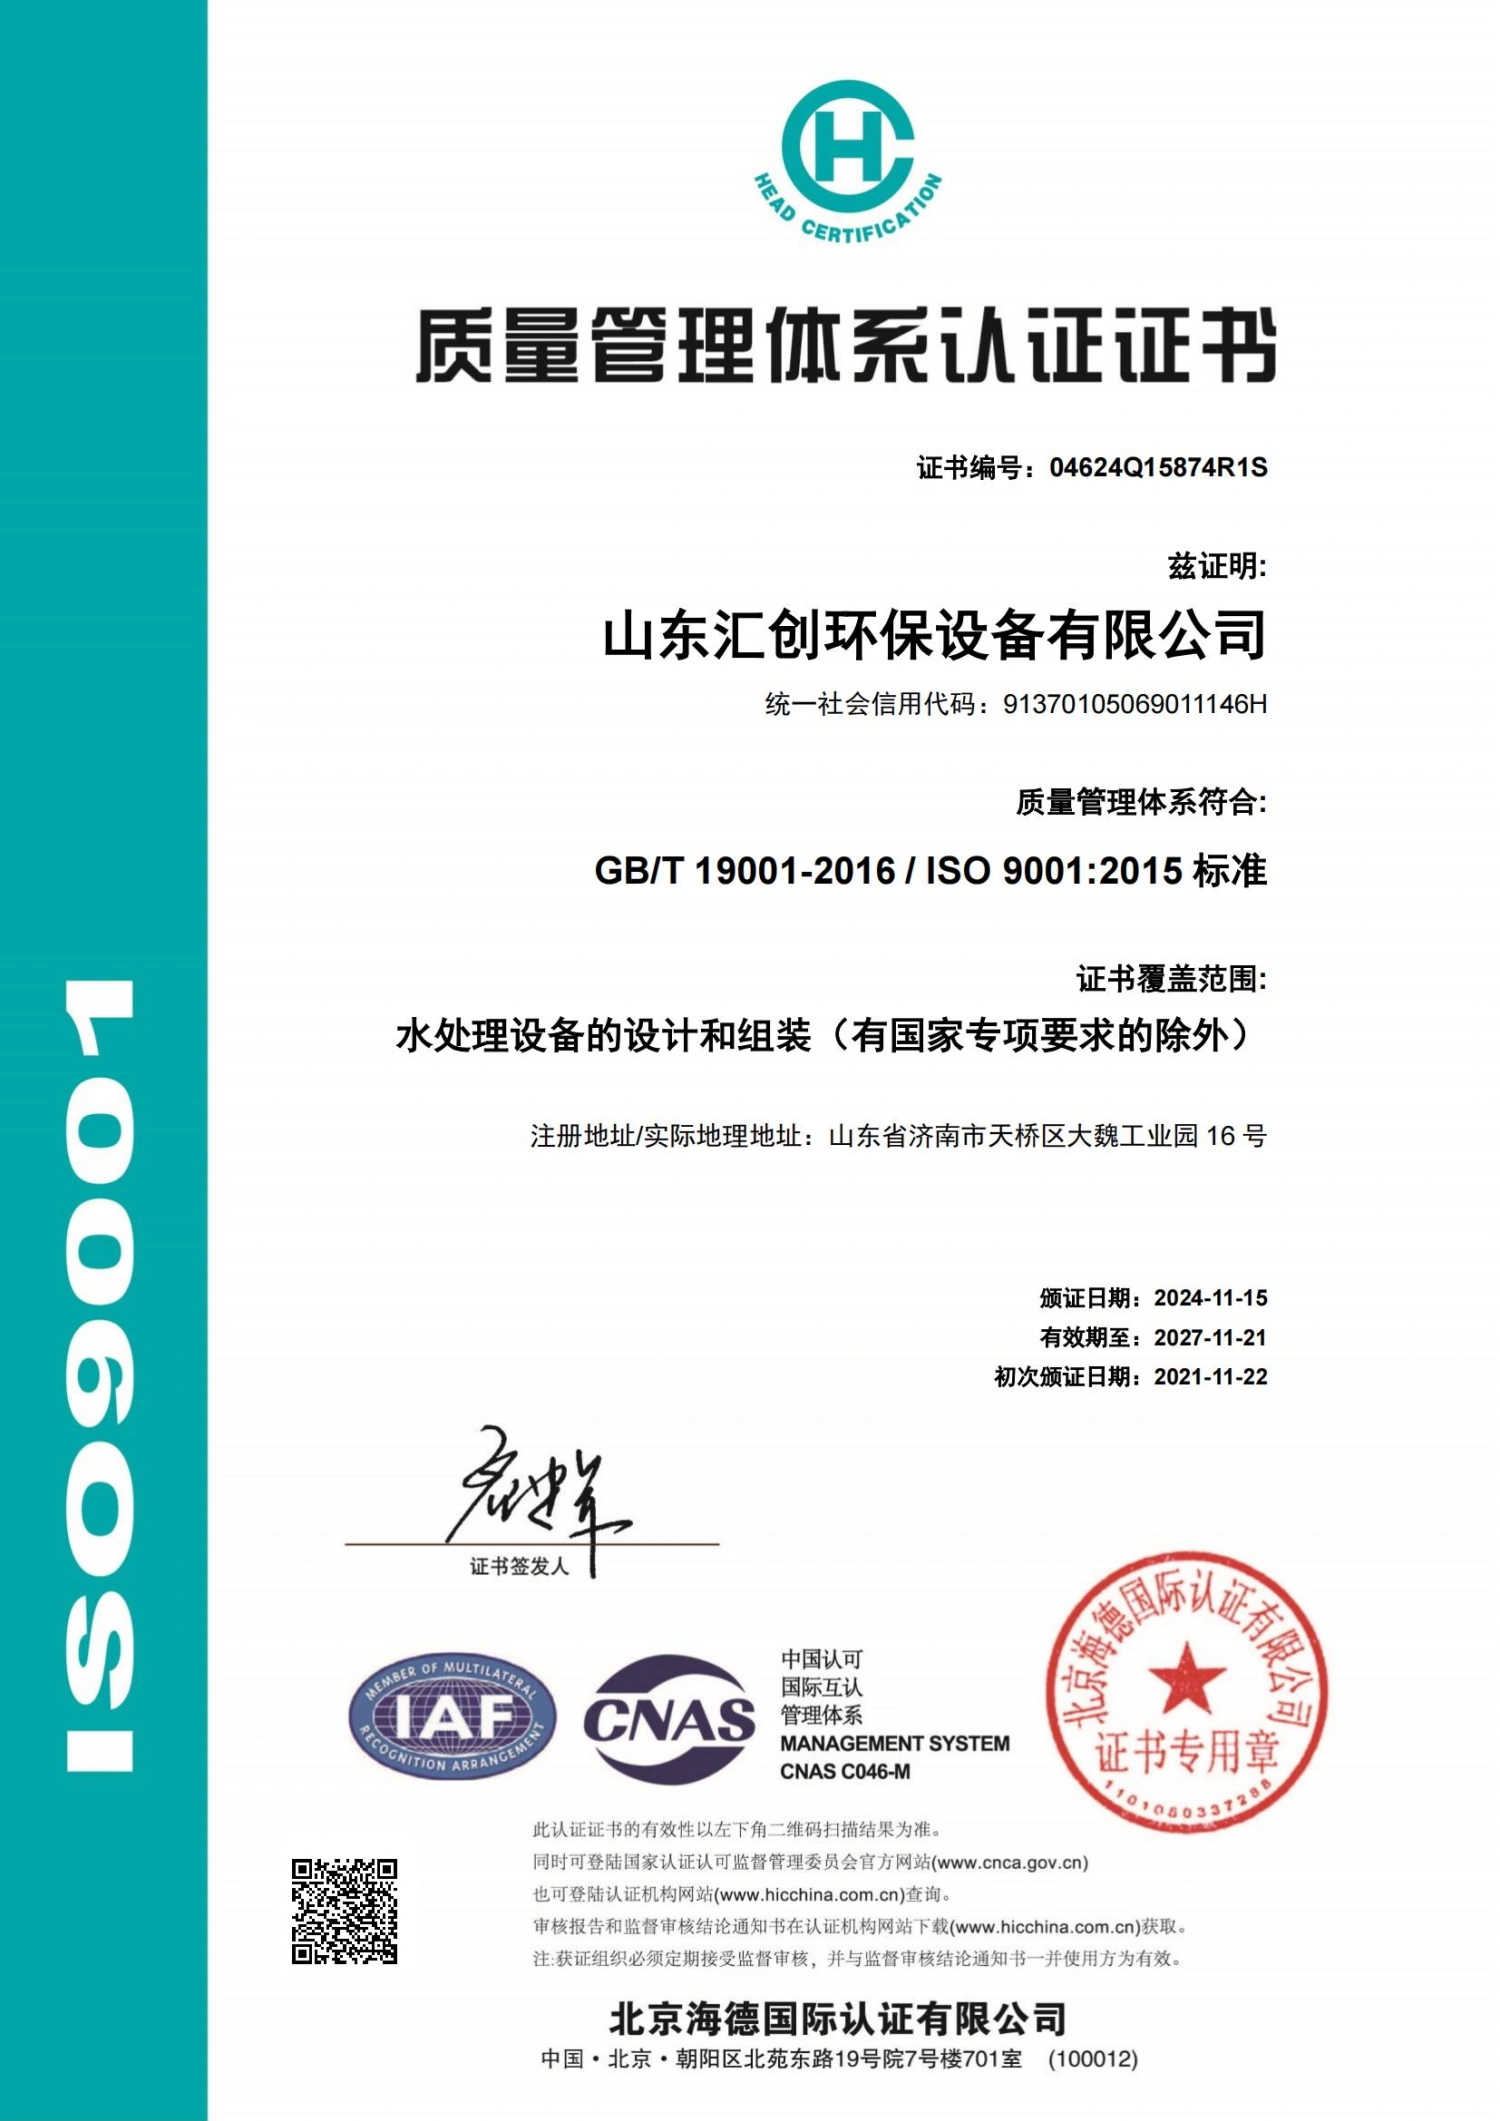
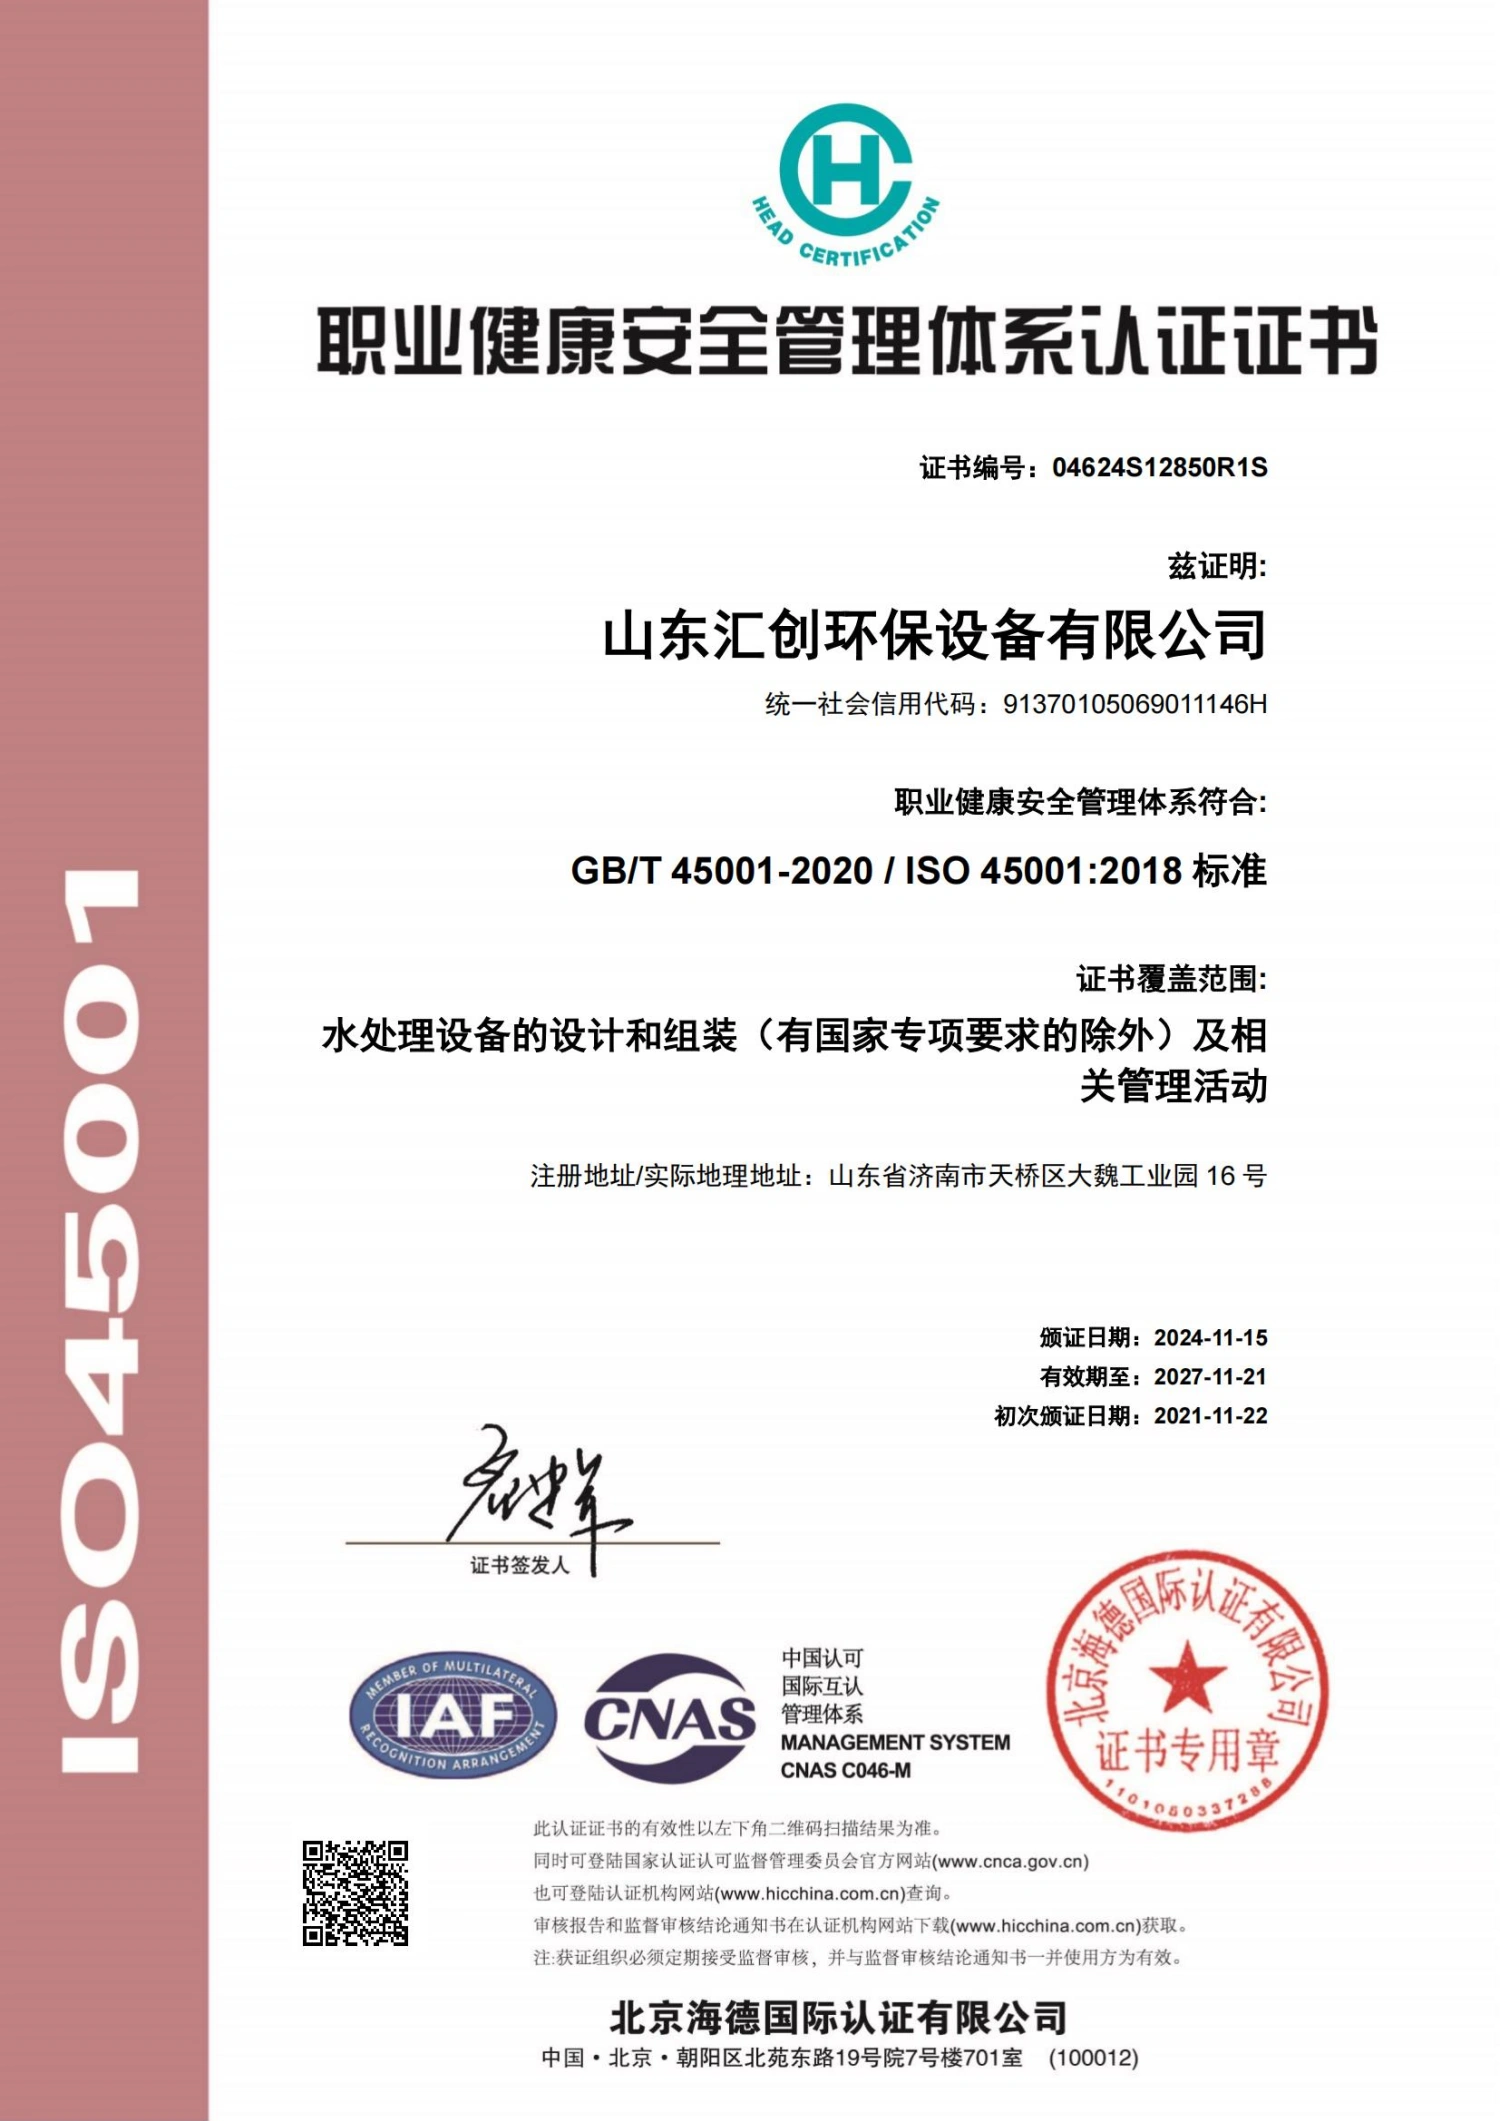
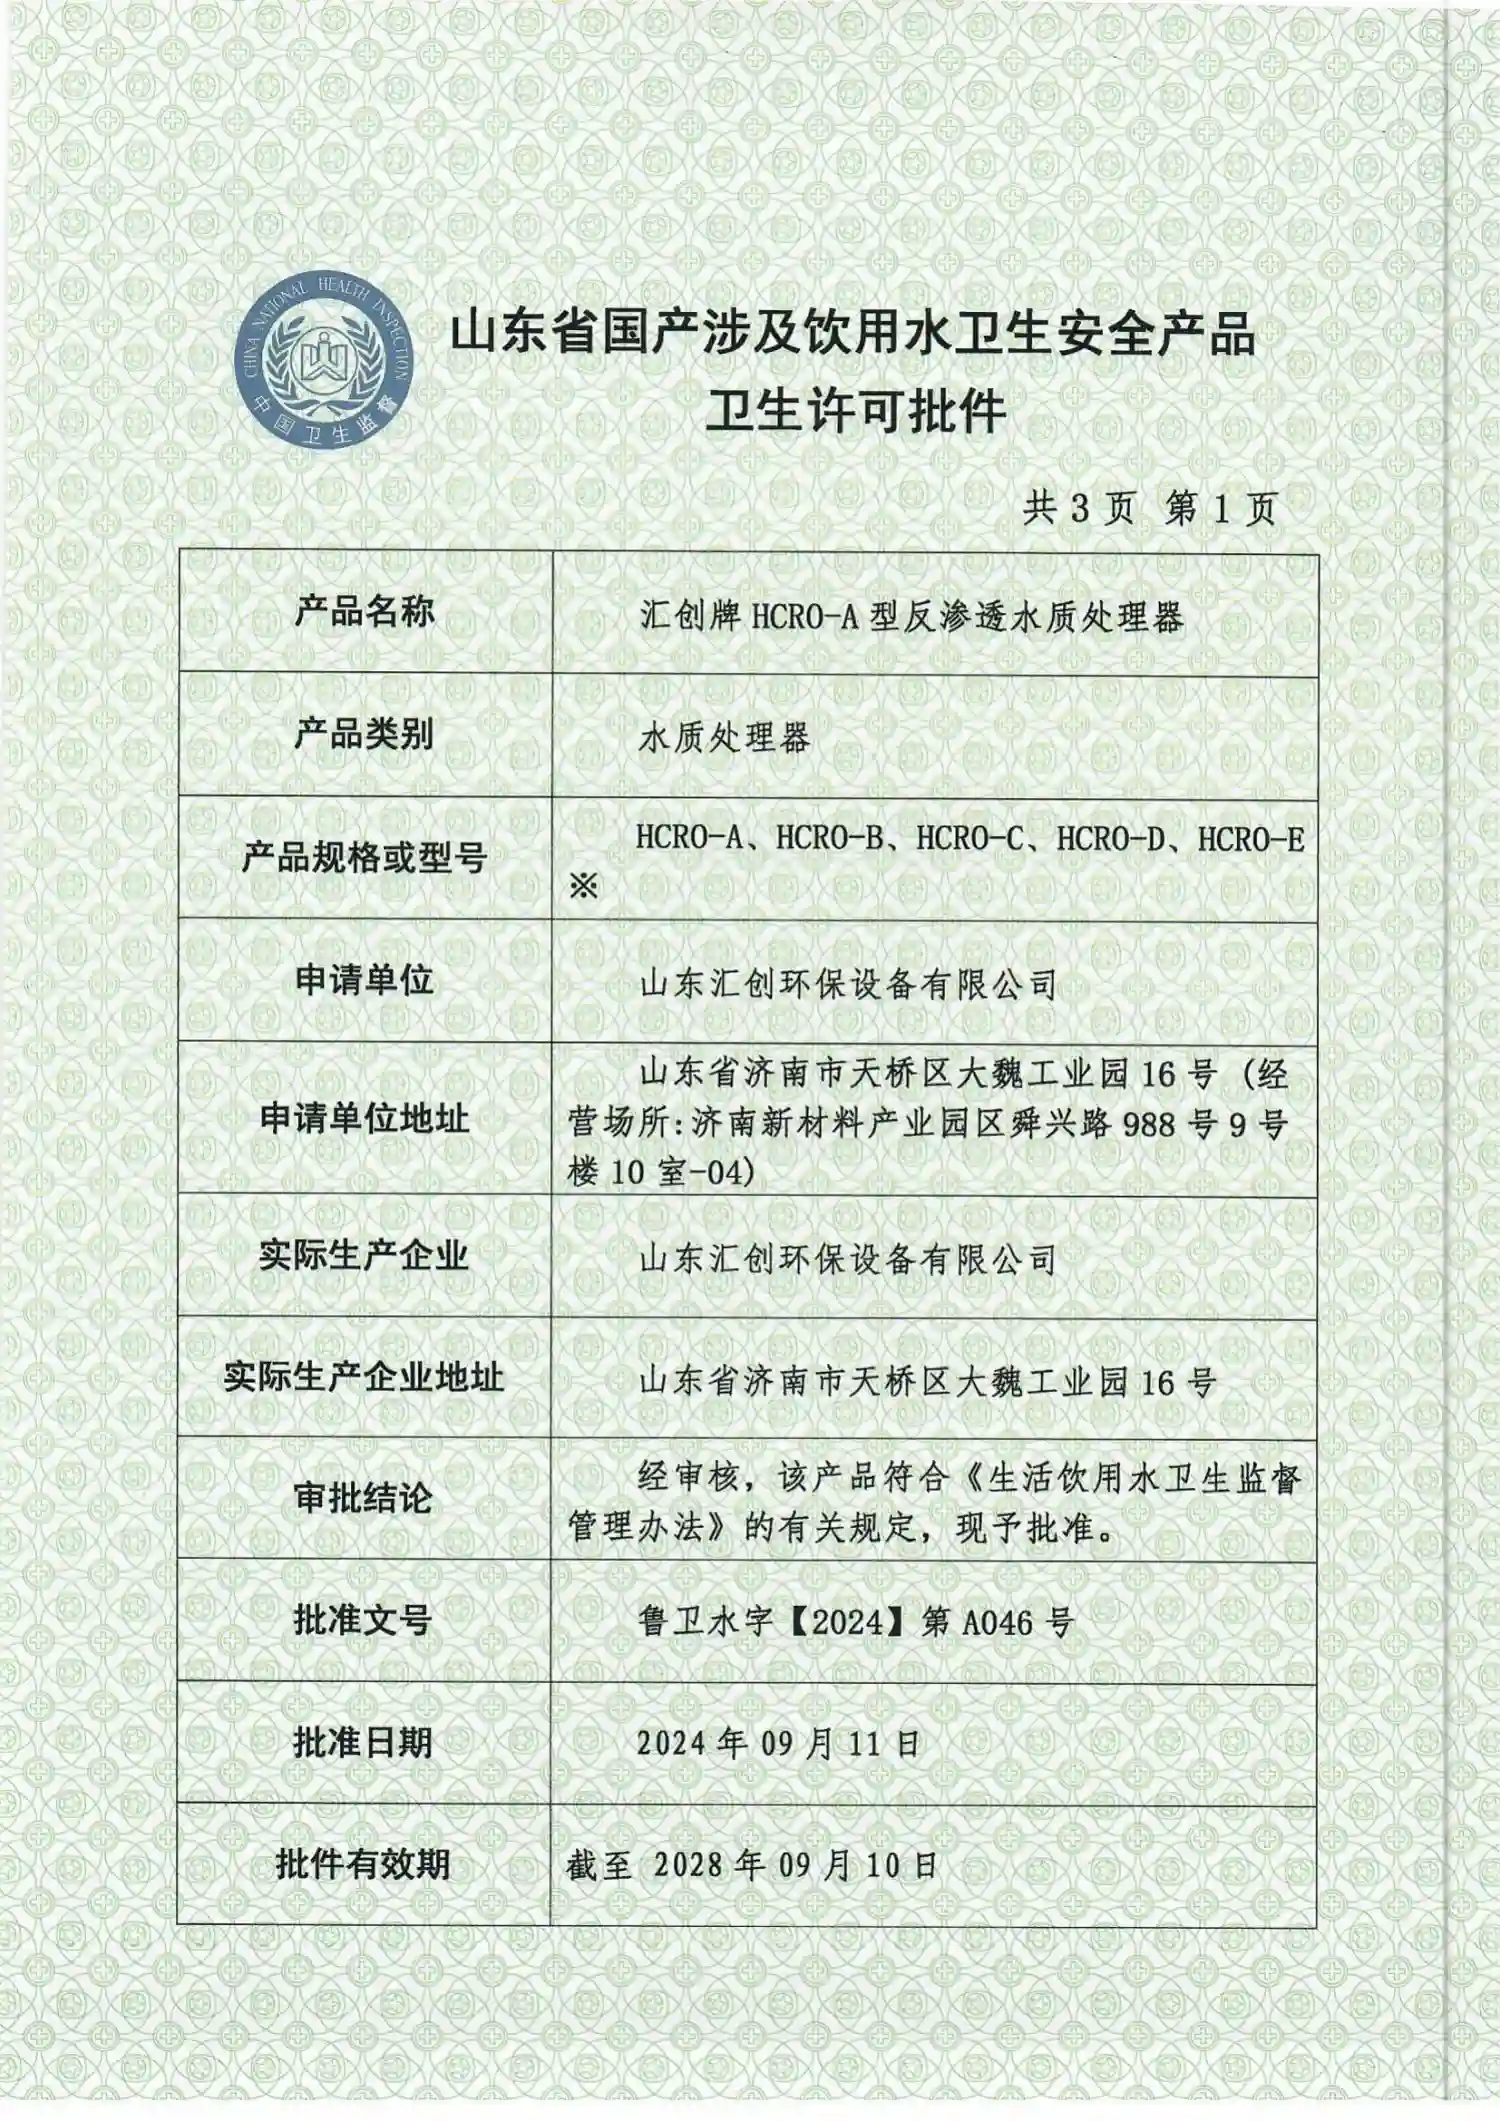
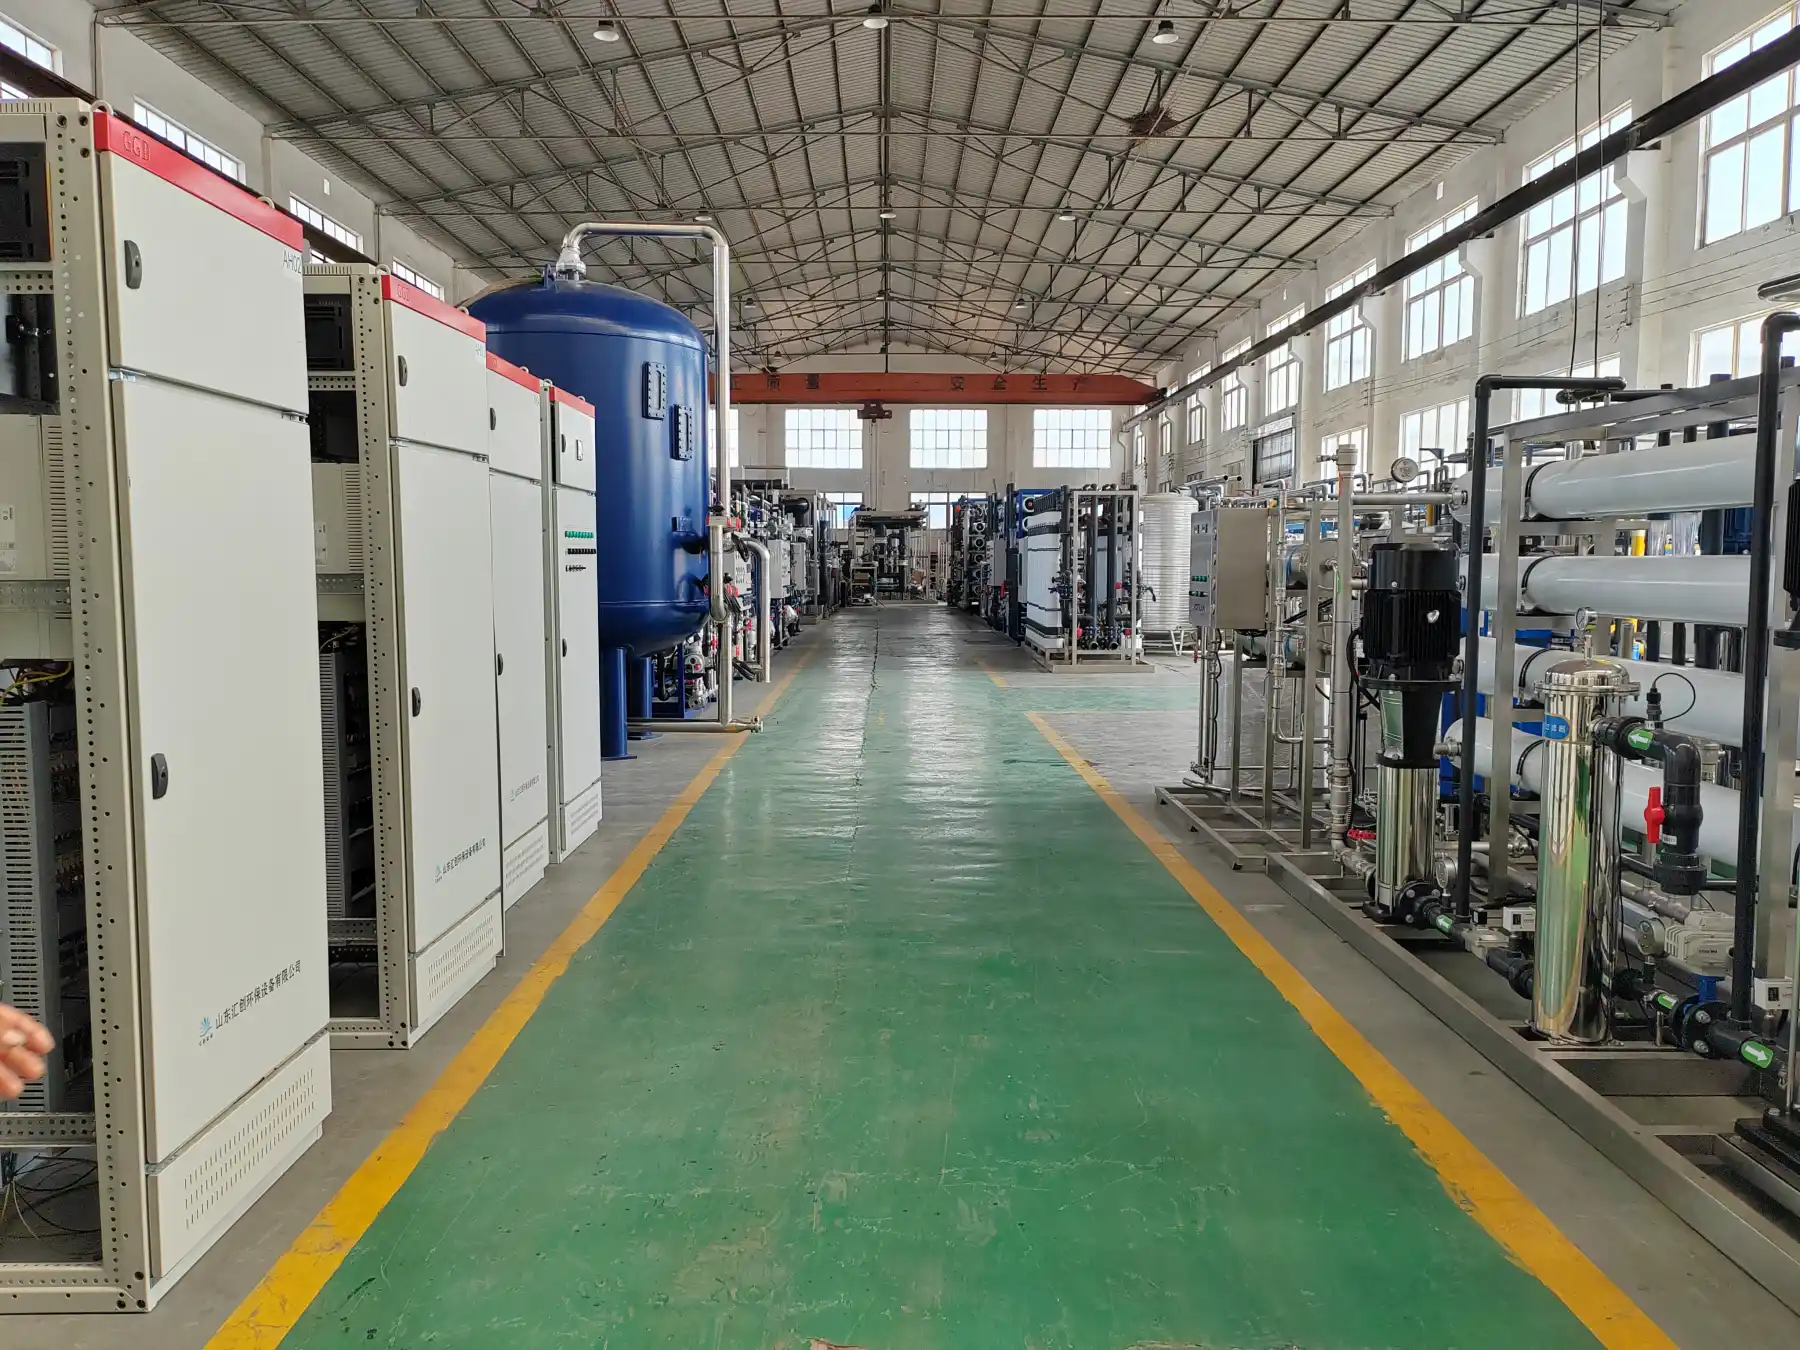
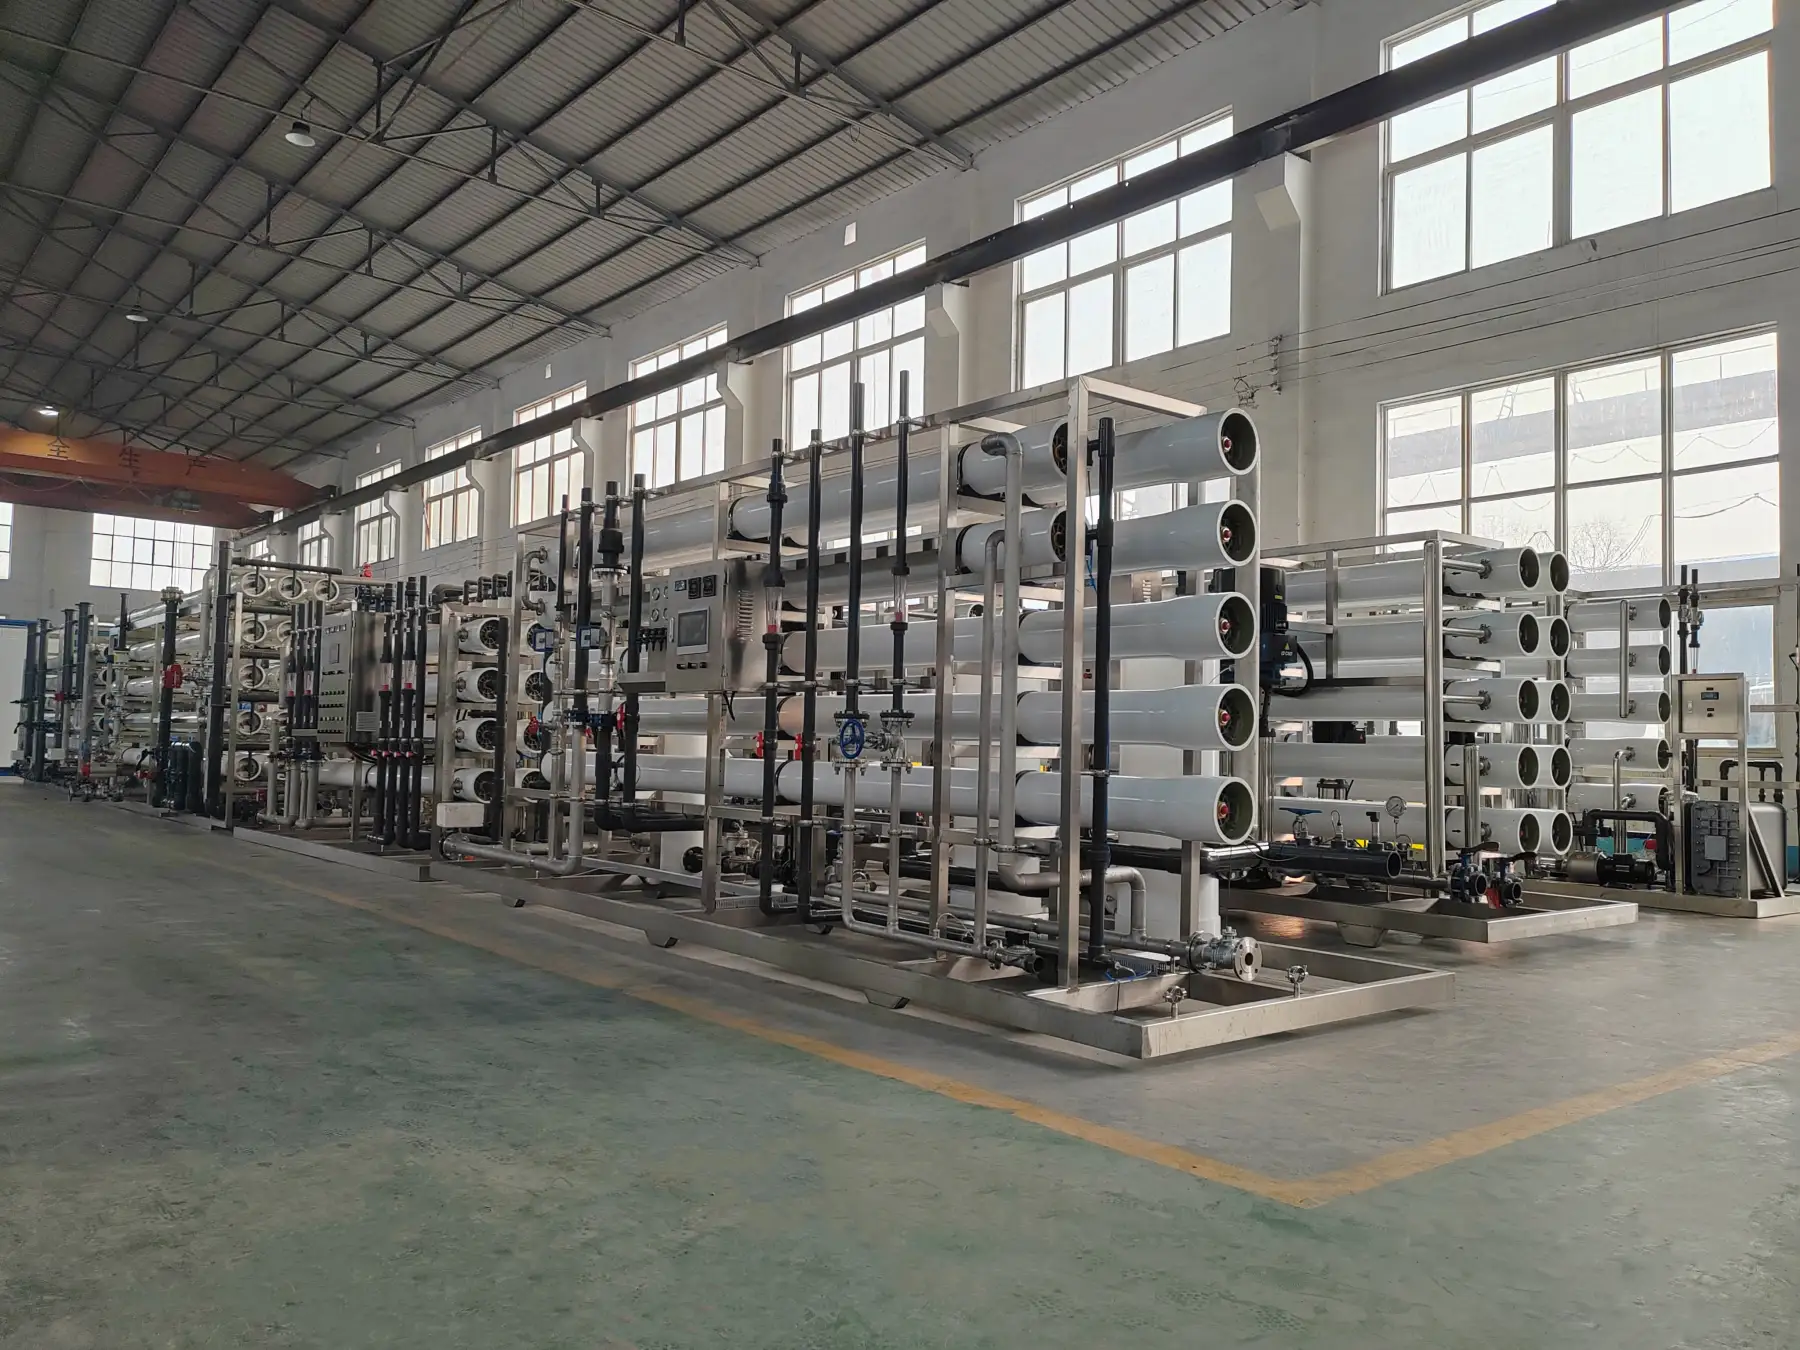
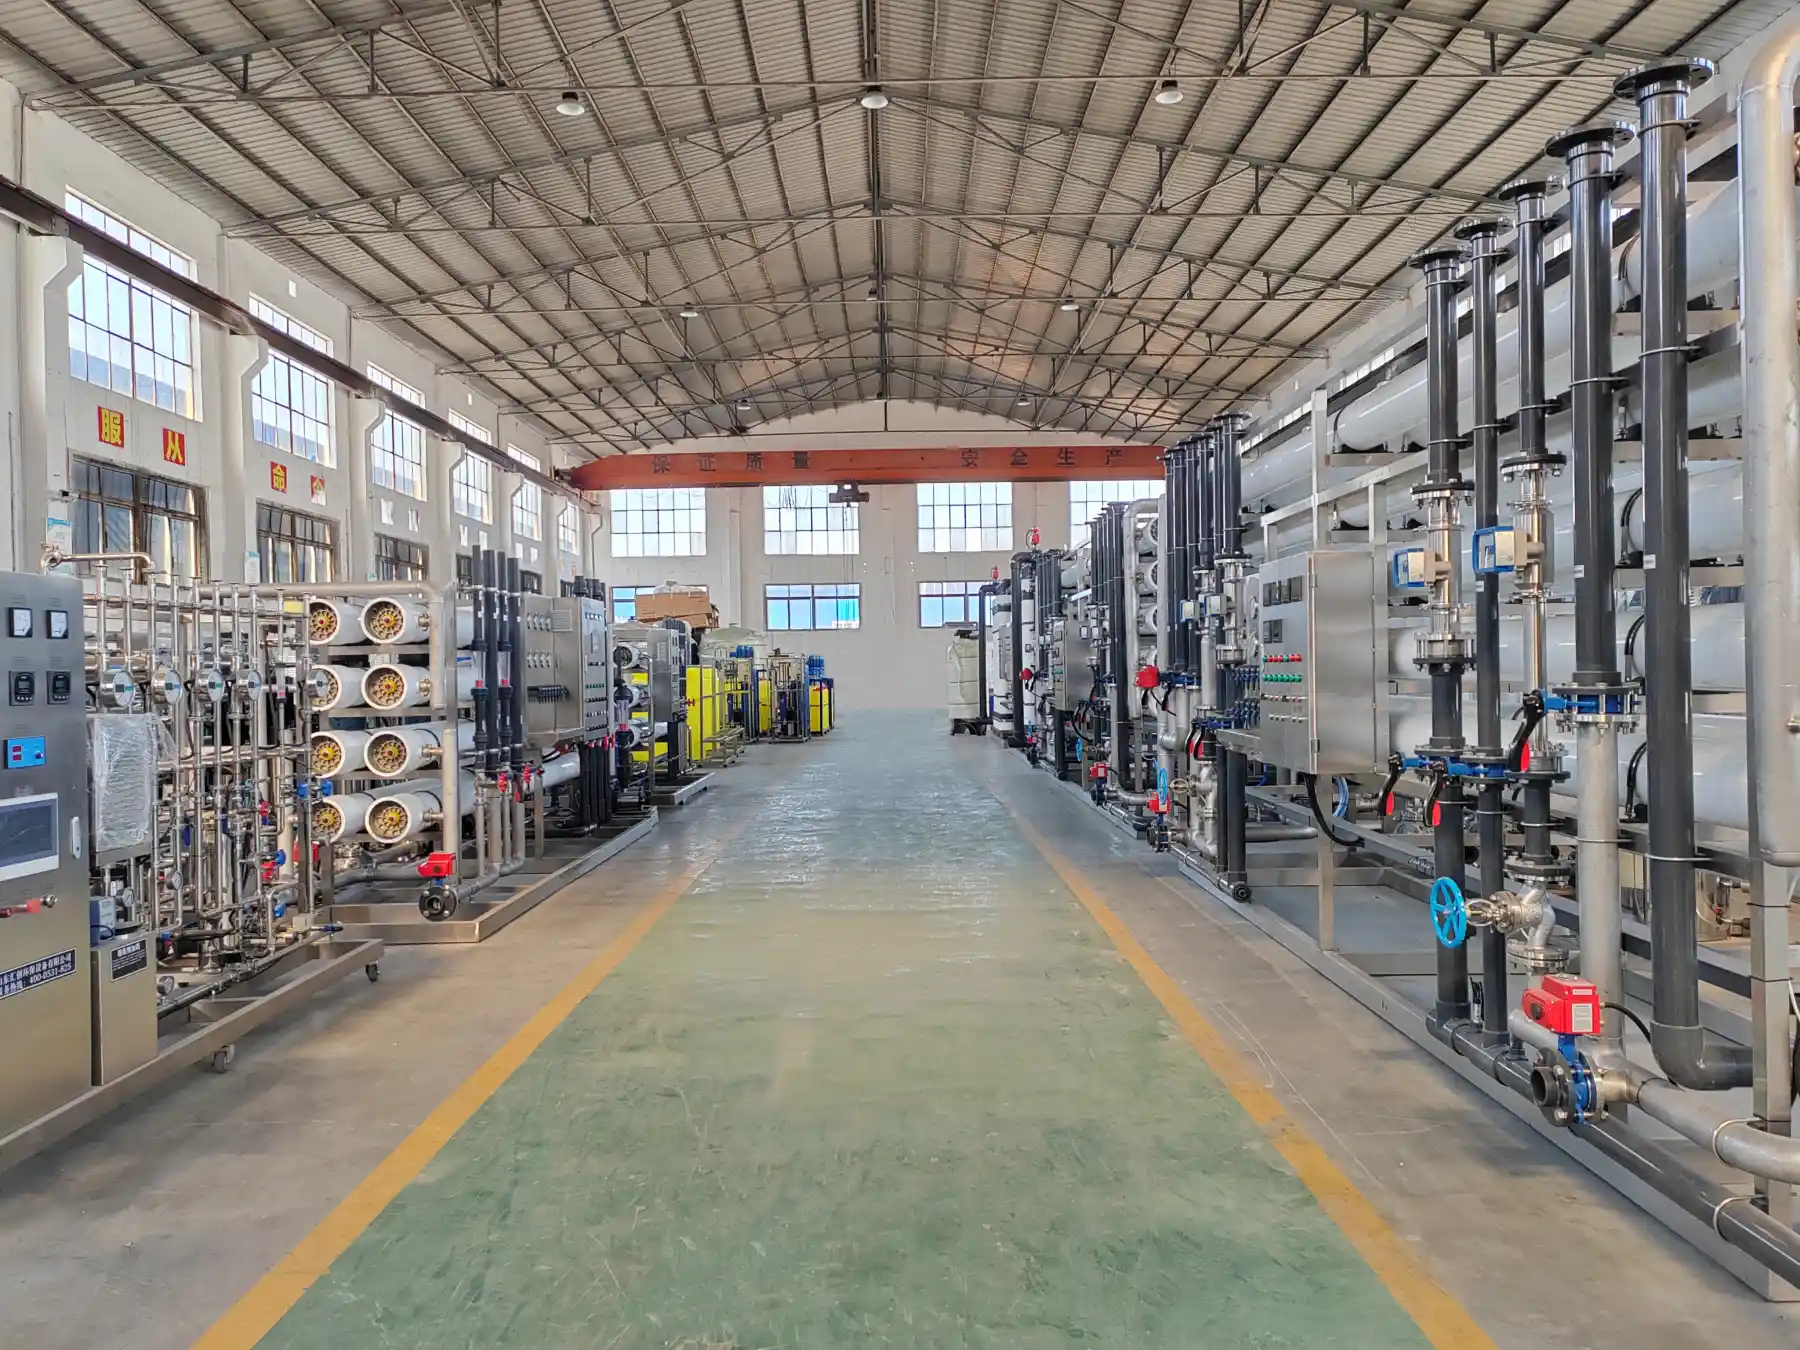
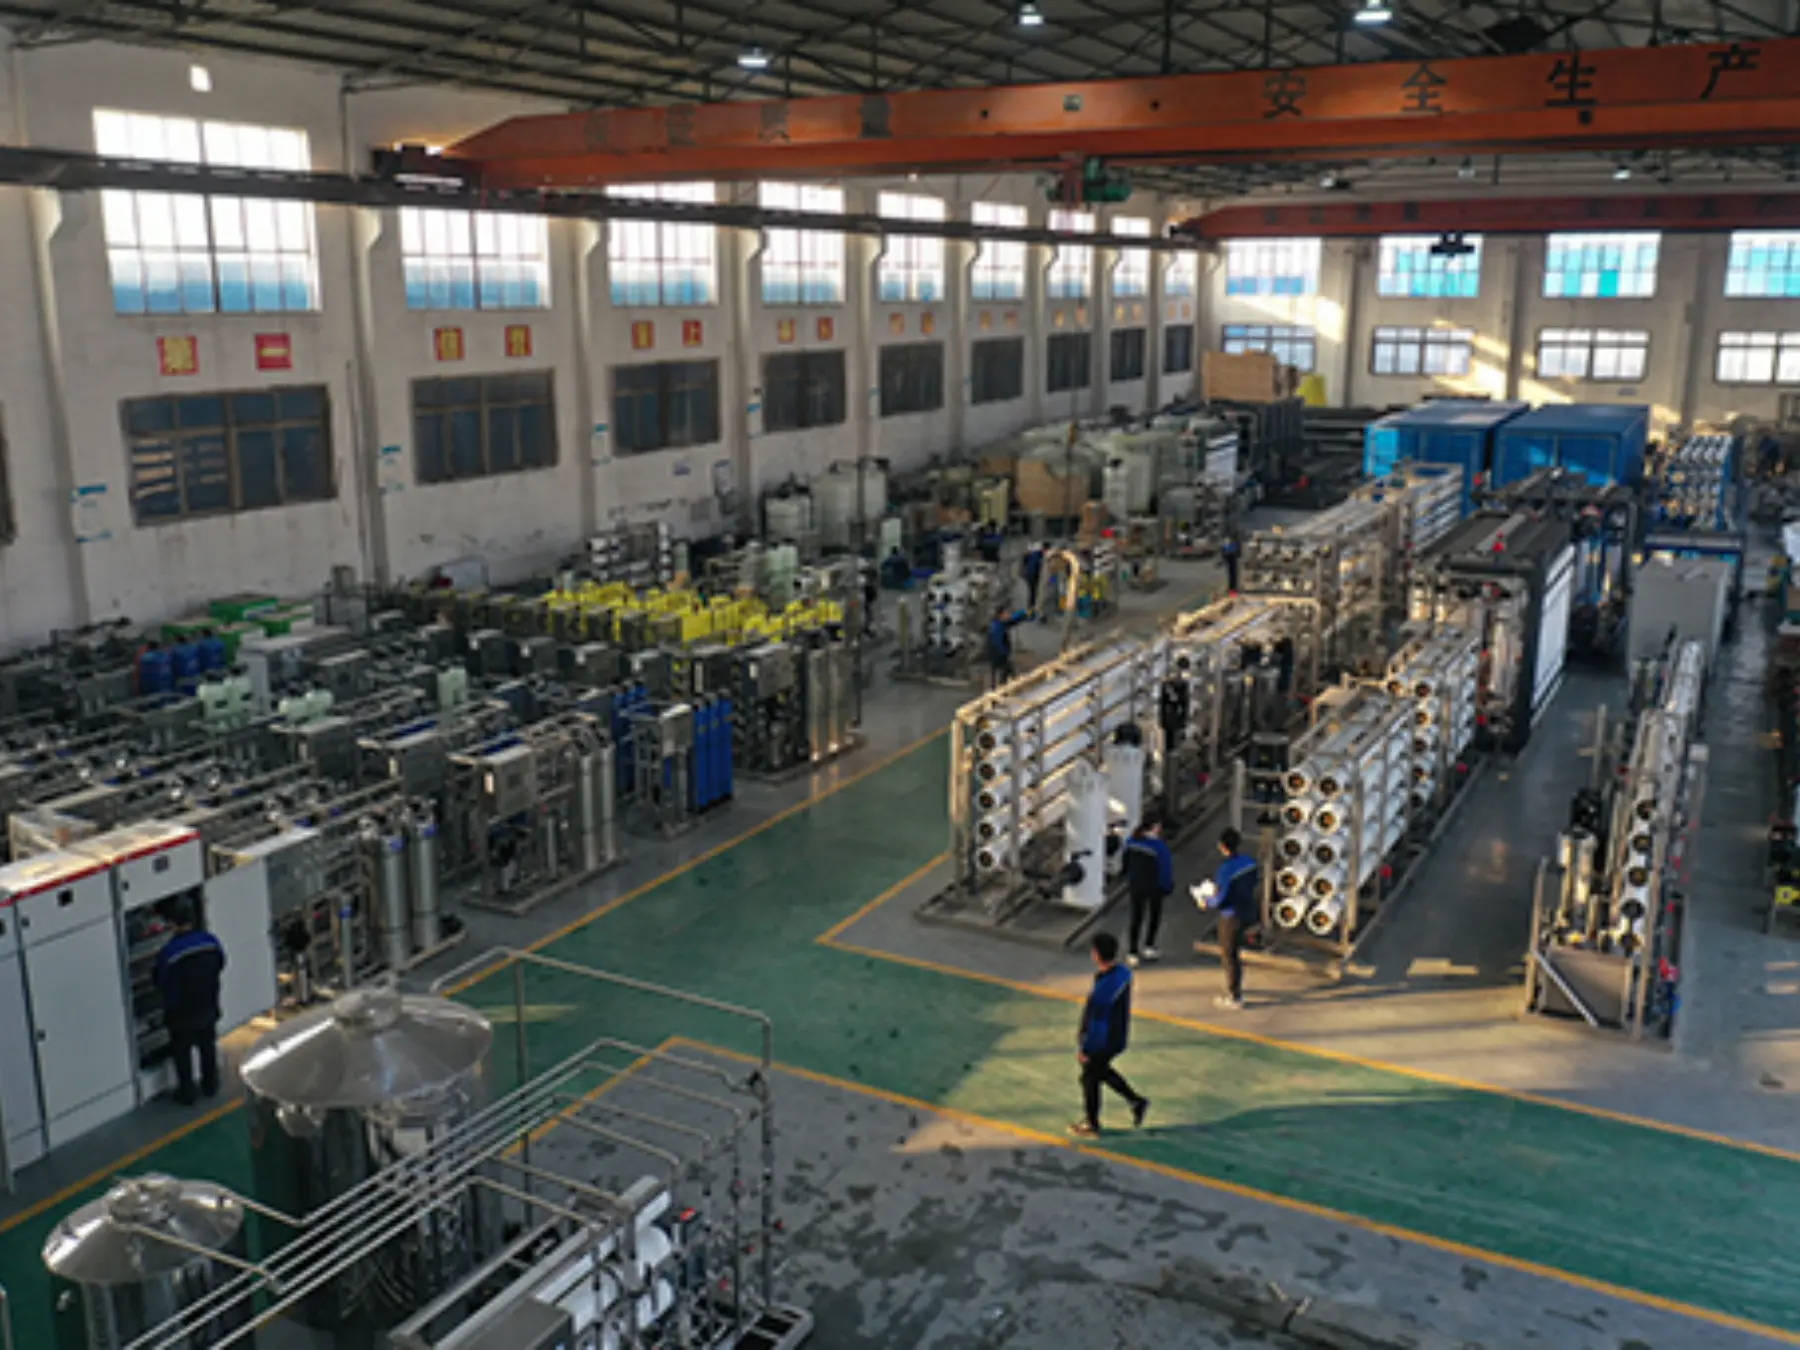
Partner with a Leading Certified Manufacturer: Supported by a 15,000 sqm production workshop, 15 senior design engineers, and a global track record of serving over 30,000 clients, Shandong Huichuang provides direct wholesale B2B pricing, complete engineering blueprints, and lifetime technical support. Contact our engineering desk today for a free custom CAD layout diagram and a competitive proposal for your wastewater project!
Reviews
There are no reviews yet.