

Heavy-Duty 10-100 T/H Packaged Industrial Water Reclamation & Reuse Plant
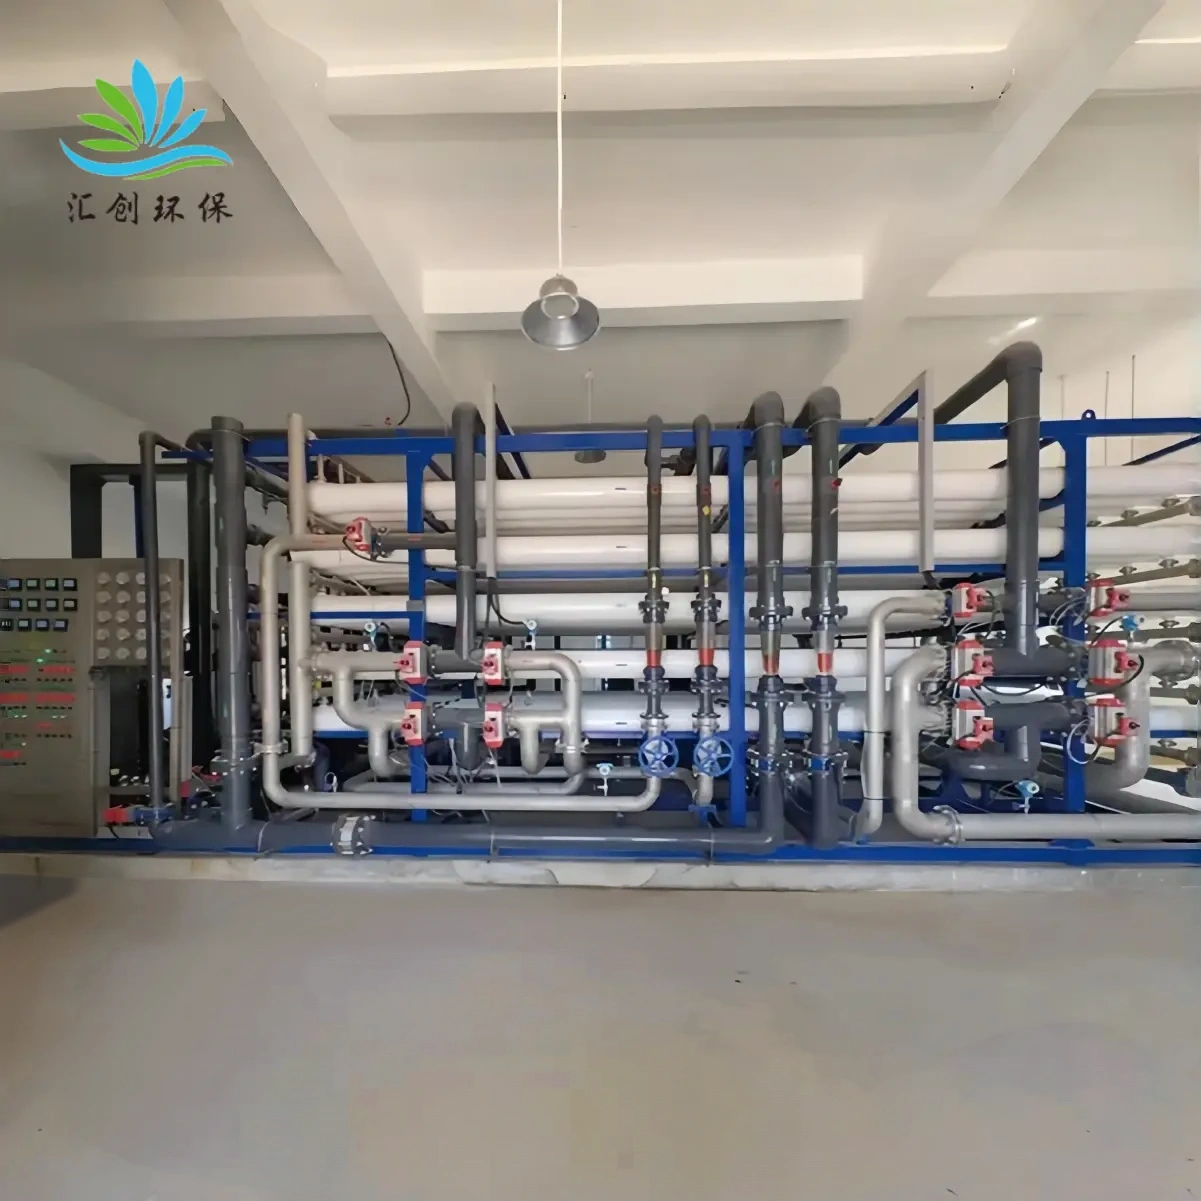
The HCQW-10T–100T Industrial Water Reclamation System designed and manufactured by Shandong Huichuang Environmental Protection Equipment Co., Ltd. is a turnkey, heavy-duty wastewater recycling plant engineered for advanced environmental compliance and massive resource conservation. Raw factory manufacturing effluent and municipal domestic sewage contain complex arrays of suspended solids, organic pollutants, heavy oils, dissolved salts, and high Chemical Oxygen Demand (COD). Directly discharging this water results in catastrophic eco-fines and wasted economic potential.
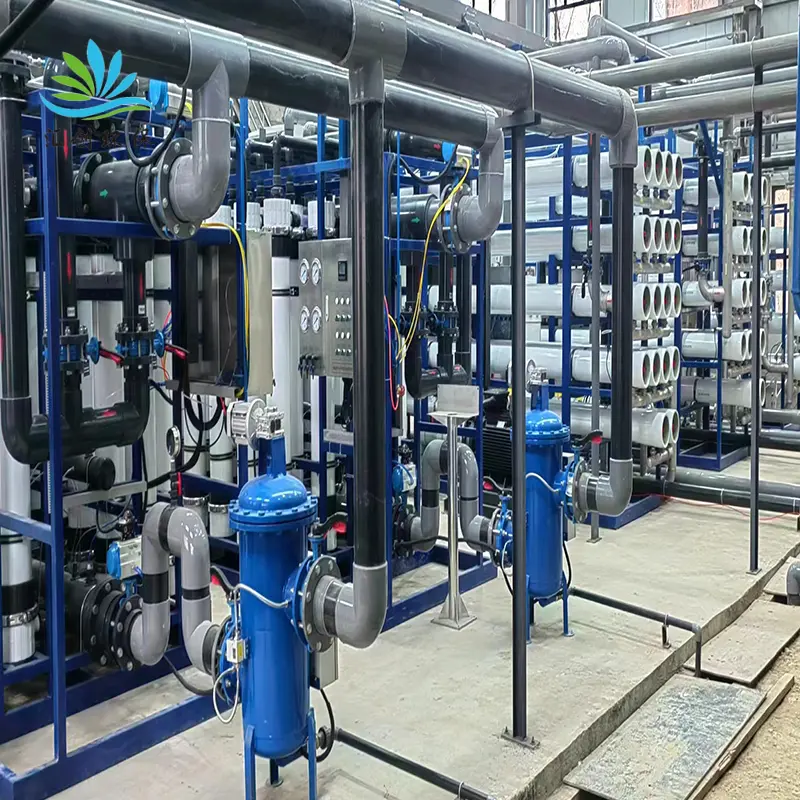
Our engineered water recycling systems solve these commercial challenges by transforming toxic waste streams into high-quality reclaimed water. Utilizing a state-of-the-art 6-stage combination process, this system deeply purifies complex wastewater to comply with the most stringent industrial reuse standards. It provides an immediate return on investment (ROI) by significantly slashing both freshwater consumption and wastewater discharge volumes.
Technical Specifications & Engineering Parameters
To assist global B2B procurement managers, facility directors, and EPC engineering contractors in matching their system requirements, here are the certified parameters for our HCQW series:
| Technical Parameter Item | Industrial Specification Details |
|---|---|
| Model Series Designation | HCQW-10T to HCQW-100T High-Volume Line |
| Production Water Capacity | 10 to 100 Tons / Hour (10,000 – 100,000 LPH Customizable Skids) |
| Working Operating Pressure | 1.0 – 1.5 MPa (Optimized hydraulic engineering) |
| Water Recovery Efficiency Rate | 60% – 75% (Highly sustainable brine concentration reduction) |
| Core Treatment Technology | 6-Stage Process: AO + MBR + UF + RO Combined Membrane Technology |
| Power Supply Required | 380V / 50Hz (Industrial Three-Phase) – Global adaptive options available |
| Standard Model Dimensions | 680 x 120 x 260 cm (Highly compact modular frame design) |
| Design & Reuse Compliance | Strictly complies with Global Reclaimed Non-Potable Water Quality Standards |
| Applicable Source Water | Industrial Production Wastewater, Domestic Sewage, Municipal Mixed Graywater |
Advanced 6-Stage Deep Treatment & Membrane Architecture
To secure flawless effluent clarity even under massive peak-load wastewater shocks, our recycling plant relies on a scientifically balanced chemical, biological, and physical filtration matrix:
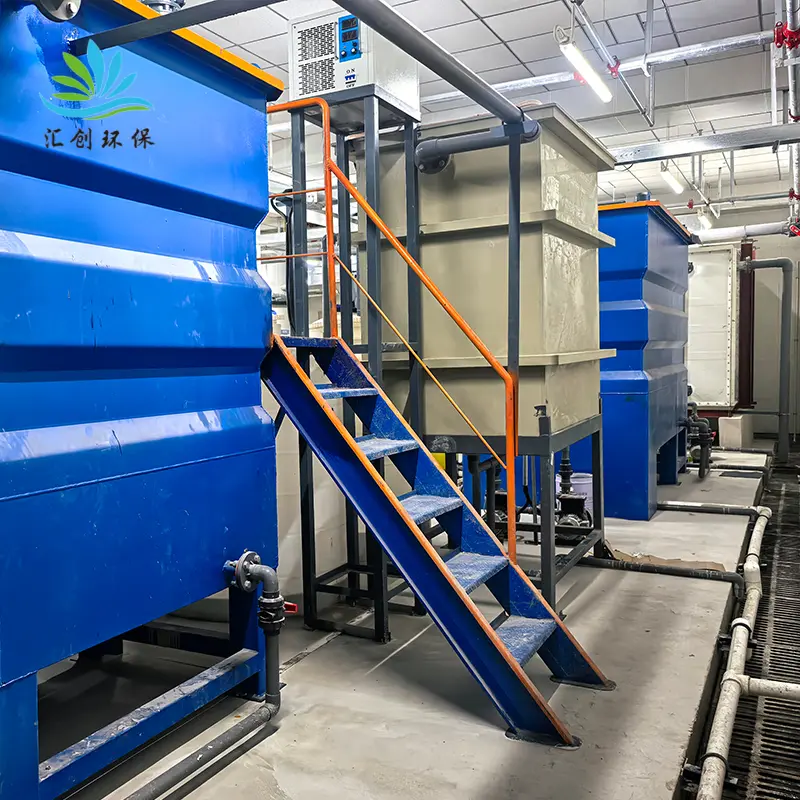
- 1. Mechanical Pretreatment & Clarification: Raw wastewater passes through settlement tanks and mechanical screens to strip away heavy mud, sand, hair, grit, and floating oil slicks.
- 2. AO Biological Degradation: The fluid moves into alternating Anaerobic/Anoxic (A) and Oxic (O) biological zones. Highly concentrated bio-bacterial colonies break down complex organic carbon structures, nitrides, and ammonia nitrogen.
- 3. MBR (Membrane Bioreactor) Clarification: High-flux submerged MBR membrane modules catch 100% of biological sludge flocs and bacteria, achieving exceptional organic reduction and stabilizing water clarity.
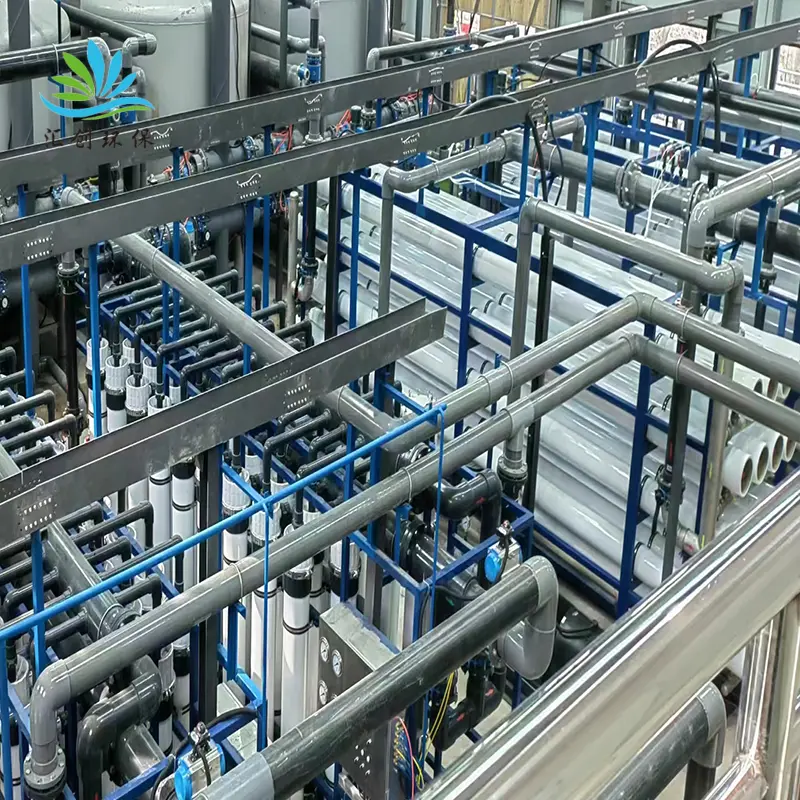
- 4. Precision Ultrafiltration (UF) Guard: Hollow fiber UF membranes act as a highly protective barrier, trapping macromolecular compounds, colloidal silica, and tiny particulates to lower the Silt Density Index (SDI).
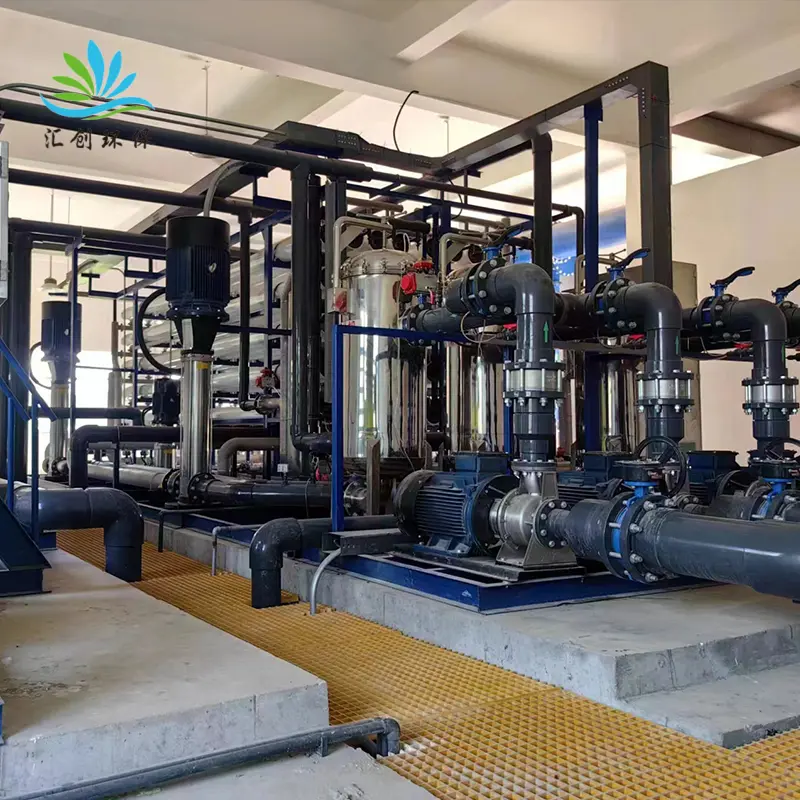
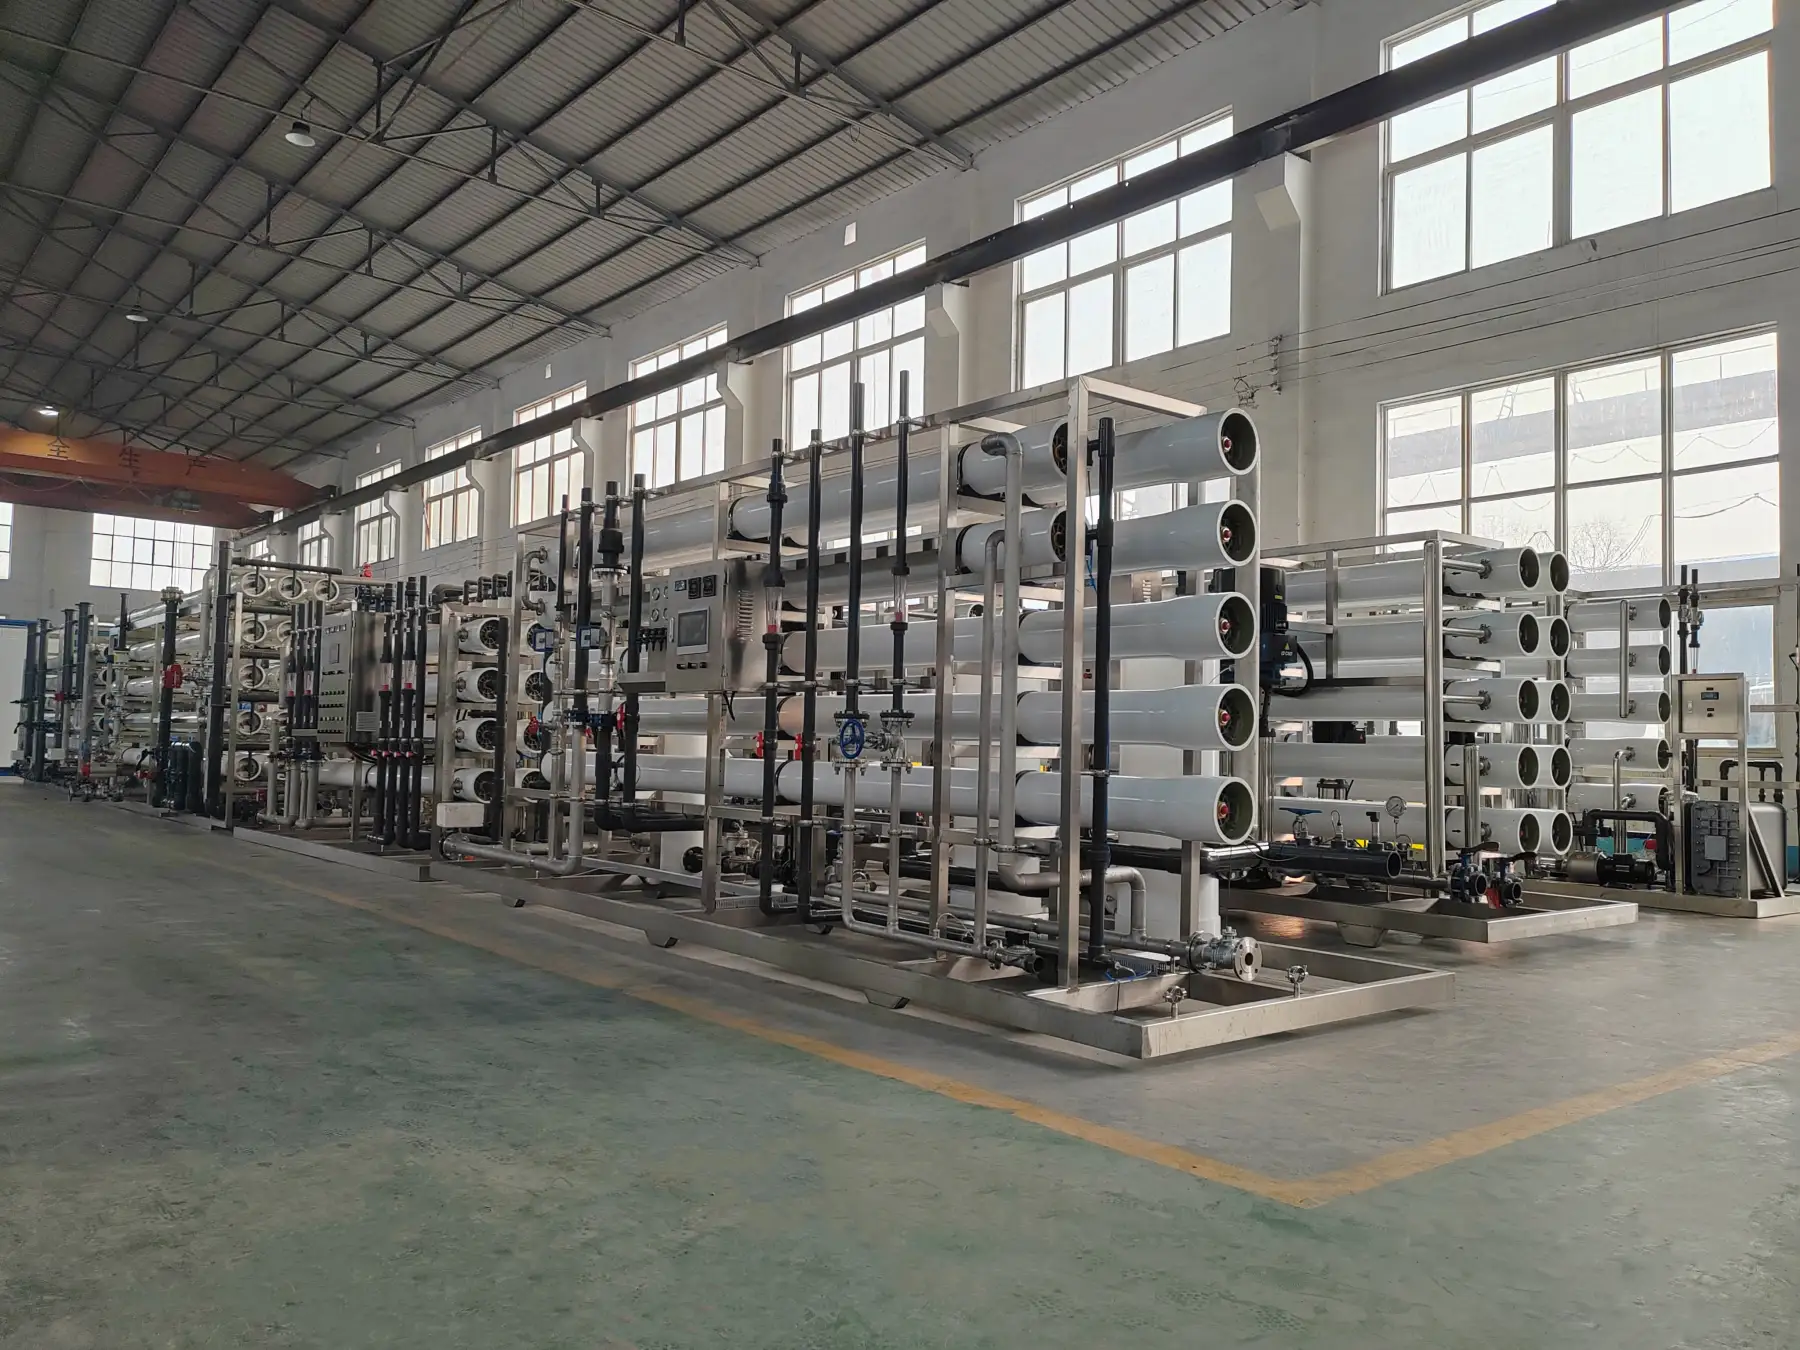
- 5. High-Rejection RO Purification: Driven by multi-stage high-pressure pumps, the water flows through premium reverse osmosis membranes, stripping away dissolved heavy metals, microscopic salts, residual chemical ions, and trace organic matter.
- 6. Disinfection & Post-Polishing: A final UV or chlorination treatment ensures the reclaimed water emerges crystal-clear, odorless, and completely sanitary for immediate storage.
Why Invest in Huichuang Wastewater Recycling Infrastructure?
- Massive Economic Returns & Cost Reduction: By reclaiming 60% to 75% of your factory’s waste fluid, this equipment directly replaces expensive municipal fresh water with premium on-site graywater. It slashes your water utility bills and drastically reduces your environmental wastewater tax.
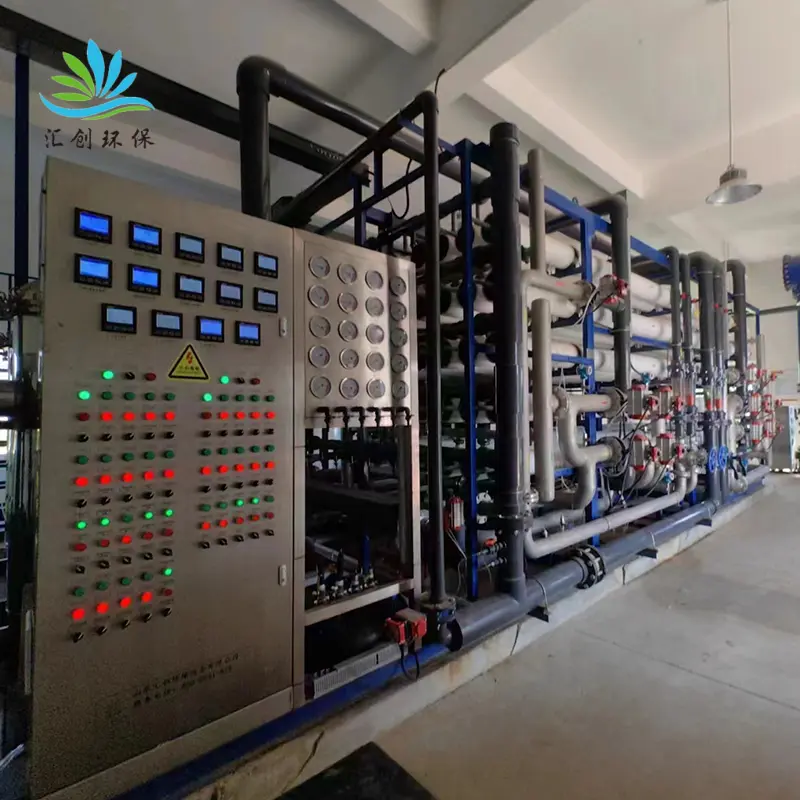
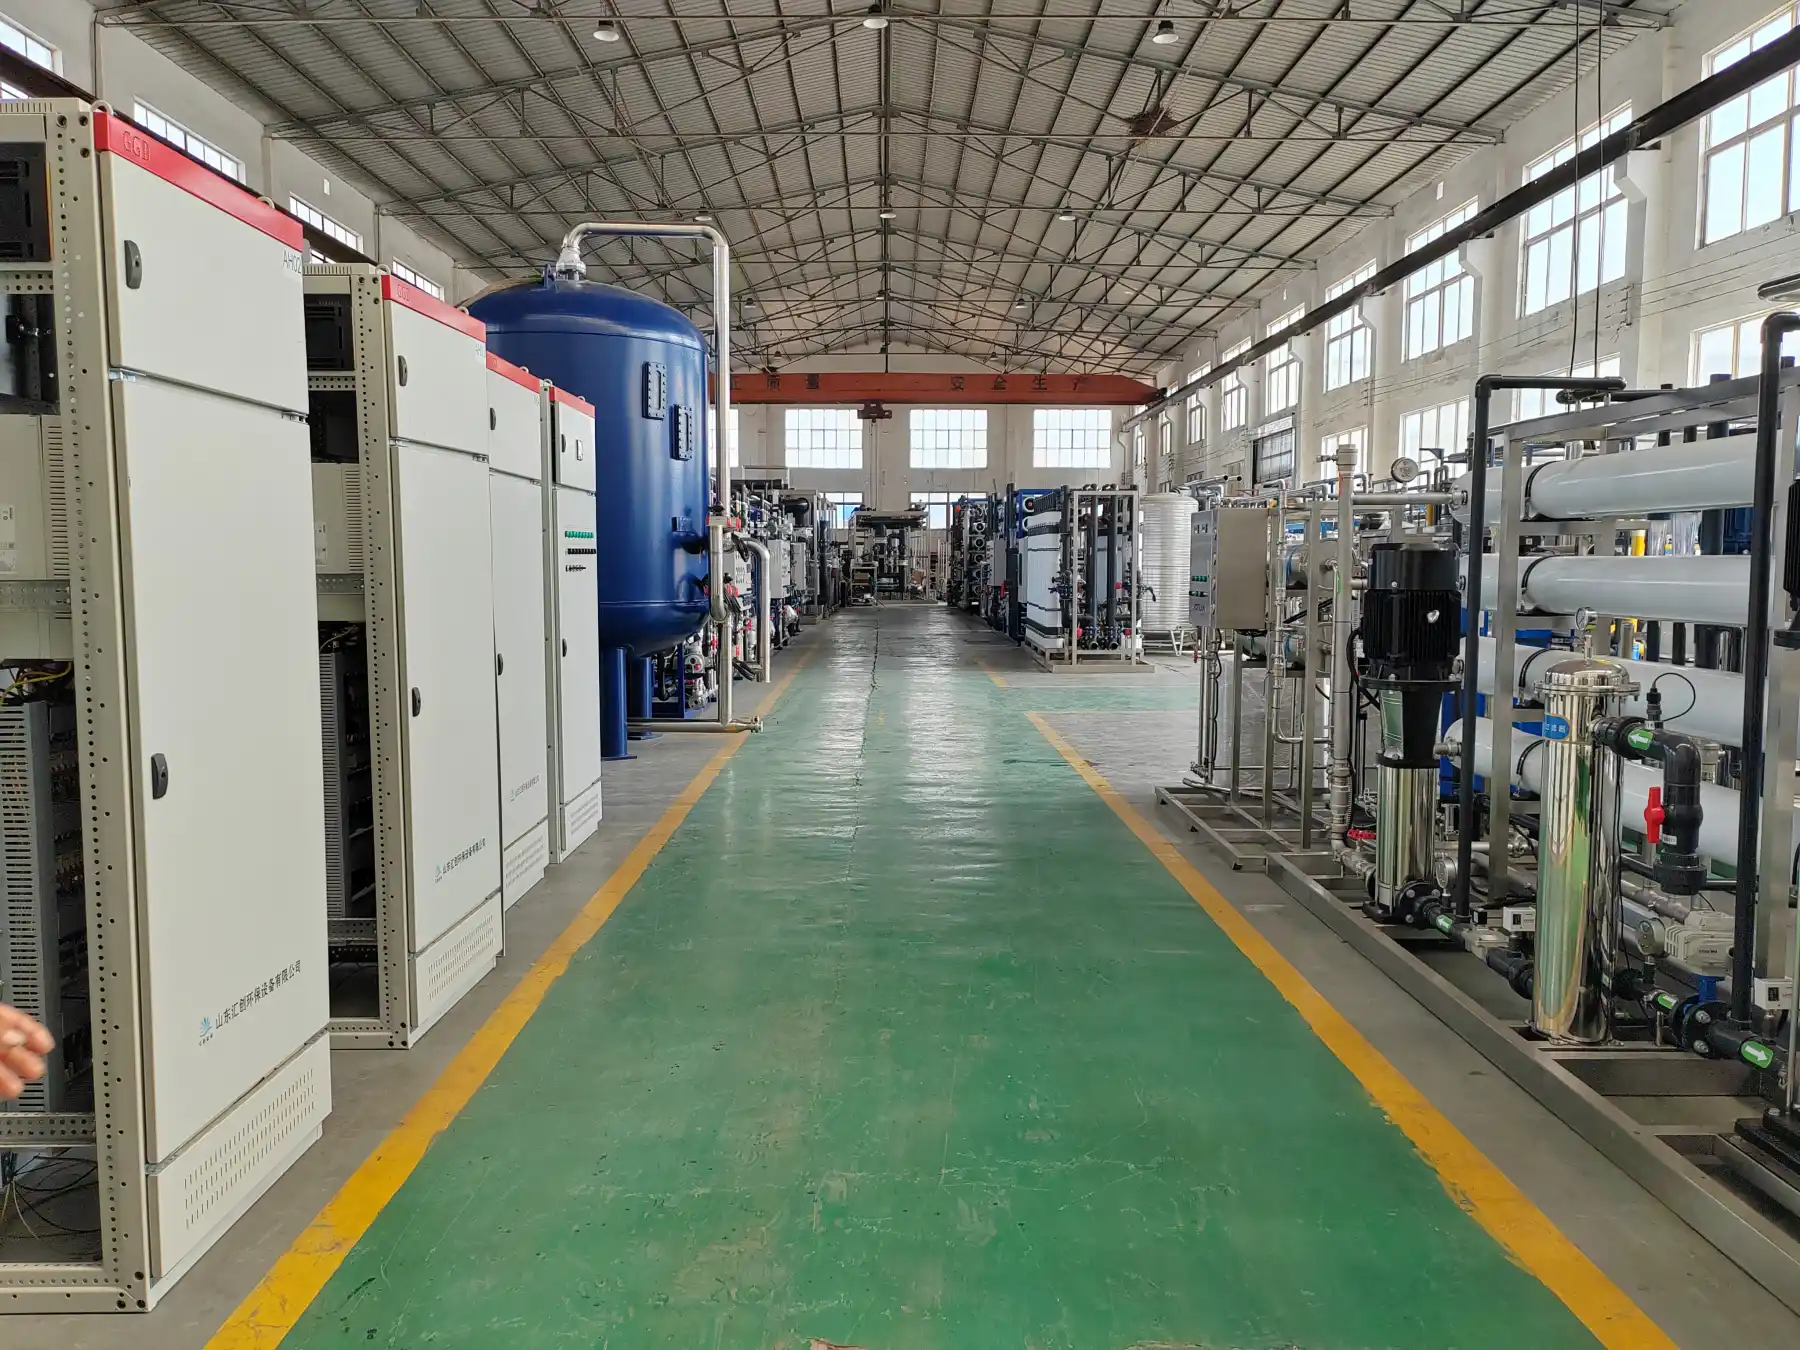
- Smart 24/7 Automation via Centralized PLC: The integrated smart electrical control panel automates water intake, chemical dosing, backwashing, and safety diagnostics. The entire multi-tier system operates seamlessly all day without full-time on-site labor.
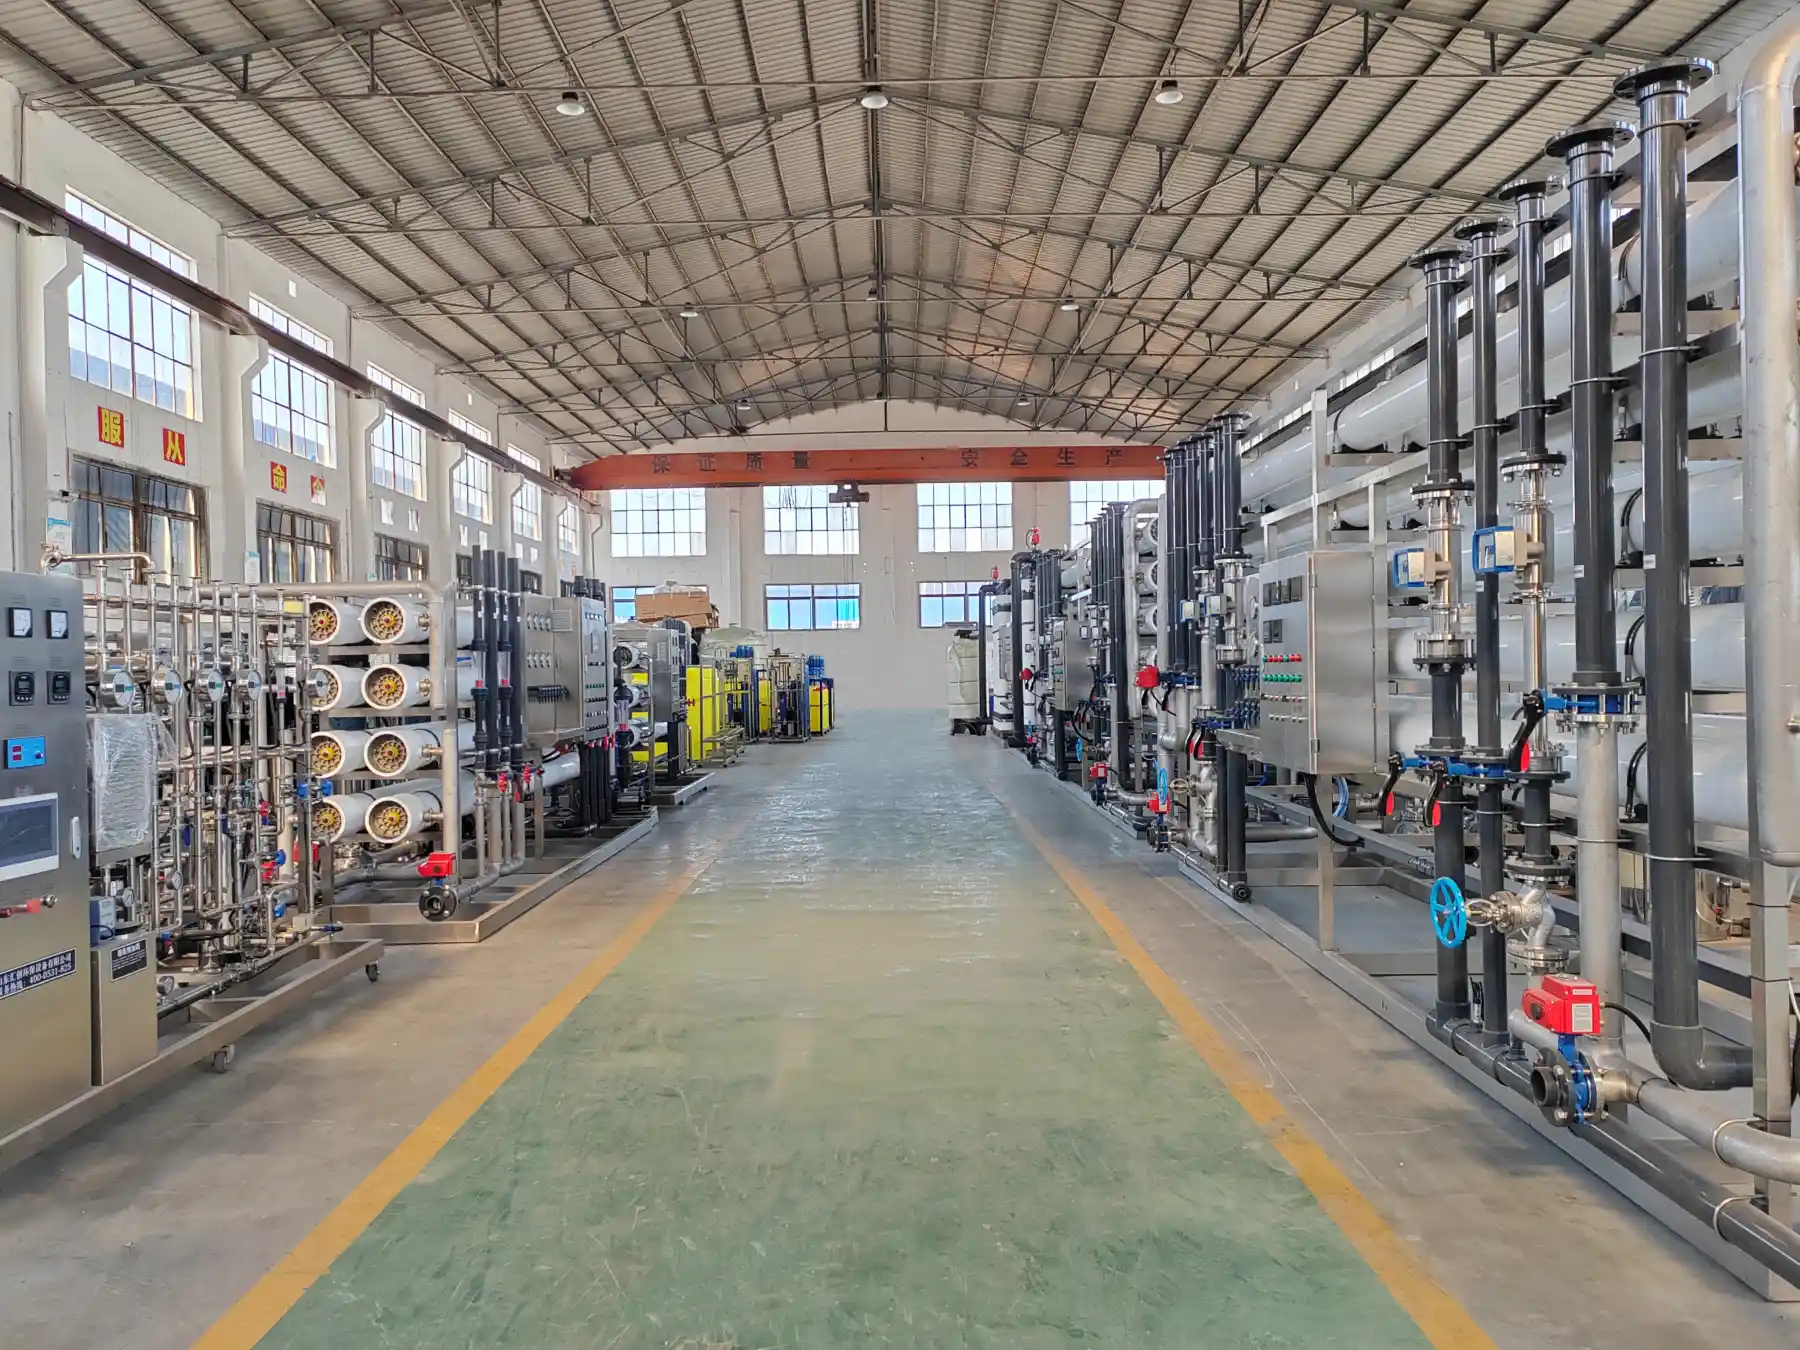
- Compact Modular Skid-Mounted Blueprint: Traditional sewage basins require immense concrete real estate and weeks of disruptive civil construction. Our compact skid-mounted steel architecture fits easily within your existing mechanical floor footprint, ensuring fast plug-and-play installation.
- Exceptional Fluid Shock Resistance: Engineered with a resilient biomass buffer framework and low-fouling membranes, our equipment effortlessly absorbs sudden changes in chemical and volume loads without experiencing system crashes.
Target Applications & Commercial Sectors
Our heavy-duty water reclamation plants are trusted by EPC firms, municipal planners, and factory owners globally across multiple sectors:
- Industrial Manufacturing Hubs: Providing continuous recycled process makeup water, chemical reaction cooling, and textile rinsing fluid for electronic, textile, and pharmaceutical complexes.
- Commercial Facilities & Buildings: Supplying reliable graywater for centralized central air conditioning cooling loops, floor flushing, and landscape greening in luxury hotels, office towers, and high-density communities.
- Municipal & Smart Town Infrastructure: Turnkey municipal graywater networks and corporate industrial park wastewater treatments aiming for zero-liquid-discharge (ZLD) milestones.
Frequently Asked Questions (FAQ)
What are the primary reuse options for water treated by this AO+MBR+UF+RO system?
The output water is premium-grade, clear, and completely odorless. It is highly suited for high-volume non-potable industrial uses, including cooling tower loop makeup, mechanical boiler feeding, large-scale facility floor washing, advanced agricultural irrigation, and industrial process recycling.
How does the system prevent the RO and UF membranes from fouling when treating wastewater?
Our multi-tier design utilizes high-flux AO and MBR bioprocesses as an exceptional pretreatment shield. By stripping away 99% of organic loading, suspended solids, and biomass flocs before the water ever contacts the UF or RO units, the system prevents membrane scaling, drastically reducing chemical cleaning (CIP) requirements to only a few times a year.
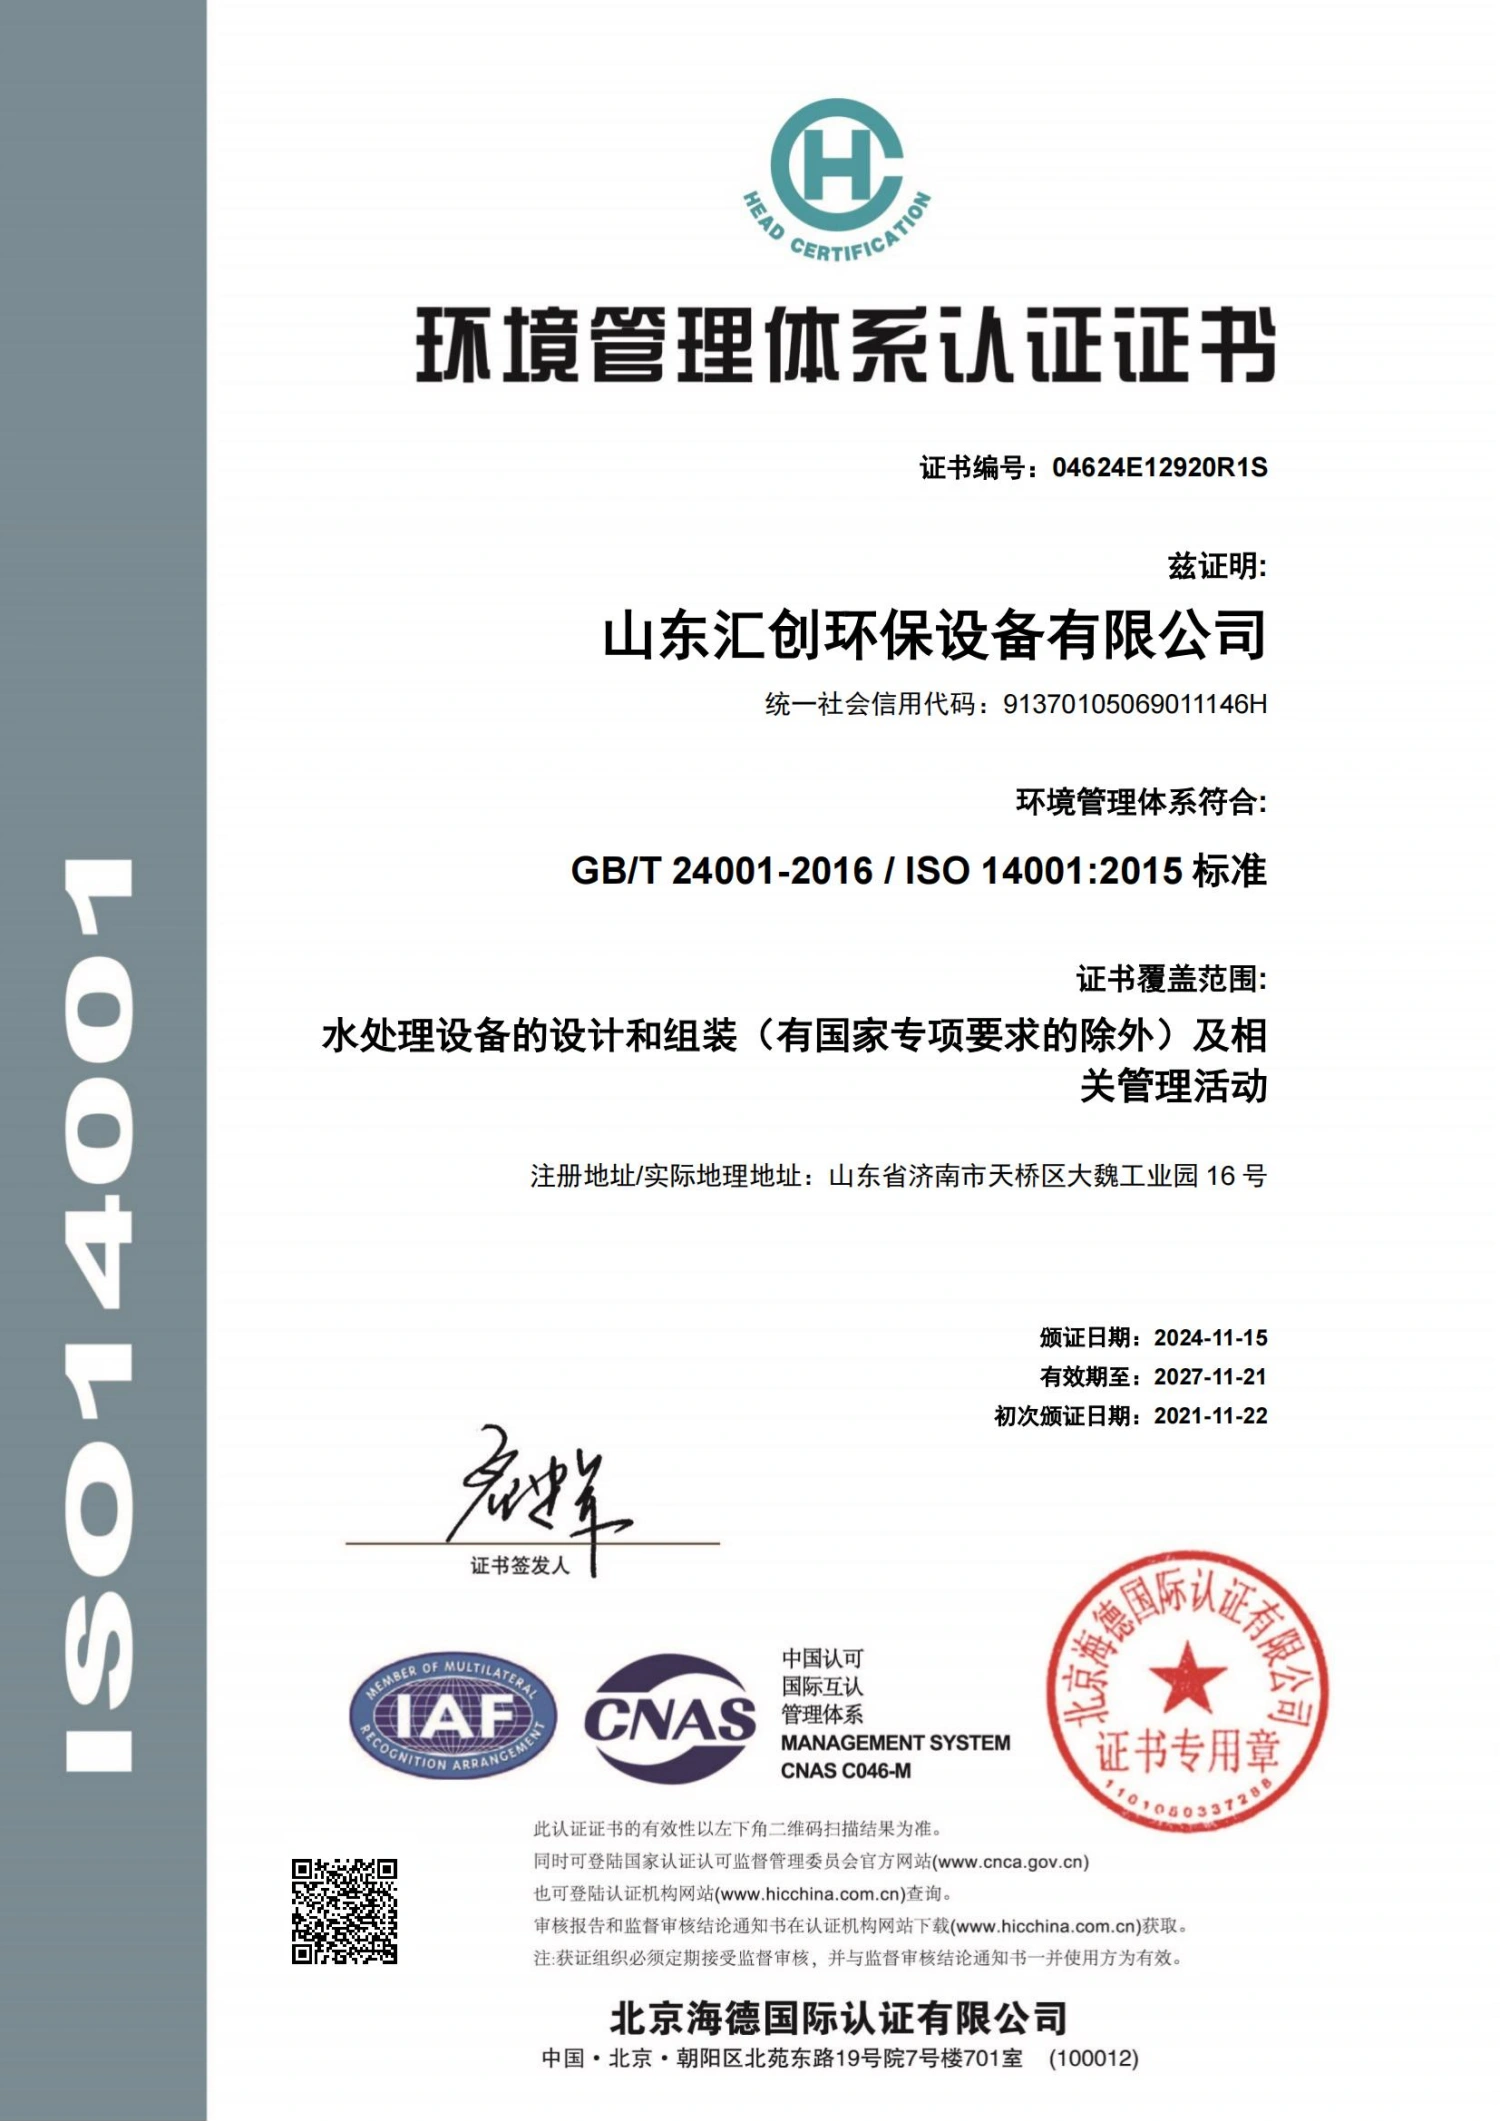
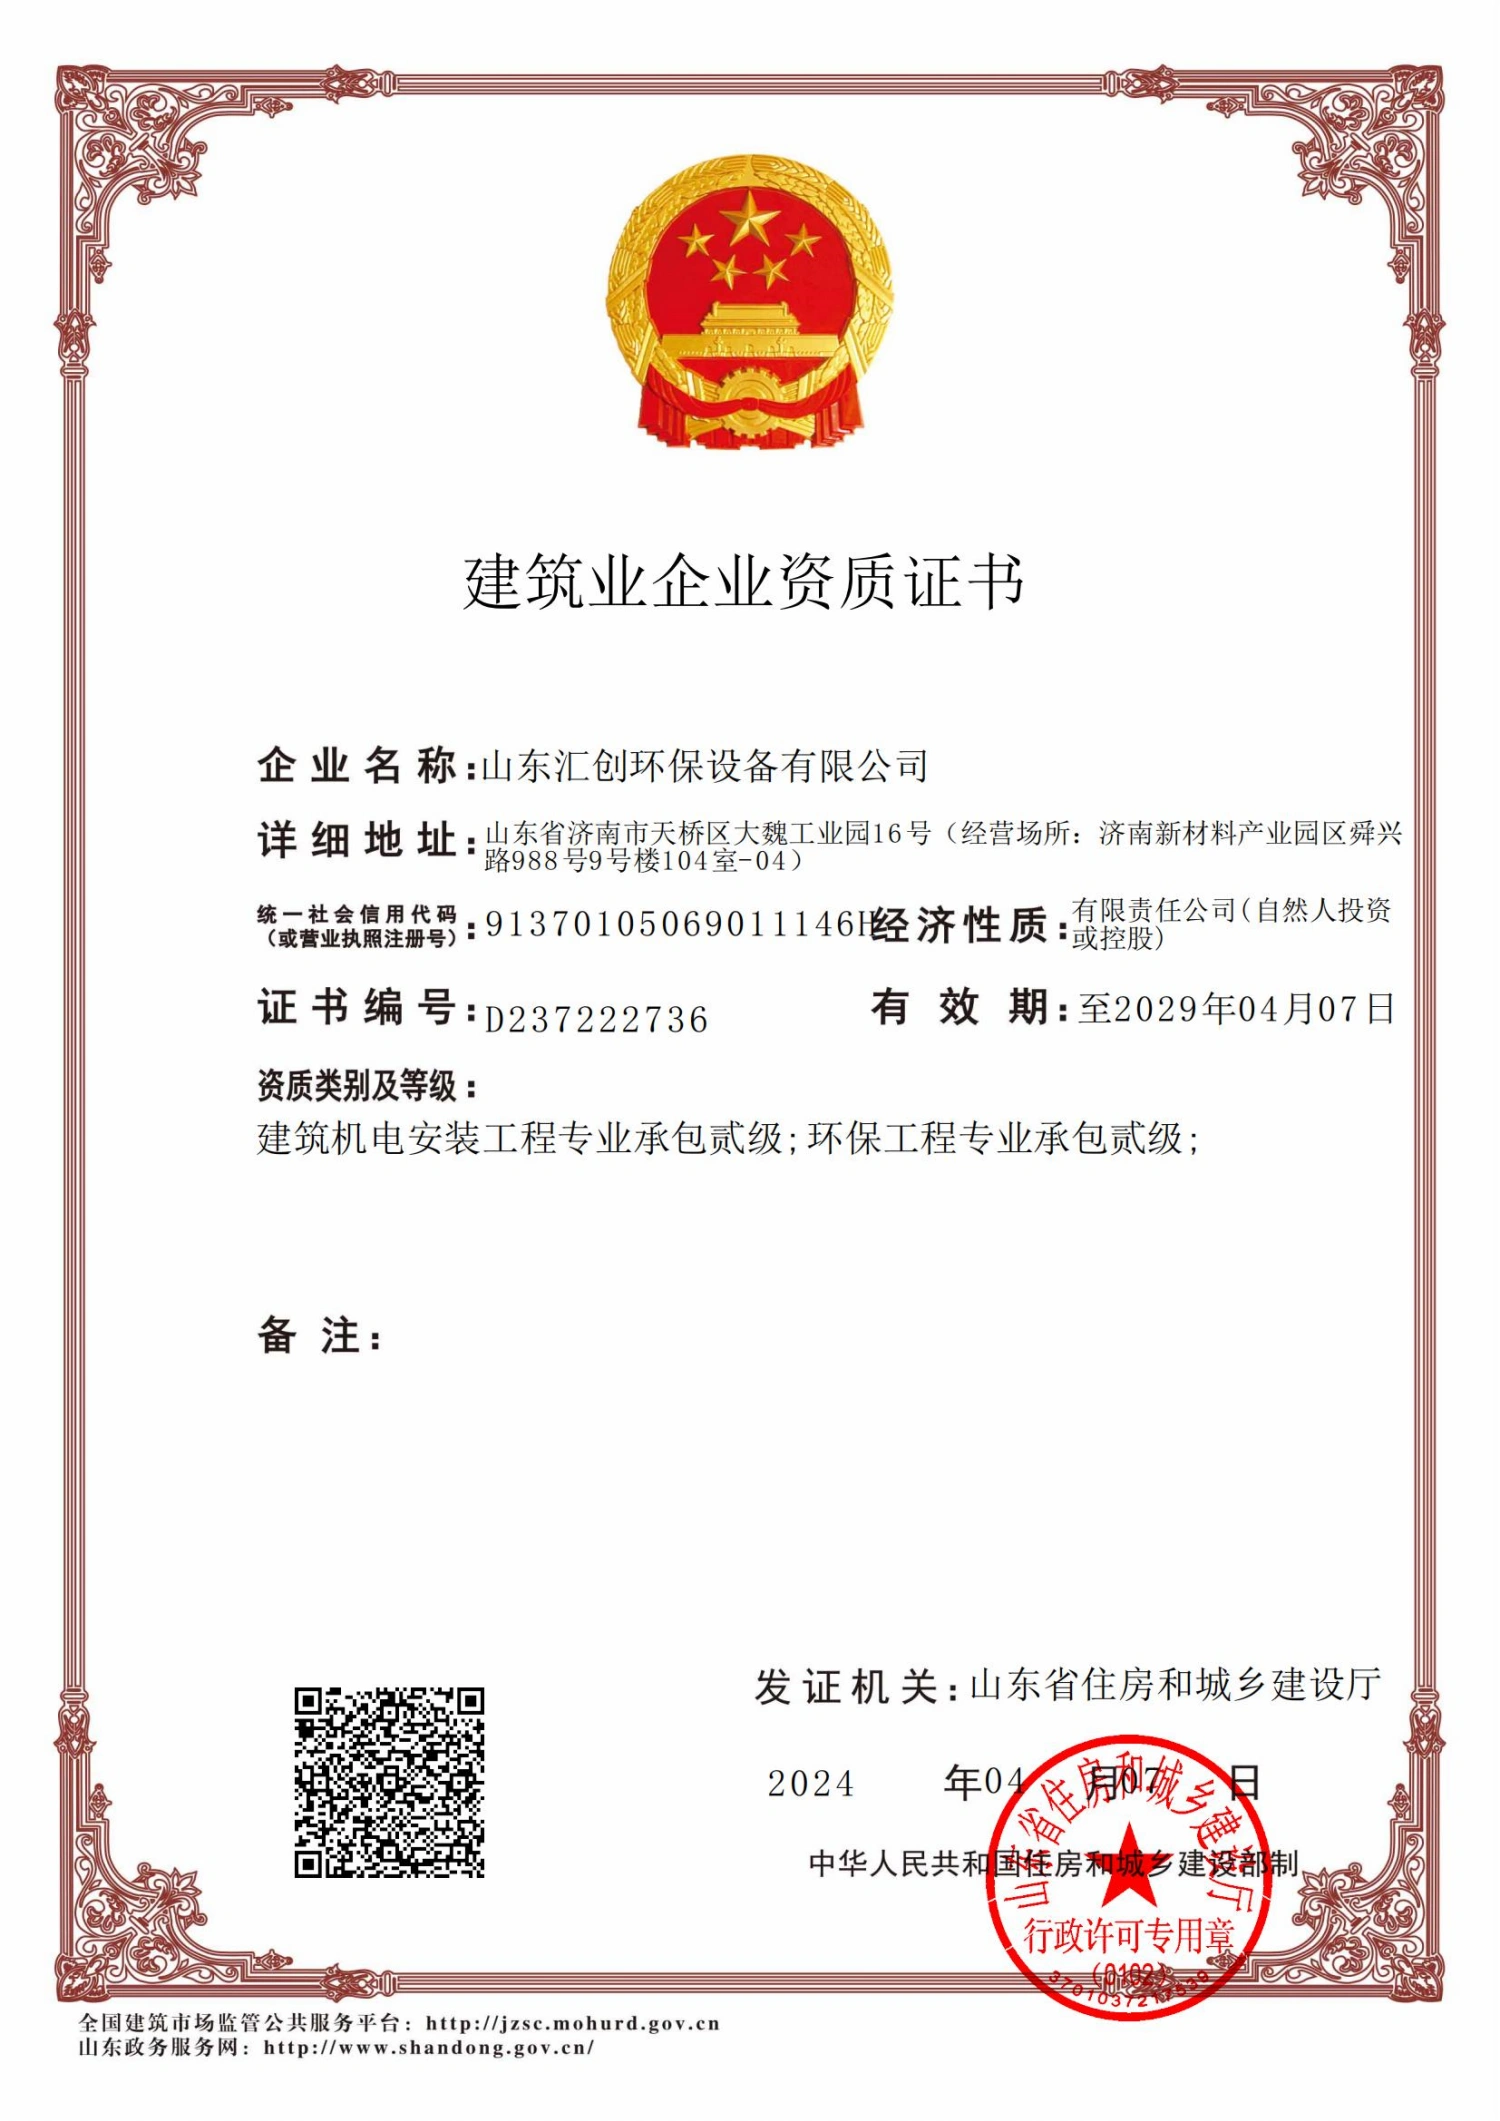
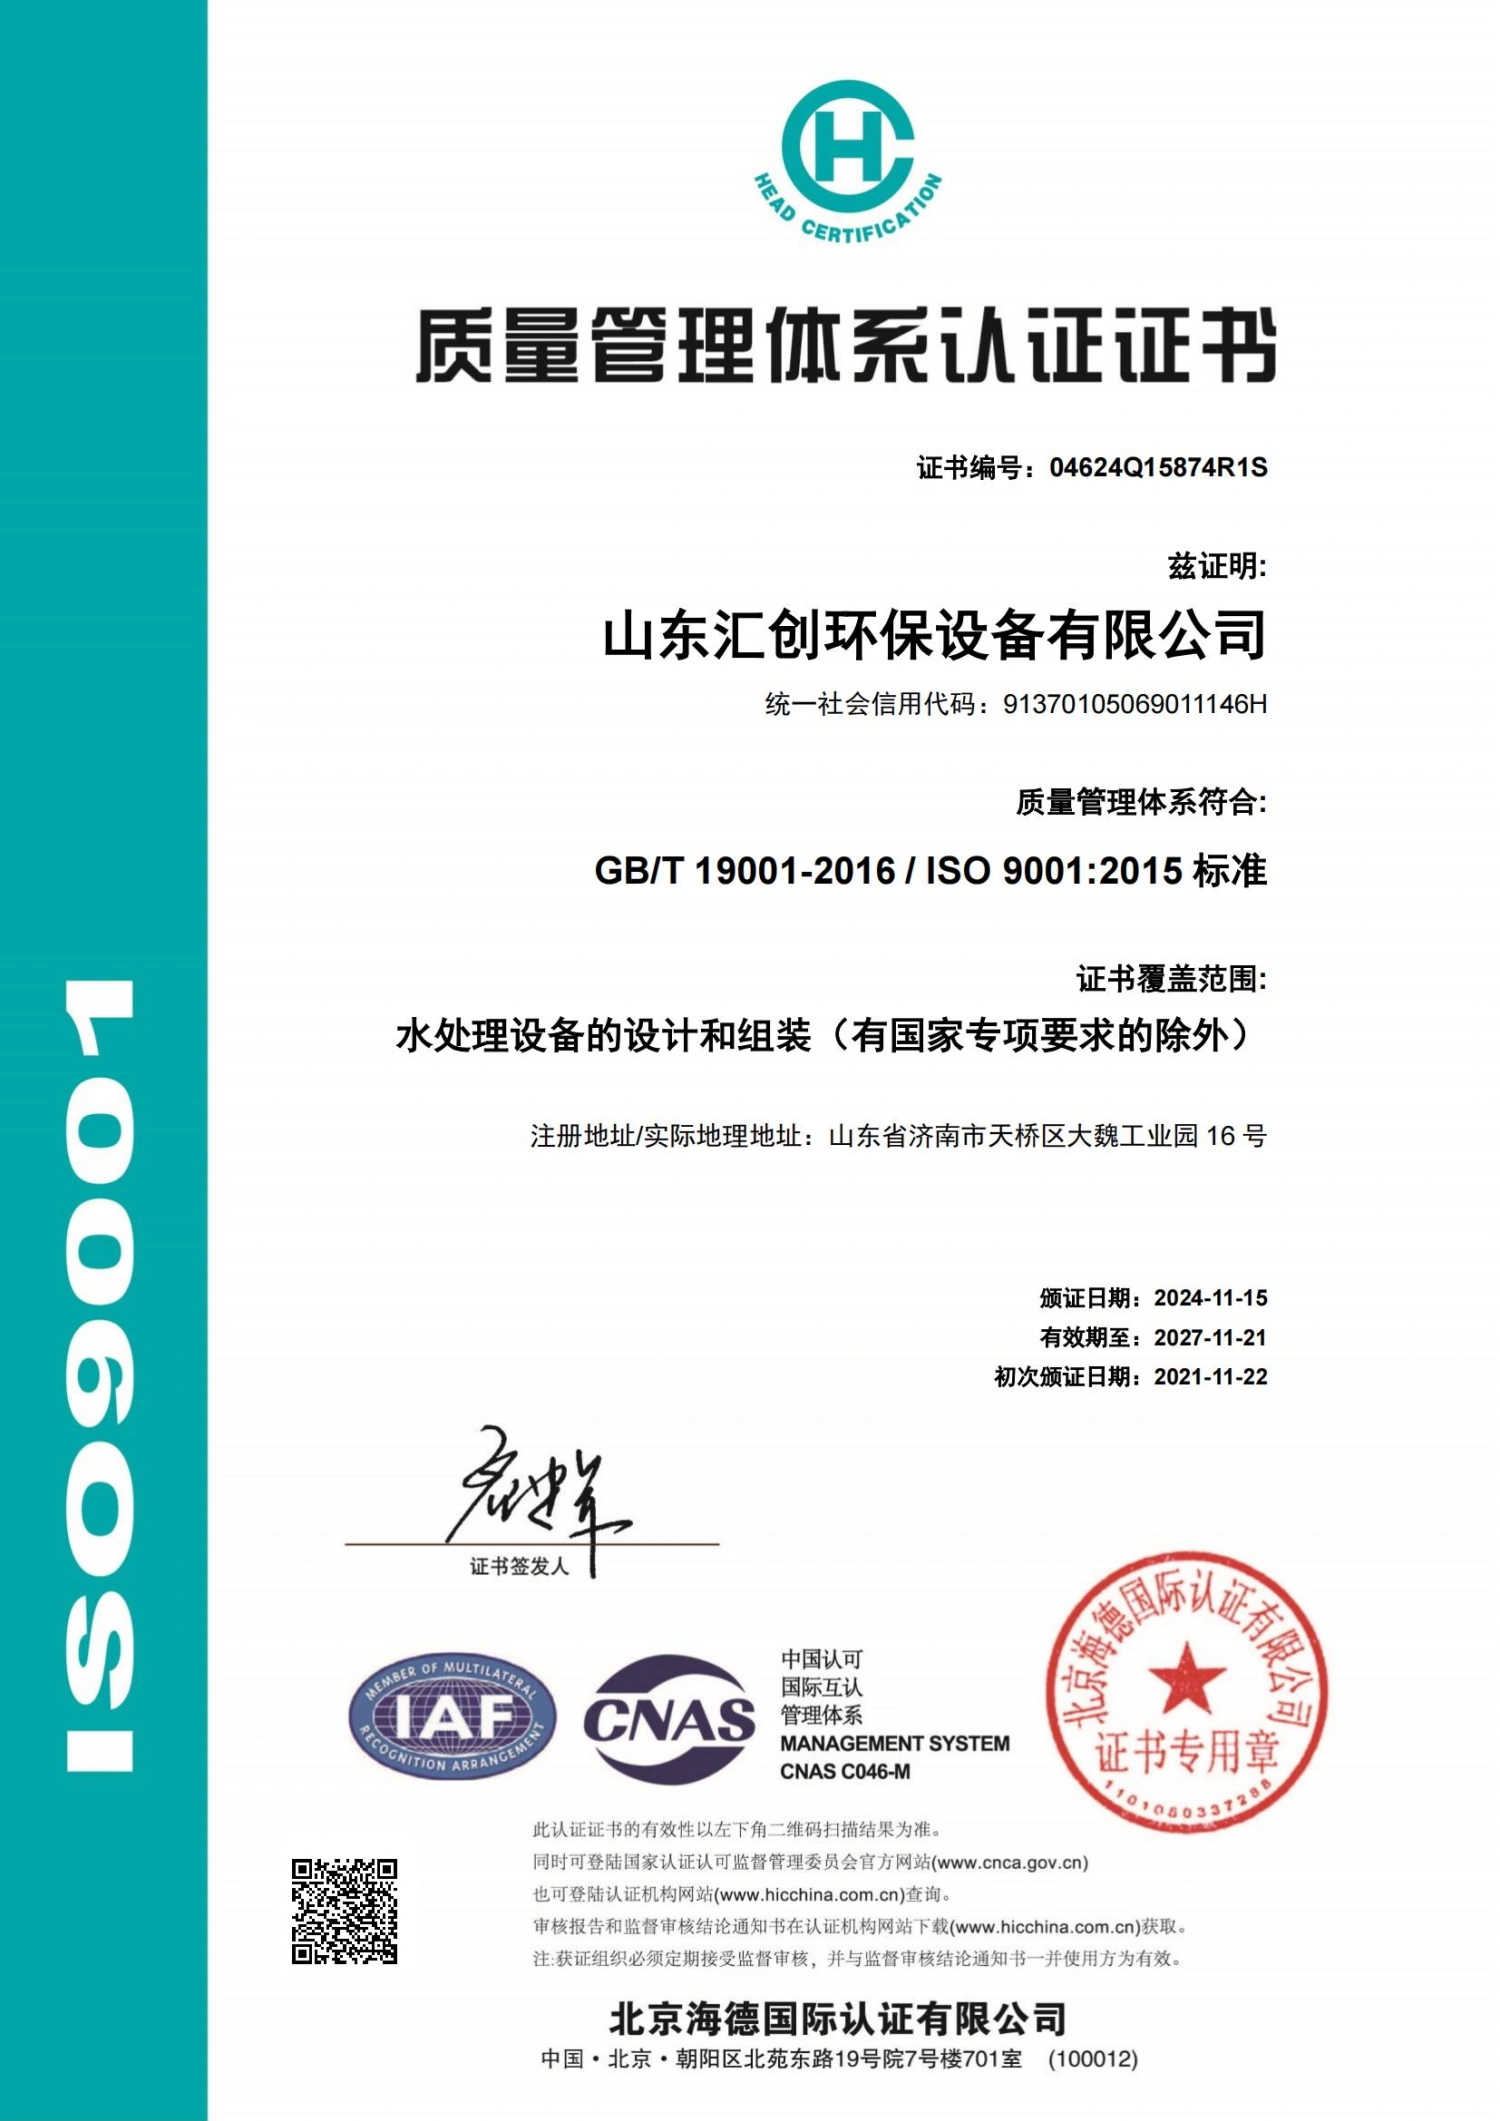
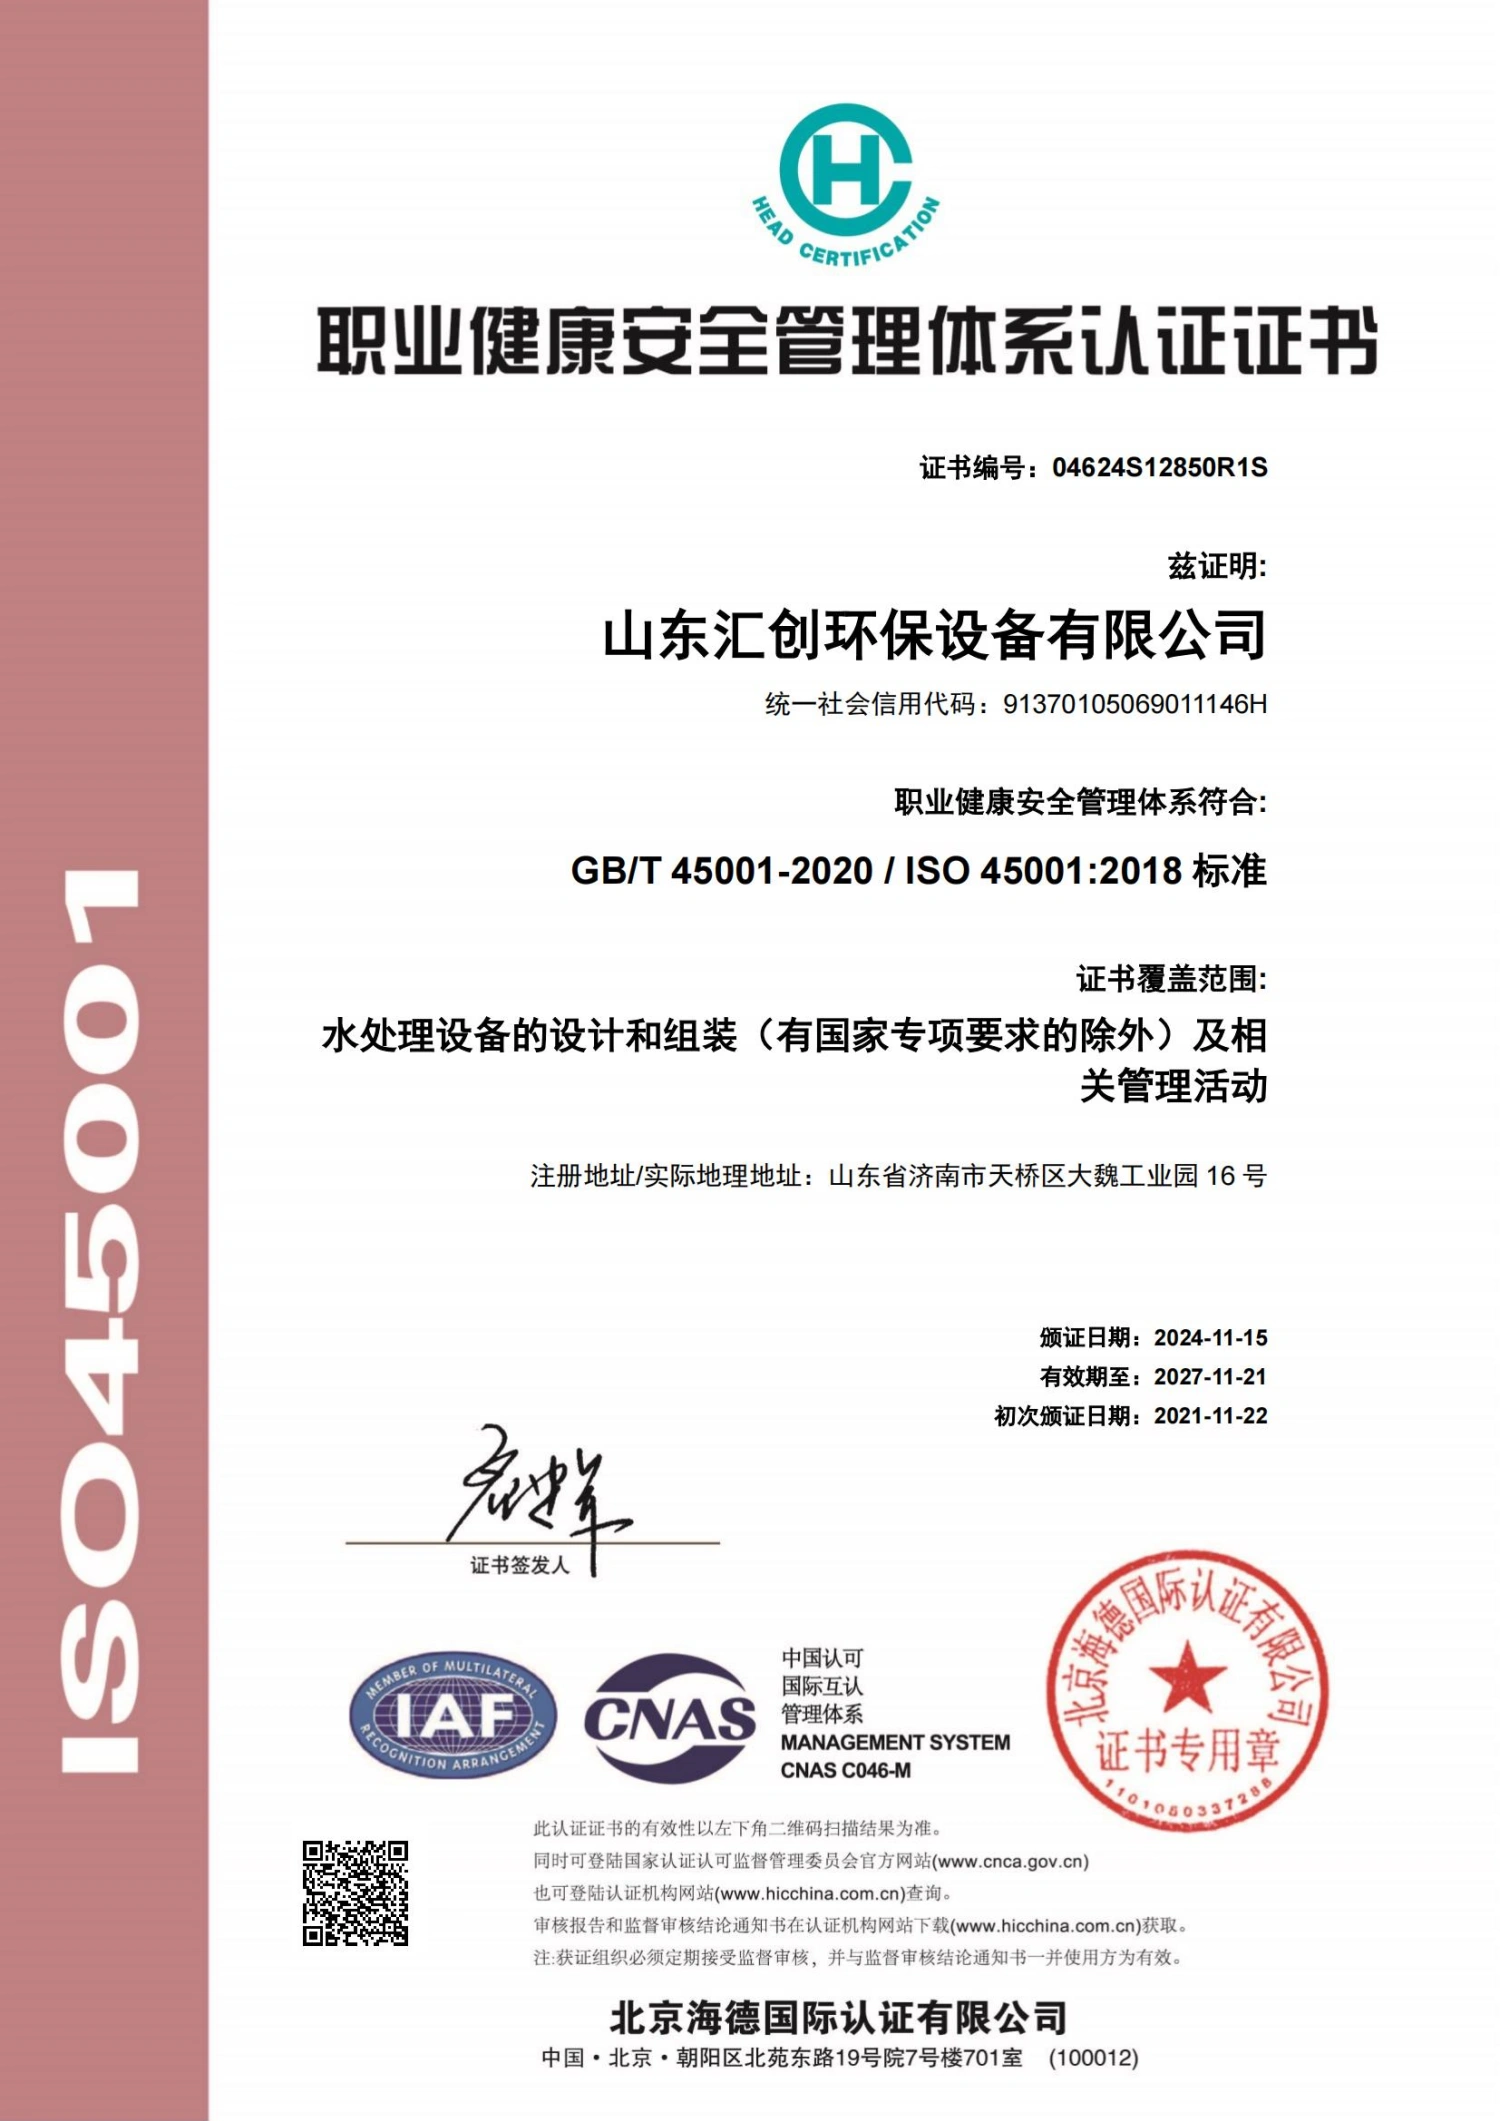
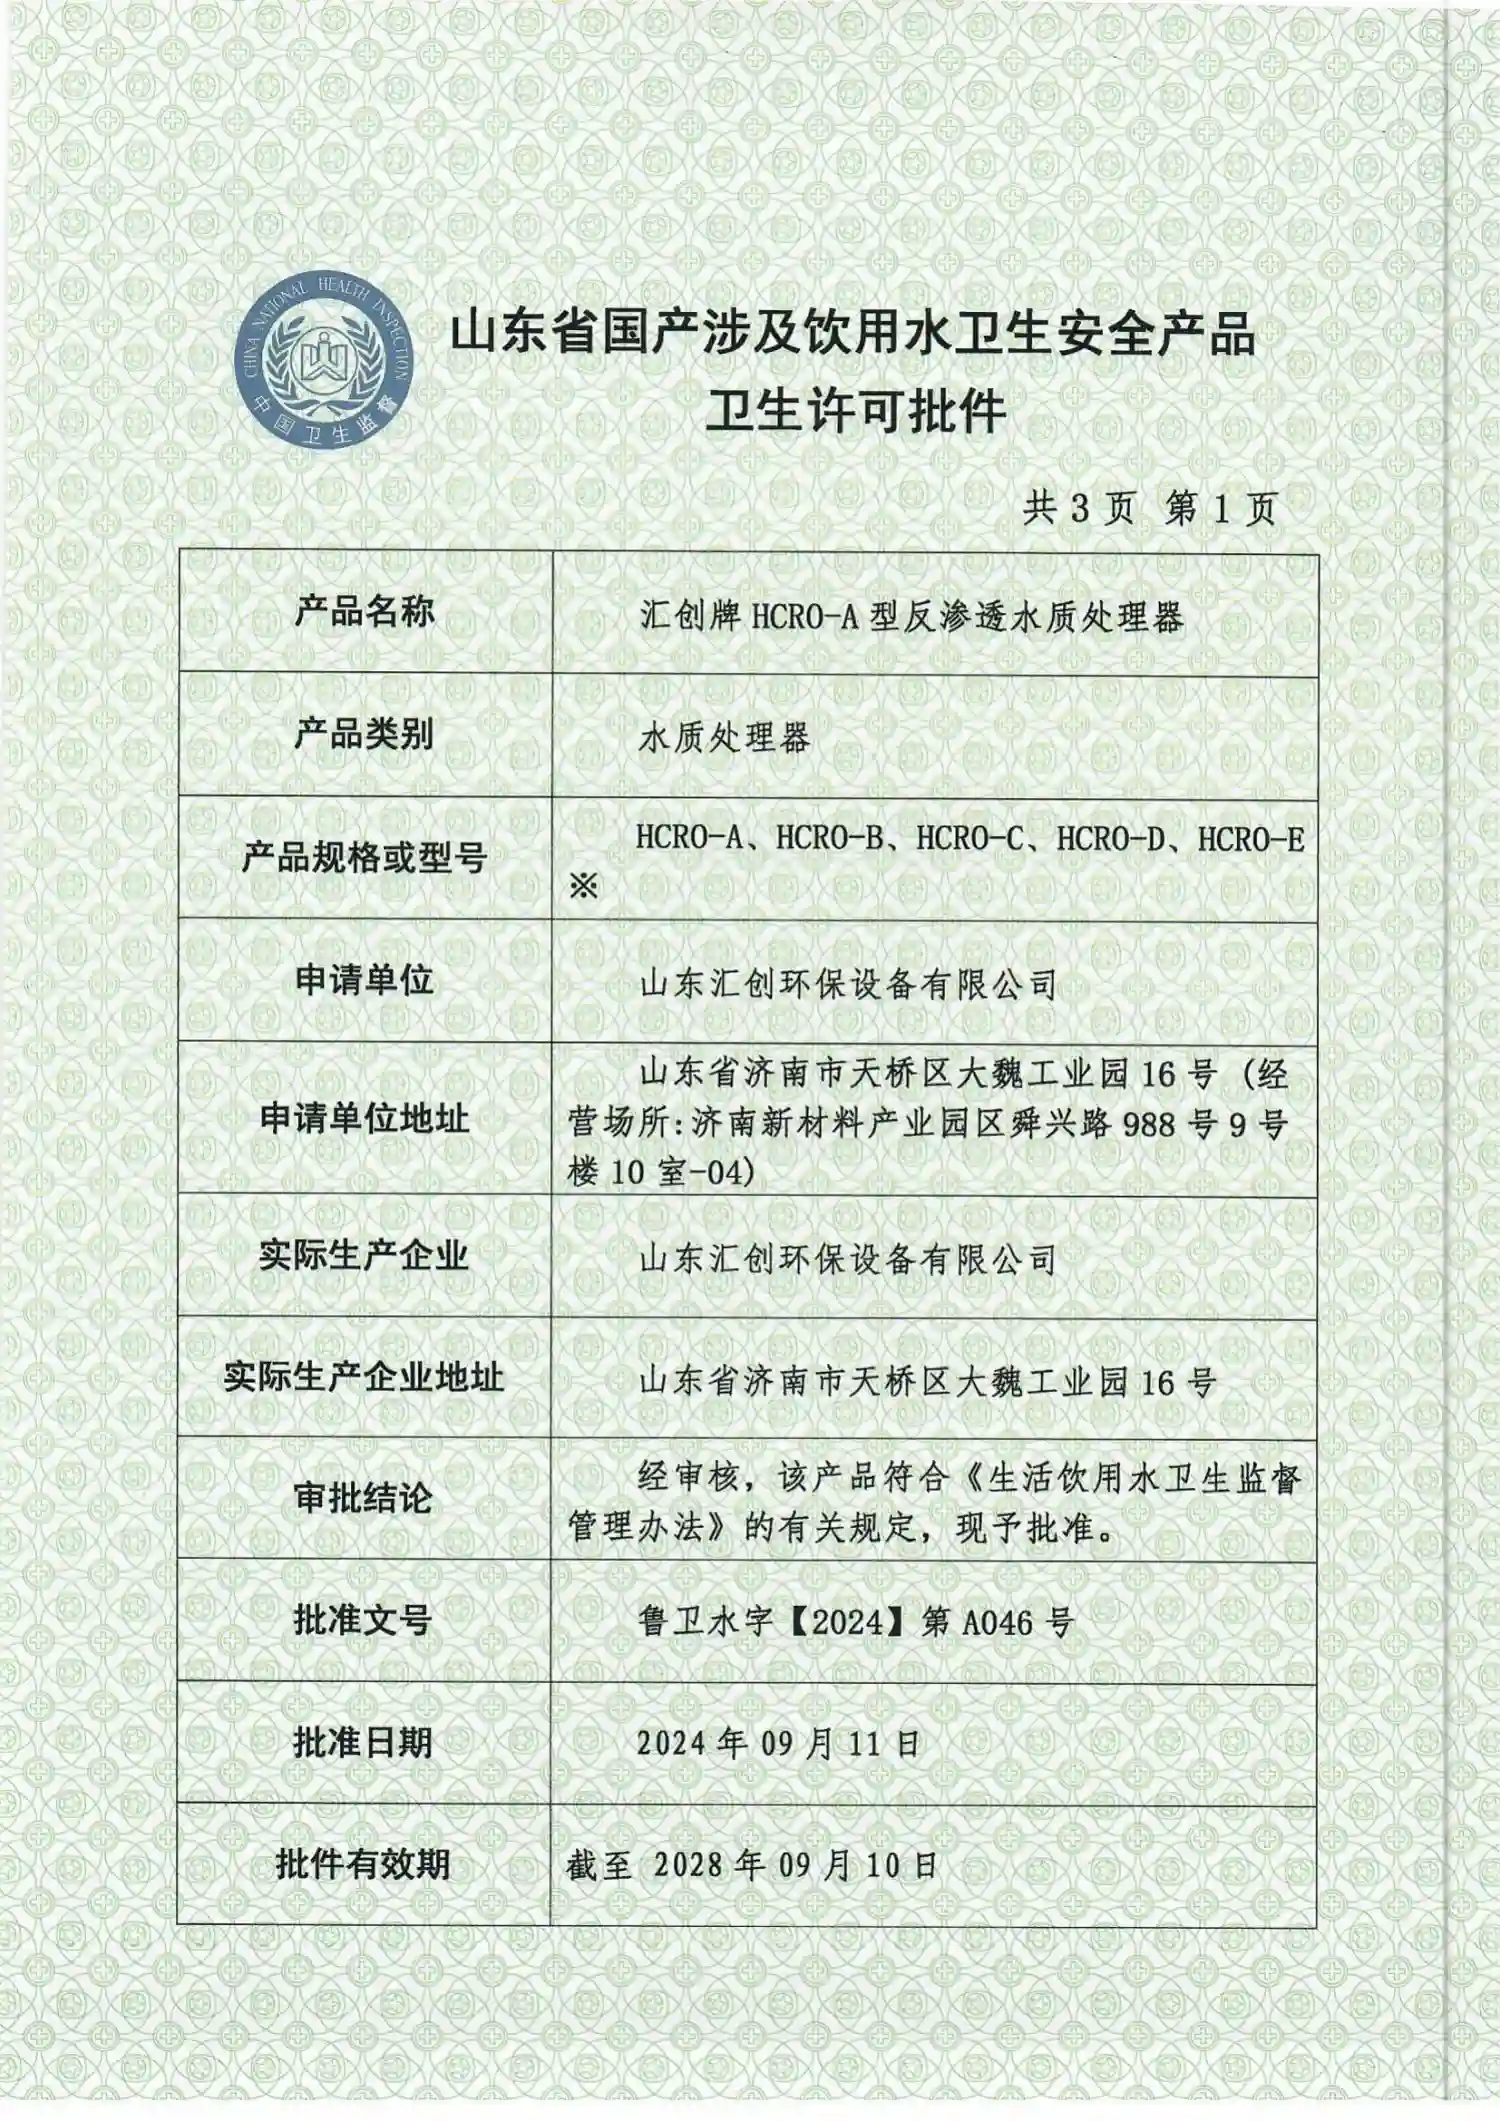
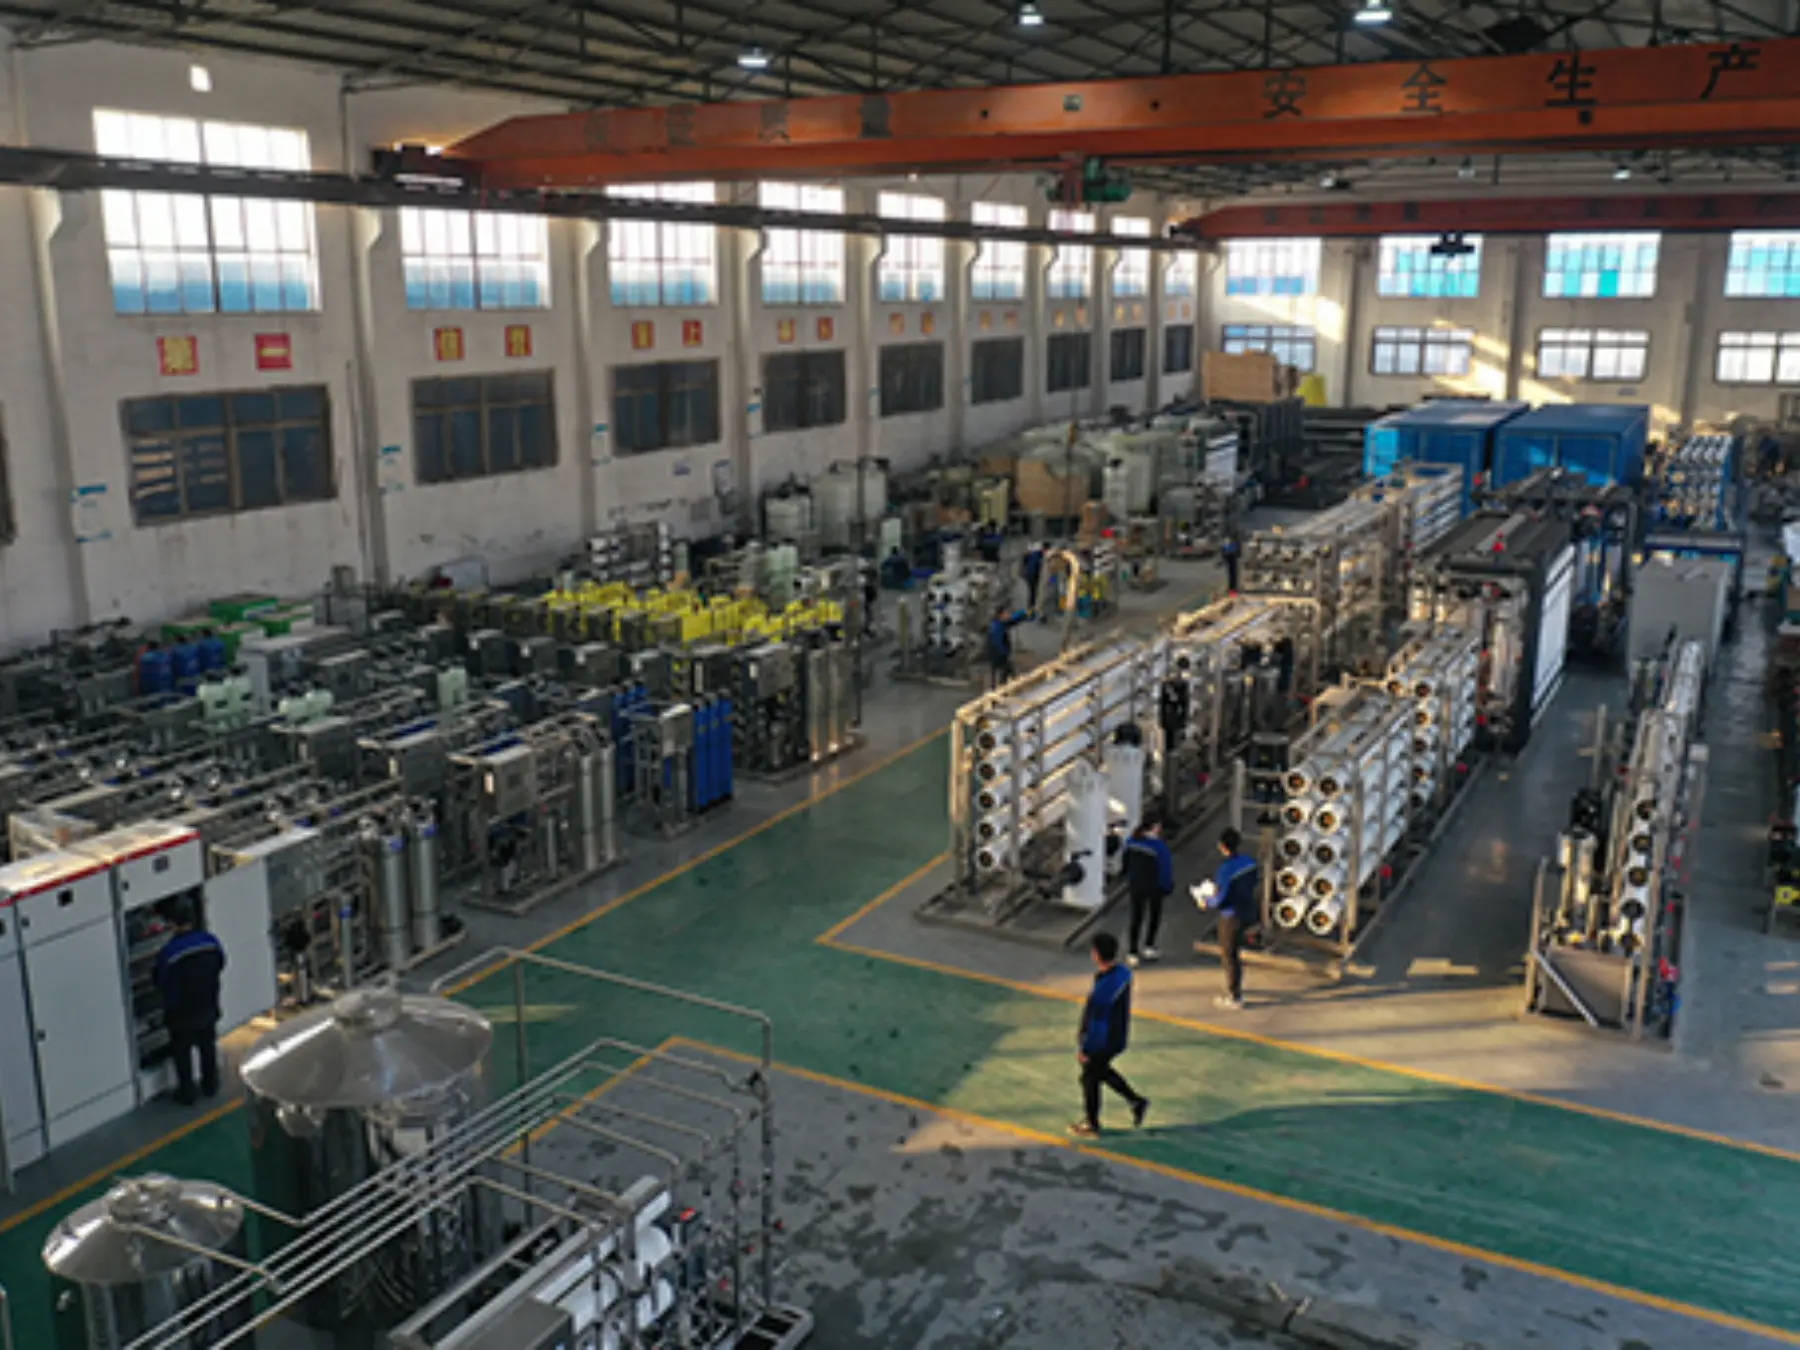
Partner with a Leading Chinese Environmental Manufacturer: Supported by a 15,000 sqm production workshop, 15 senior design engineers, and a global track record of serving over 30,000 clients, Shandong Huichuang provides direct wholesale B2B pricing, complete engineering blueprints, and lifetime technical support. Contact our engineering desk today for a free custom CAD layout diagram and a competitive proposal for your water recycling project!
Reviews
There are no reviews yet.